

 English
 русский
 عربى


Fang Xuelan — Customer After-Sales Supervisor
Home / Author / Fang Xuelan — Customer After-Sales Supervisor / DK-7735 High-Speed Wire EDM Machine: Large-Format Four-Axis Cutting for Precision Production
DK-7735 High-Speed Wire EDM Machine: Large-Format Four-Axis Cutting for Precision Production
2026-08-27
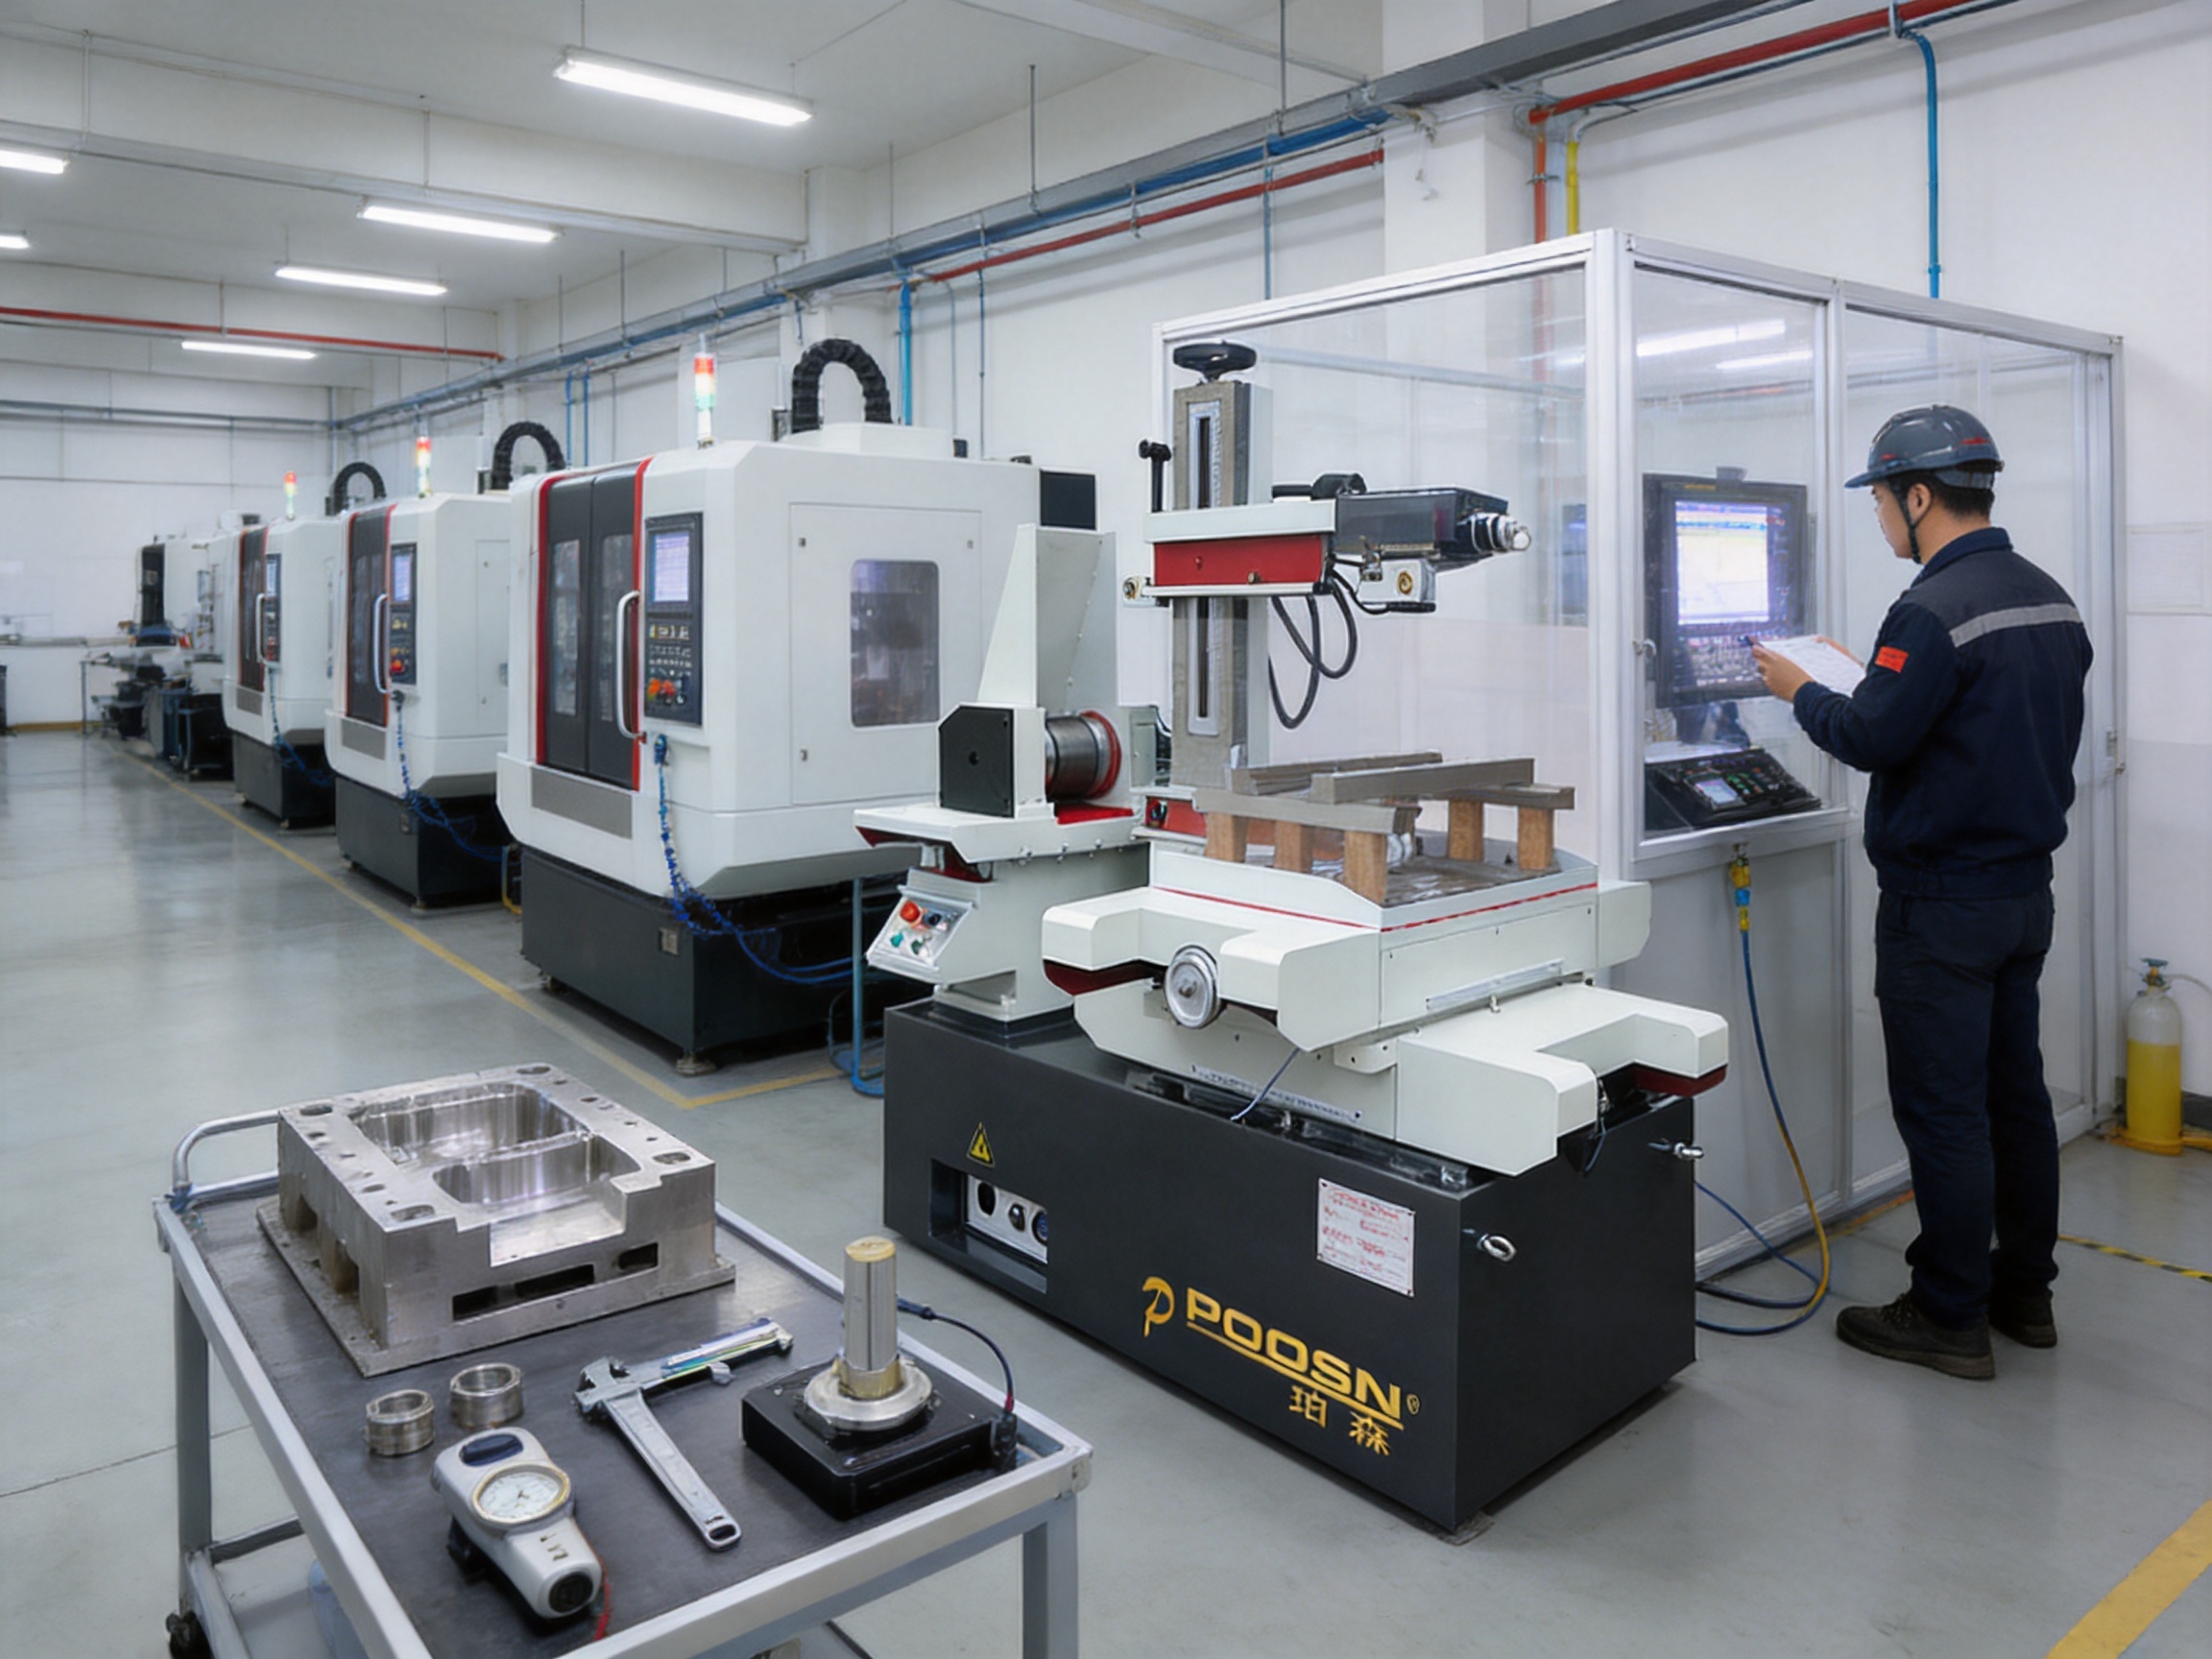
Modern manufacturers increasingly require machining equipment that can combine dimensional accuracy, high productivity, dependable operation, and flexibility across a wide range of workpiece sizes. These requirements are especially demanding in mold manufacturing, automotive components, aerospace structures, precision machinery, and other industries where complex profiles must be cut from difficult conductive materials. The DK-7735 CNC High-Speed Wire Electrical Discharge Machining Machine is designed to address these needs through a large working envelope, four-axis linkage, high cutting efficiency, strong load capacity, and a mechanical structure intended for continuous industrial use.
As a high-speed wire-cut EDM model in the DK-77 series, the DK-7735 is positioned between compact precision machines and larger heavy-duty platforms. It provides more X-axis and Y-axis travel than smaller models while maintaining a practical footprint for medium-sized production facilities. Its 350 mm X-axis travel, 450 mm Y-axis travel, 450 mm maximum cutting thickness, and 300 kg maximum worktable load enable manufacturers to process larger and heavier workpieces without immediately moving to a substantially larger machine.
The machine uses a four-axis control architecture based on X, Y, U, and V axes. This arrangement supports coordinated movement for straight cutting, taper cutting, upper and lower profile variation, and other complex trajectories. With cutting efficiency of up to 16,000 mm²/h, the DK-7735 is suitable not only for prototype work and precision mold production, but also for repetitive manufacturing where cycle time and cost per part are important considerations.
Its overall value is based on more than a single speed specification. The DK-7735 integrates a reinforced cast-iron structure, precision transmission components, digital pulse discharge control, wire-tension management, dielectric circulation and filtration, an operator-oriented control interface, and safety enclosure features. Together, these systems help create a stable machining environment in which accuracy, productivity, and operating reliability can be maintained over extended production periods.
Content
- 1 1. Product Positioning and Main Applications
- 2 2. Core Technical Specifications
- 3 3. Large Working Envelope and 300 kg Load Capacity
- 4 4. Four-Axis Linkage for Complex Contours
- 5 5. High-Speed Cutting and Production Efficiency
- 6 6. Discharge Control and Wire EDM Process Stability
- 7 7. Reinforced Machine Structure and Long-Term Accuracy
- 8 8. Precision Transmission and Positioning Components
- 9 9. Wire Transport, Tension, and Breakage Reduction
- 10 10. Filtration, Cooling, and Dielectric Management
- 11 11. Surface Quality and Precision Machining
- 12 12. Control Cabinet and Operator Experience
- 13 13. Safety and Workshop Cleanliness
- 14 14. Manufacturing Strengths and Quality Assurance
- 15 15. Advantages Over Conventional and Entry-Level Alternatives
- 16 16. Cost-Effectiveness in Batch Manufacturing
- 17 17. Installation and Commissioning Considerations
- 18 18. Maintenance and Service Support
- 19 19. Model Selection Within the DK-77 Series
- 20 20. Recommended Workflow for New Customers
- 21 21. Customization and OEM/ODM Capability
- 22 22. Quality Management and Corporate Experience
- 23 23. Environmental and Operational Responsibility
- 24 24. Practical Competitive Summary
- 25 25. Frequently Asked Questions
- 25.1 Q1: What is the worktable size of the DK-7735?
- 25.2 Q2: What is the maximum workpiece load?
- 25.3 Q3: What is the maximum cutting thickness?
- 25.4 Q4: Can the machine cut tapered profiles?
- 25.5 Q5: Is the DK-7735 suitable for mass production?
- 25.6 Q6: What materials can the DK-7735 process?
- 25.7 Q7: What surface finish can the machine achieve?
- 25.8 Q8: Which control cabinets are available?
- 25.9 Q9: Does the machine automatically adjust cutting parameters?
- 25.10 Q10: What installation conditions are recommended?
- 25.11 Q11: How can wire breakage be reduced?
- 25.12 Q12: How does the machine support long-term operation?
- 26 26. Conclusion
- 27 References
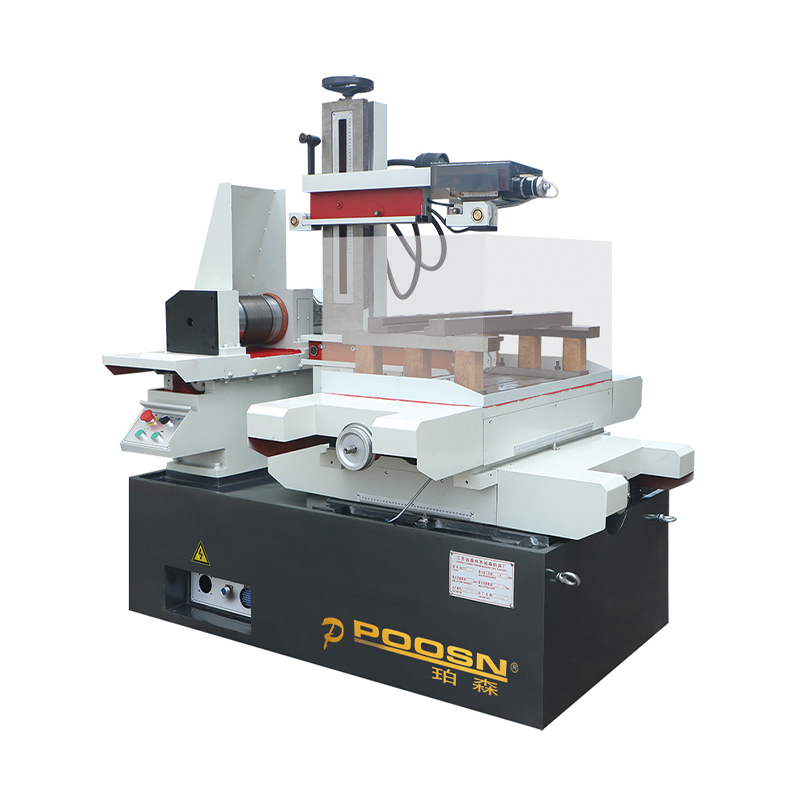
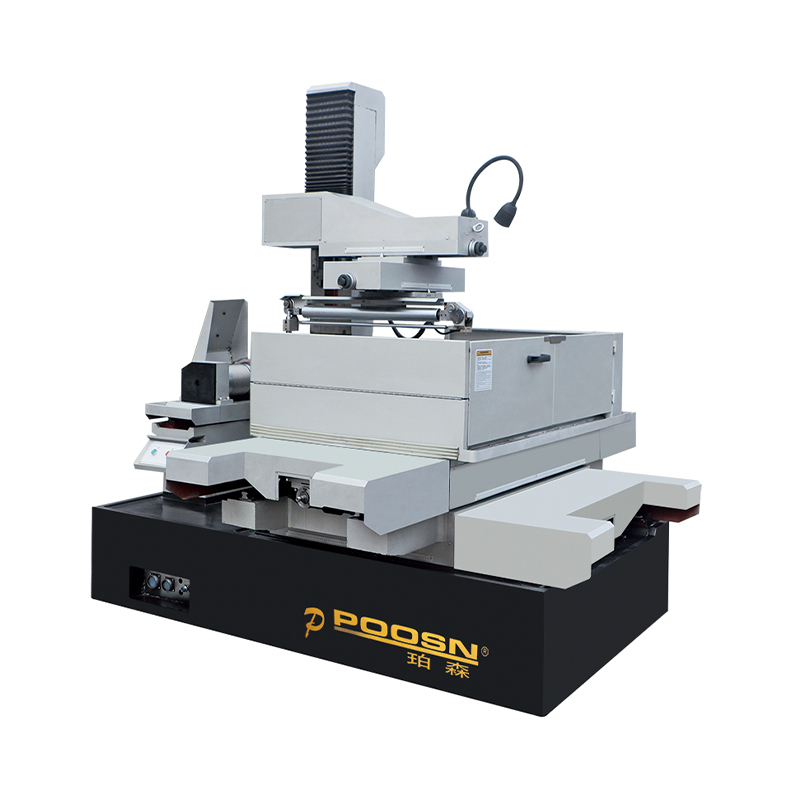
- 28 Product: DK-7735 CNC High-Speed Wire EDM Machine (4-Axis, 300kg Load)
1. Product Positioning and Main Applications
The DK-7735 is intended for manufacturers that need a larger working range than a small or entry-level wire EDM can provide. A compact machine may be adequate for small inserts, narrow components, and limited-size profiles, but its table dimensions, axis travel, and load rating can restrict production when the workpiece becomes wider, taller, or heavier. The DK-7735 addresses this limitation with a 500 × 750 mm worktable and 350 × 450 mm X/Y travel.
The machine is suitable for cutting steel, stainless steel, aluminum, copper, and other electrically conductive materials. Because wire EDM removes material through controlled electrical discharges rather than direct mechanical contact, it can produce intricate contours without applying conventional cutting forces to the workpiece. This makes it valuable for hardened materials, narrow slots, fine internal profiles, punches, dies, and components whose geometry would be difficult to obtain using milling, sawing, or conventional turning.
Typical applications include precision molds, stamping dies, cutting tools, automotive components, mechanical parts, aerospace components, and high-value replacement parts. The four-axis system also makes the DK-7735 appropriate for tapered profiles and parts requiring controlled variation between the upper and lower contour. In production environments, the machine can be used for both first-piece development and repeated batches, allowing a manufacturer to consolidate several machining requirements on one platform.
The DK-7735 is particularly useful where workpiece size and productivity must be balanced. The DK-7725 is designed for smaller and medium-sized components, while the DK-7745 and larger models provide greater travel and load capability. The DK-7735 occupies a practical middle position: it offers a substantial cutting area and 300 kg load capacity without requiring the installation space, foundation preparation, or investment associated with the largest machines in the series.
2. Core Technical Specifications
The following specifications describe the DK-7735 configuration and provide a basis for evaluating its suitability for a particular manufacturing process. Actual cutting performance may depend on material, thickness, workpiece geometry, wire type, dielectric condition, control cabinet selection, flushing conditions, and the selected electrical parameters.
| Item | DK-7735 Specification |
| Machine type | CNC high-speed wire-cut EDM machine |
| Axis configuration | X, Y, U, and V axes with four-axis linkage |
| Worktable size | 500 × 750 mm |
| X-axis travel | 350 mm |
| Y-axis travel | 450 mm |
| Maximum cutting thickness | 450 mm |
| Maximum worktable load | 300 kg |
| Maximum cutting efficiency | Up to 16,000 mm²/h, depending on configuration |
| Optimal surface roughness | Ra ≤ 2.5 μm |
| Maximum cutting taper | ±6°/80 mm |
| Drive system | X, Y, U, and V stepper drive with four-axis linkage |
| Standard control cabinet | ZH-K68 desktop cabinet |
| Optional control cabinet | ZHZK-03 vertical cabinet |
| Power supply | 3N 380 V ±10% |
| Machine dimensions | Approximately 1,650 × 1,250 × 1,830 mm |
| Machine weight | Approximately 1,100 kg |
| Accuracy standard | GB/T 7926-2015 |
The maximum cutting efficiency of 16,000 mm²/h should be understood as a rated upper value rather than a guaranteed result for every workpiece. Cutting efficiency is affected by workpiece thickness, material conductivity, flushing, wire condition, electrical discharge settings, and surface-finish requirements. A rough cutting pass may achieve a higher material-removal rate, while finishing passes prioritize dimensional accuracy and surface quality.
The stated surface roughness of Ra ≤ 2.5 μm represents the optimal surface-finish capability under suitable machining conditions. When a component requires a finer finish, additional skim cuts and carefully controlled electrical parameters may be applied. This separation between rough cutting and finishing allows the manufacturer to select a process balance appropriate to the part’s function, appearance, and tolerance requirements.
3. Large Working Envelope and 300 kg Load Capacity
One of the most important advantages of the DK-7735 is its ability to accommodate larger workpieces than compact high-speed wire EDM machines. The 500 × 750 mm worktable and 350 × 450 mm X/Y travel provide room for medium-sized plates, dies, mold components, and complex mechanical parts. A larger working envelope can reduce the need to reposition a workpiece or divide a profile into multiple setups.
Reducing the number of setups has several benefits. It can shorten preparation time, reduce alignment operations, minimize accumulated positioning errors, and simplify the production route. When a part can be clamped and cut in one stable setup, the operator has better control over datum references and the relationship between multiple features. This is especially valuable for dies and molds in which several contours must maintain precise positional relationships.
The 300 kg worktable load rating further expands the machine’s practical application range. Heavy plates and mold components can be supported without exceeding the specified load capacity, provided that the load is distributed correctly and the workholding method is suitable. Strong load capability is also useful in production environments where workpieces are mounted with fixtures, support plates, or auxiliary clamping structures.
Compared with smaller machines, the DK-7735 therefore offers a more favorable balance between capacity and installation requirements. Compared with very large models, it can be easier to place in a medium-sized workshop and may require less capital investment, while still supporting a broad range of industrial parts. This balance is one of its most relevant competitive strengths for manufacturers whose workpieces are too large for compact equipment but do not justify an extra-large platform.
4. Four-Axis Linkage for Complex Contours
The DK-7735 uses coordinated X, Y, U, and V axis movement. The X and Y axes control the primary movement of the worktable or machining path, while the U and V axes control the relative position of the upper and lower wire guides. This arrangement permits the wire to incline in a controlled manner, allowing the machine to produce tapered surfaces and profiles in which the upper and lower contours are not identical.
Four-axis linkage is particularly valuable in mold and die production. A taper may be required to facilitate part release, compensate for a design feature, or create a specific functional surface. Without coordinated upper and lower guide movement, the machine would be limited to largely vertical cutting or would require additional operations. The DK-7735 can execute these geometries within the available taper and thickness range.
The system also supports complex, irregular trajectories. Internal openings, narrow slots, gear-like profiles, punches, dies, and precision mechanical contours can be programmed according to the part drawing. When the control system applies path compensation and optimized movement, it can help maintain cutting consistency around corners and intricate shapes.
Four-axis control also provides production flexibility. A manufacturer may use the same machine for conventional straight cutting one day and tapered or variable-profile cutting the next. This reduces the need for dedicated equipment for every geometry and allows job shops to accept a broader range of customer requirements. For manufacturers operating multiple product lines, this flexibility can improve machine utilization.
5. High-Speed Cutting and Production Efficiency
The DK-7735 is designed around the practical production advantages of high-speed wire EDM. A maximum cutting efficiency of up to 16,000 mm²/h can reduce the time required for rough cutting, especially when the workpiece contains large sections of material. Shorter cutting cycles can increase daily output and improve the economics of repeated jobs.
Production efficiency, however, involves more than the movement speed of the wire or the nominal discharge rate. Efficient machining also depends on stable wire transport, reliable dielectric circulation, appropriate flushing, effective parameter control, simple program preparation, and minimal downtime between parts. The DK-7735 addresses these factors as part of an integrated machine system.
For batch production, even a modest reduction in machining time per workpiece can generate substantial annual savings. If a manufacturer cuts dozens or hundreds of similar components, improved cycle time increases available capacity without requiring an immediate expansion of the machine fleet. The same efficiency can also reduce overtime, improve delivery performance, and lower the labor cost allocated to each component.
The machine’s productivity must be matched to the required surface quality. High-speed rough cutting can be followed by finishing cuts when the application requires tighter dimensional control or improved surface appearance. This process structure allows operators to use the available power efficiently while preserving the quality requirements of the final part.
Three control cabinet options are associated with the DK-77 high-speed WEDM configuration. The standard ZH-K68 desktop cabinet is intended for normal operation, while the ZHZK-03 vertical cabinet is available as an option. The control cabinet selection can influence the operating interface and specific process performance, so the appropriate configuration should be confirmed according to the intended work, automation requirements, and operator preferences.
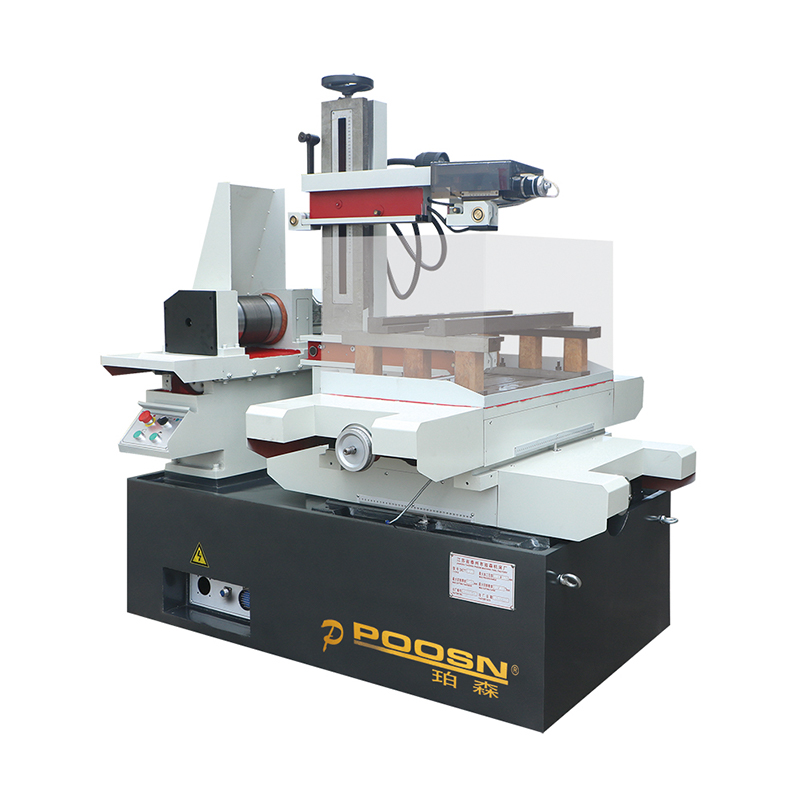
DK-7735 CNC High-Speed Wire EDM Machine (4-Axis, 300kg Load)
6. Discharge Control and Wire EDM Process Stability
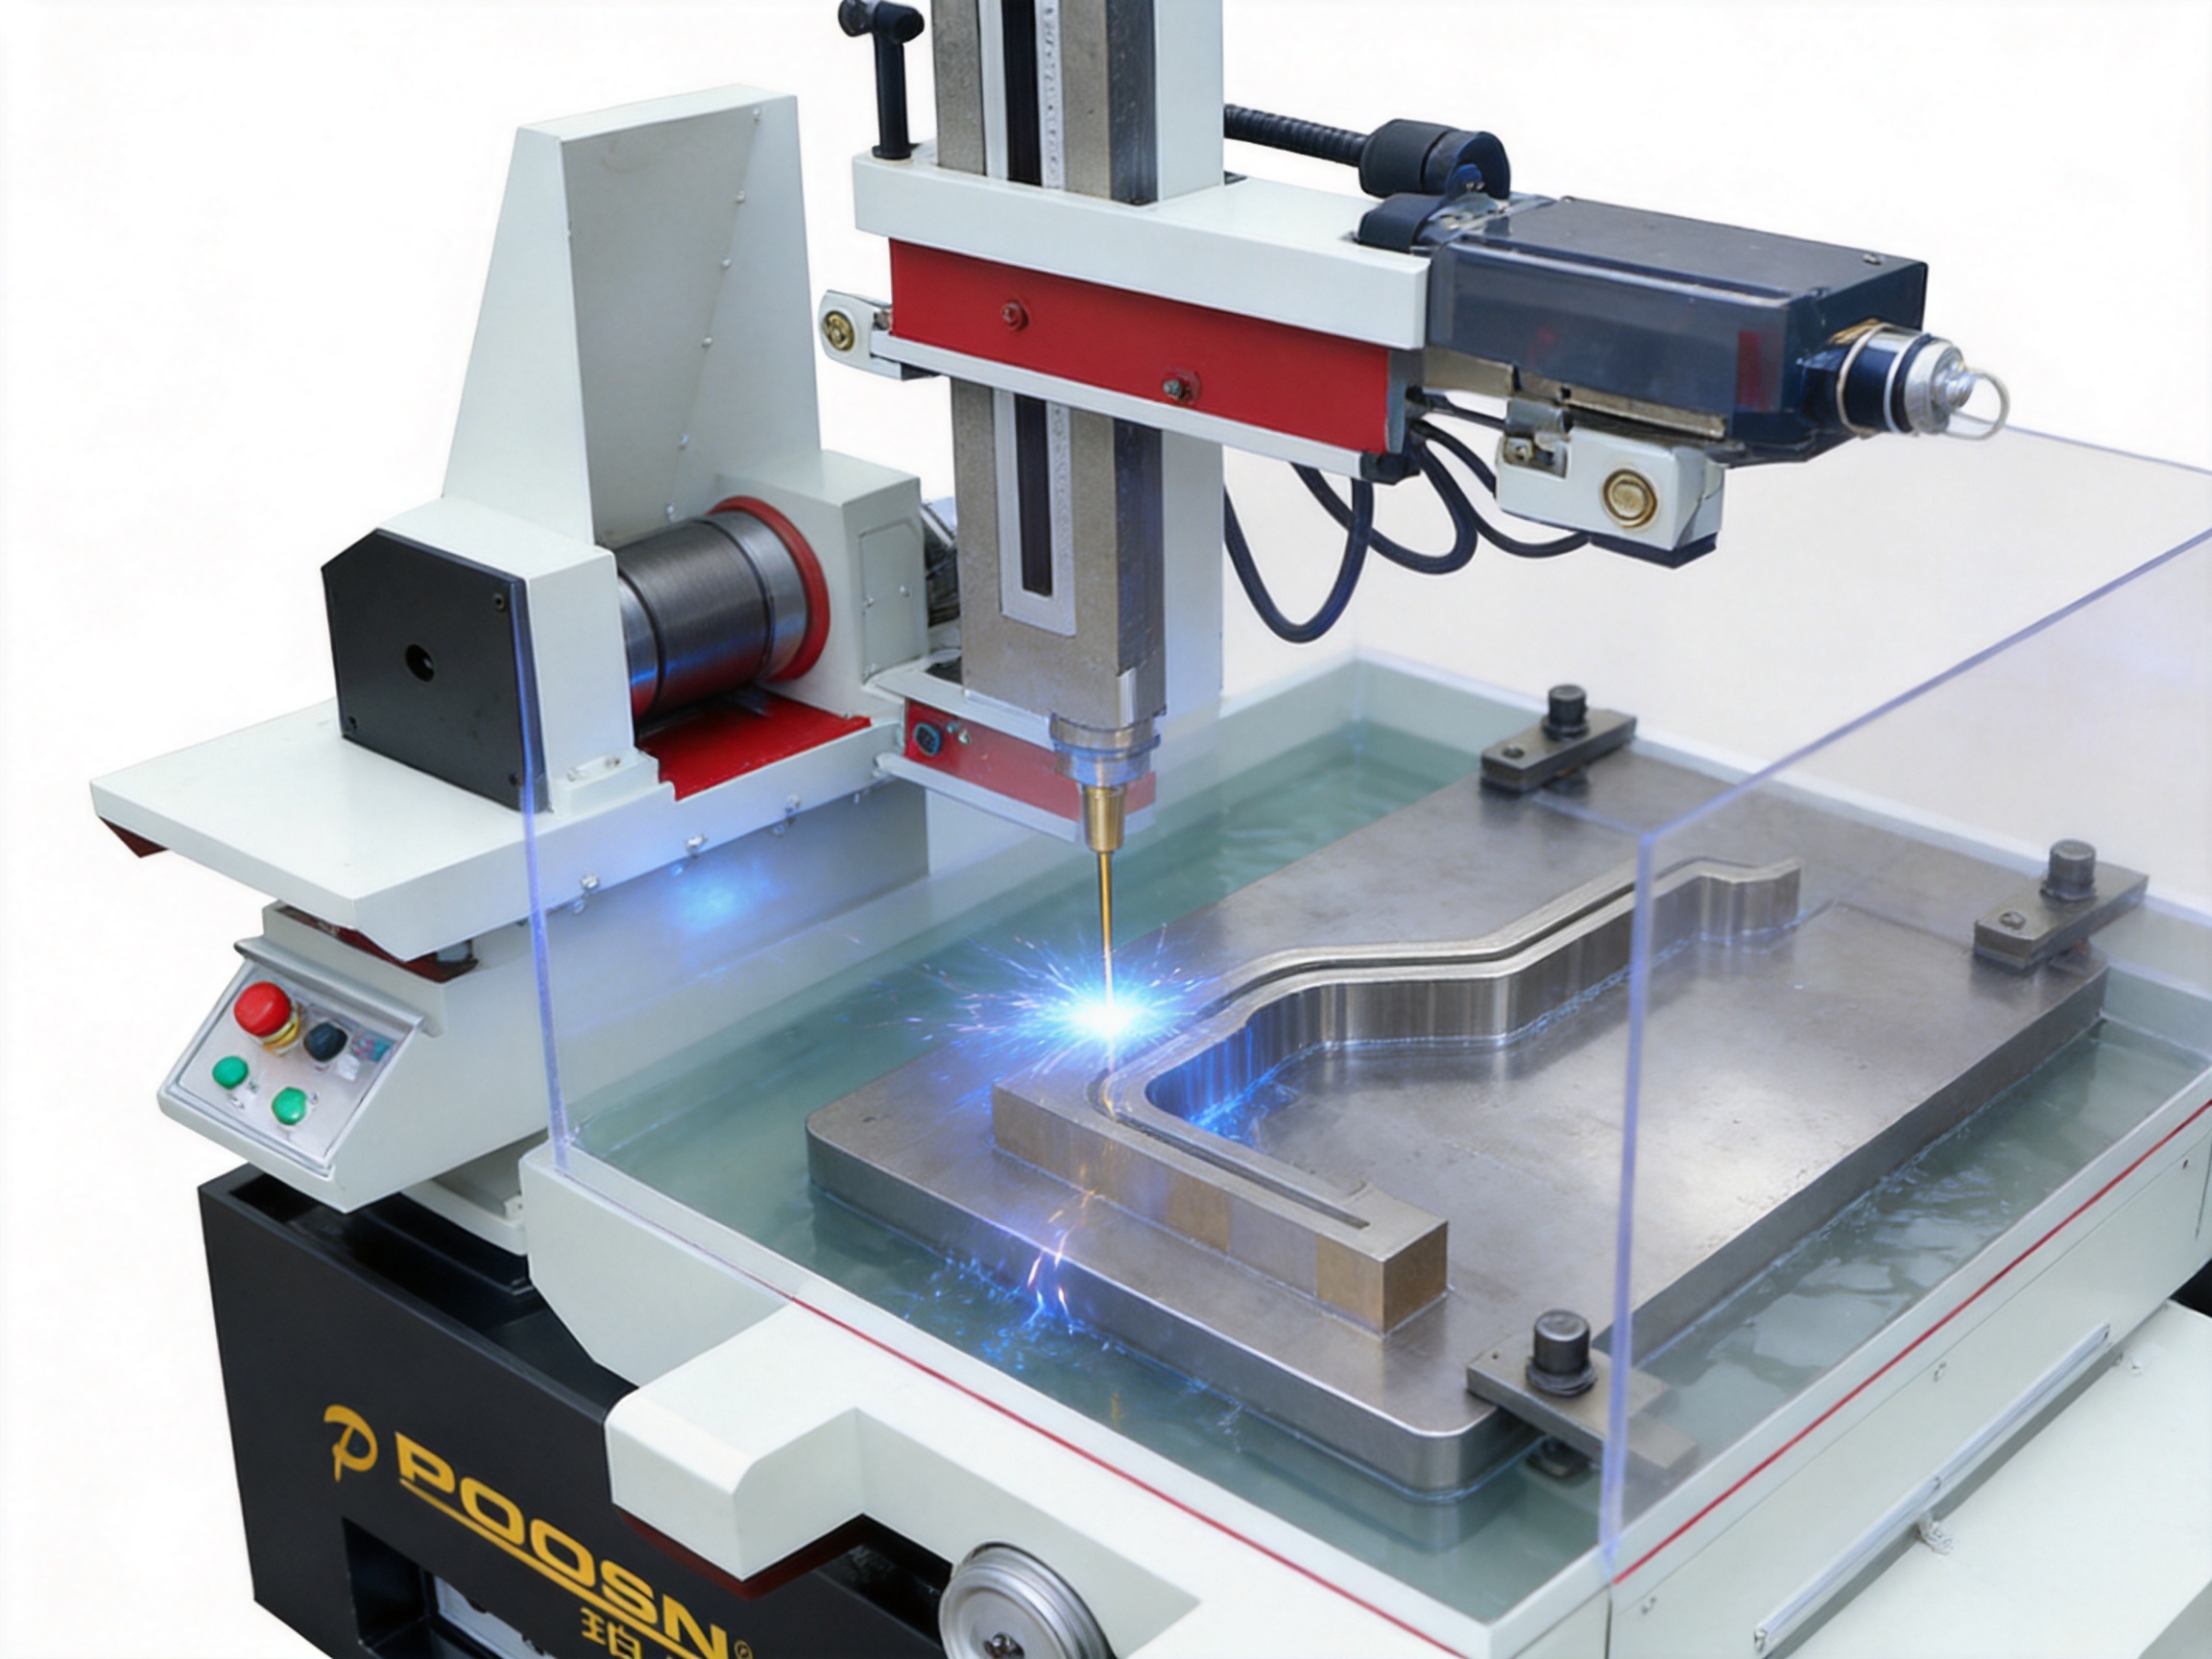
Wire EDM depends on a controlled series of electrical discharges between the moving wire electrode and the workpiece. The wire does not make continuous mechanical contact with the material. Instead, a carefully maintained gap is filled with dielectric fluid, and electrical pulses generate localized thermal energy that melts and removes small volumes of material. The stability of this discharge process has a direct influence on cutting speed, surface quality, wire consumption, dimensional accuracy, and the risk of wire breakage.
The DK-7735 incorporates a digital pulse power supply designed to adjust discharge parameters according to factors such as material type and thickness. Intelligent parameter adjustment can help maintain an appropriate energy level as the cutting conditions change. This is important because the electrical requirements for a thin stainless-steel component are different from those for a thick hardened-steel mold plate.
A stable pulse output helps prevent excessive discharge energy, unstable arcs, and irregular material removal. It can also support more consistent machining along long contours. In practical production, stable discharge behavior reduces the likelihood that operators will need to stop the machine repeatedly to correct settings or respond to wire failures.
The system is also intended to balance cutting speed with wire consumption and surface finish. A process that removes material very quickly but consumes wire excessively or produces an unacceptable surface may not be economical. By optimizing the pulse conditions, the machine can help manufacturers achieve a more useful combination of speed, quality, and operating cost.
Parameter optimization remains a process responsibility. Operators should select settings based on workpiece material, thickness, programmed geometry, wire specification, required taper, flushing conditions, and the number of finishing passes. The DK-7735 provides a technical platform for this optimization, but correct setup and routine process control remain essential for the best results.
7. Reinforced Machine Structure and Long-Term Accuracy
Structural rigidity is fundamental to the performance of a wire EDM machine. Although the cutting process does not involve the same mechanical forces as milling or turning, the machine must still maintain accurate relationships between the wire guides, worktable, column, and workpiece. Thermal variation, vibration, repeated axis movement, and the weight of large workpieces can all influence machining results.
The DK-7735 uses a high-strength cast-iron machine base that undergoes aging treatment. Aging is intended to reduce internal casting stress and improve dimensional stability. A stable base helps the machine maintain its geometric relationships during extended operation and reduces the risk of gradual deformation caused by residual stress in the casting.
The reinforced structure is especially important when cutting thick or heavy workpieces. A machine that is technically capable of accepting a large load must also preserve guide alignment and wire position under that load. The DK-7735’s structural design, together with appropriate support and workholding, is intended to provide a stable foundation for medium-sized heavy components.
Long-term accuracy depends on the entire installation and maintenance system, not only on the casting. The machine should be placed on a suitable foundation, leveled correctly, protected from severe temperature fluctuation, and maintained according to the operating manual. Lubrication, dielectric cleanliness, guide condition, wire alignment, and periodic accuracy checks all contribute to sustained performance.
The machine accuracy specification references GB/T 7926-2015. This provides a recognized basis for evaluating the positioning and machining accuracy of wire-cut EDM equipment. Before production release, users should establish their own inspection procedure using qualified measuring instruments and representative workpieces, especially when the machine will be used for high-tolerance components.
8. Precision Transmission and Positioning Components
Accurate wire cutting requires precise and repeatable movement. The DK-7735 uses precision ball screws and high-rigidity linear guides in its transmission and positioning system. Ball screws convert motor rotation into controlled linear movement, while linear guides support smooth and stable axis travel.
These components help the machine execute programmed paths with fine feed control. Smooth movement is important when cutting small radii, narrow slots, sharp corners, and intricate curves. Irregular movement or backlash could lead to contour errors, visible marks, or inconsistent dimensions between repeated workpieces.
The drive system uses stepper drives for the X, Y, U, and V axes. The four-axis linkage arrangement coordinates these drives so that the wire follows the programmed trajectory. Properly tuned acceleration, deceleration, interpolation, and compensation functions can help prevent unnecessary vibration and maintain a consistent cutting path.
Positioning repeatability is particularly valuable in batch production. Once a workholding method and program have been validated, the operator can load successive workpieces using the same references. Consistent axis movement reduces variation from one part to the next and makes it easier to establish a predictable inspection routine.
Transmission components also influence maintenance requirements. Regular lubrication and protection from contamination are essential. Abrasive particles and dirty working fluid can accelerate wear on moving components. A disciplined maintenance schedule helps preserve the advantages of the precision transmission system throughout the machine’s service life.
9. Wire Transport, Tension, and Breakage Reduction
Wire transport is a critical subsystem in high-speed WEDM. The wire must travel continuously through the machining zone at a controlled speed and tension. If the tension is too low, the wire may deflect or vibrate, affecting straightness and dimensional accuracy. If the tension is too high or the discharge is unstable, the risk of wire breakage may increase.
The DK-7735 incorporates a high-sensitivity tension control design intended to maintain stable wire travel. Stable wire transport helps preserve the relationship between the programmed path and the actual cut. It is particularly important in thick workpieces, where flushing conditions and discharge behavior can create additional cutting challenges.
Reducing wire breakage can improve production efficiency in several ways. It reduces unplanned stoppages, minimizes operator intervention, avoids repeated threading operations, and helps prevent defects caused by interrupted cuts. In high-volume production, these small improvements can accumulate into meaningful gains in equipment utilization.
Wire management should be combined with proper selection of wire type, tension, speed, electrical parameters, and flushing conditions. The wire path, guides, contact components, and collection system should be inspected regularly. Consumable components must be replaced when wear or contamination begins to affect machining stability.
10. Filtration, Cooling, and Dielectric Management
Working fluid performs several functions during wire EDM. It supports the electrical discharge, removes eroded particles from the cutting gap, cools the machining zone, and helps maintain a stable process environment. If the fluid becomes contaminated or its temperature changes excessively, cutting efficiency and surface quality can decline.
The DK-7735 incorporates a multi-stage integrated circulation and cooling concept. Filtration helps remove suspended particles from the dielectric fluid, while circulation maintains a continuous flow through the machining area. Cooling helps control temperature variation and supports more stable cutting conditions during extended operation.
Maintaining dielectric cleanliness is especially important when cutting thick materials or complex contours. Poor flushing can allow debris to remain in the gap, increasing the risk of unstable discharges, short circuits, slow cutting, and wire breakage. Effective filtration supports more consistent machining and may extend the service life of internal fluid-handling components.
Operators should monitor fluid condition, filtration performance, pump operation, and temperature. Filters should be cleaned or replaced according to actual operating conditions and the manufacturer’s maintenance recommendations. The use of suitable working fluid is also important for protecting the machine and achieving repeatable results.
Dielectric management is a practical area where user discipline directly affects performance. Even an advanced machine can lose efficiency if fluid maintenance is neglected. A routine inspection plan should include checking fluid clarity, flow, pressure, temperature, filter loading, and signs of contamination.
11. Surface Quality and Precision Machining
The DK-7735 is designed to support precision machining with an optimal surface roughness of Ra ≤ 2.5 μm under appropriate conditions. Surface quality is influenced by pulse energy, wire speed, workpiece material, thickness, flushing, cutting speed, and the number of finishing passes.
For a typical production process, the first cut removes the majority of the material efficiently. Subsequent skim cuts refine the contour and reduce the effects of the roughing operation. The control system’s path optimization and automatic gap compensation functions can help improve the consistency of these passes, particularly around corners and detailed profiles.
Sharp corners require careful control because the wire and discharge gap must respond to changes in direction. Excessive energy or poorly controlled motion can produce corner overcut, while insufficient energy may reduce efficiency. The DK-7735’s control algorithms are intended to optimize the path and compensate for process conditions, helping operators achieve more consistent corner quality.
Dimensional accuracy also depends on correct wire alignment and machine setup. The upper and lower wire guides must be clean and correctly adjusted. The workpiece must be securely clamped, properly supported, and accurately referenced. Thermal conditions should be as stable as practical, particularly when cutting large parts or holding close tolerances.
The machine can therefore be used in applications where both productivity and finish quality are important. It is not limited to rough profile separation. With suitable process planning, it can produce finished contours for molds, punches, dies, and precision components while reducing the number of secondary operations.
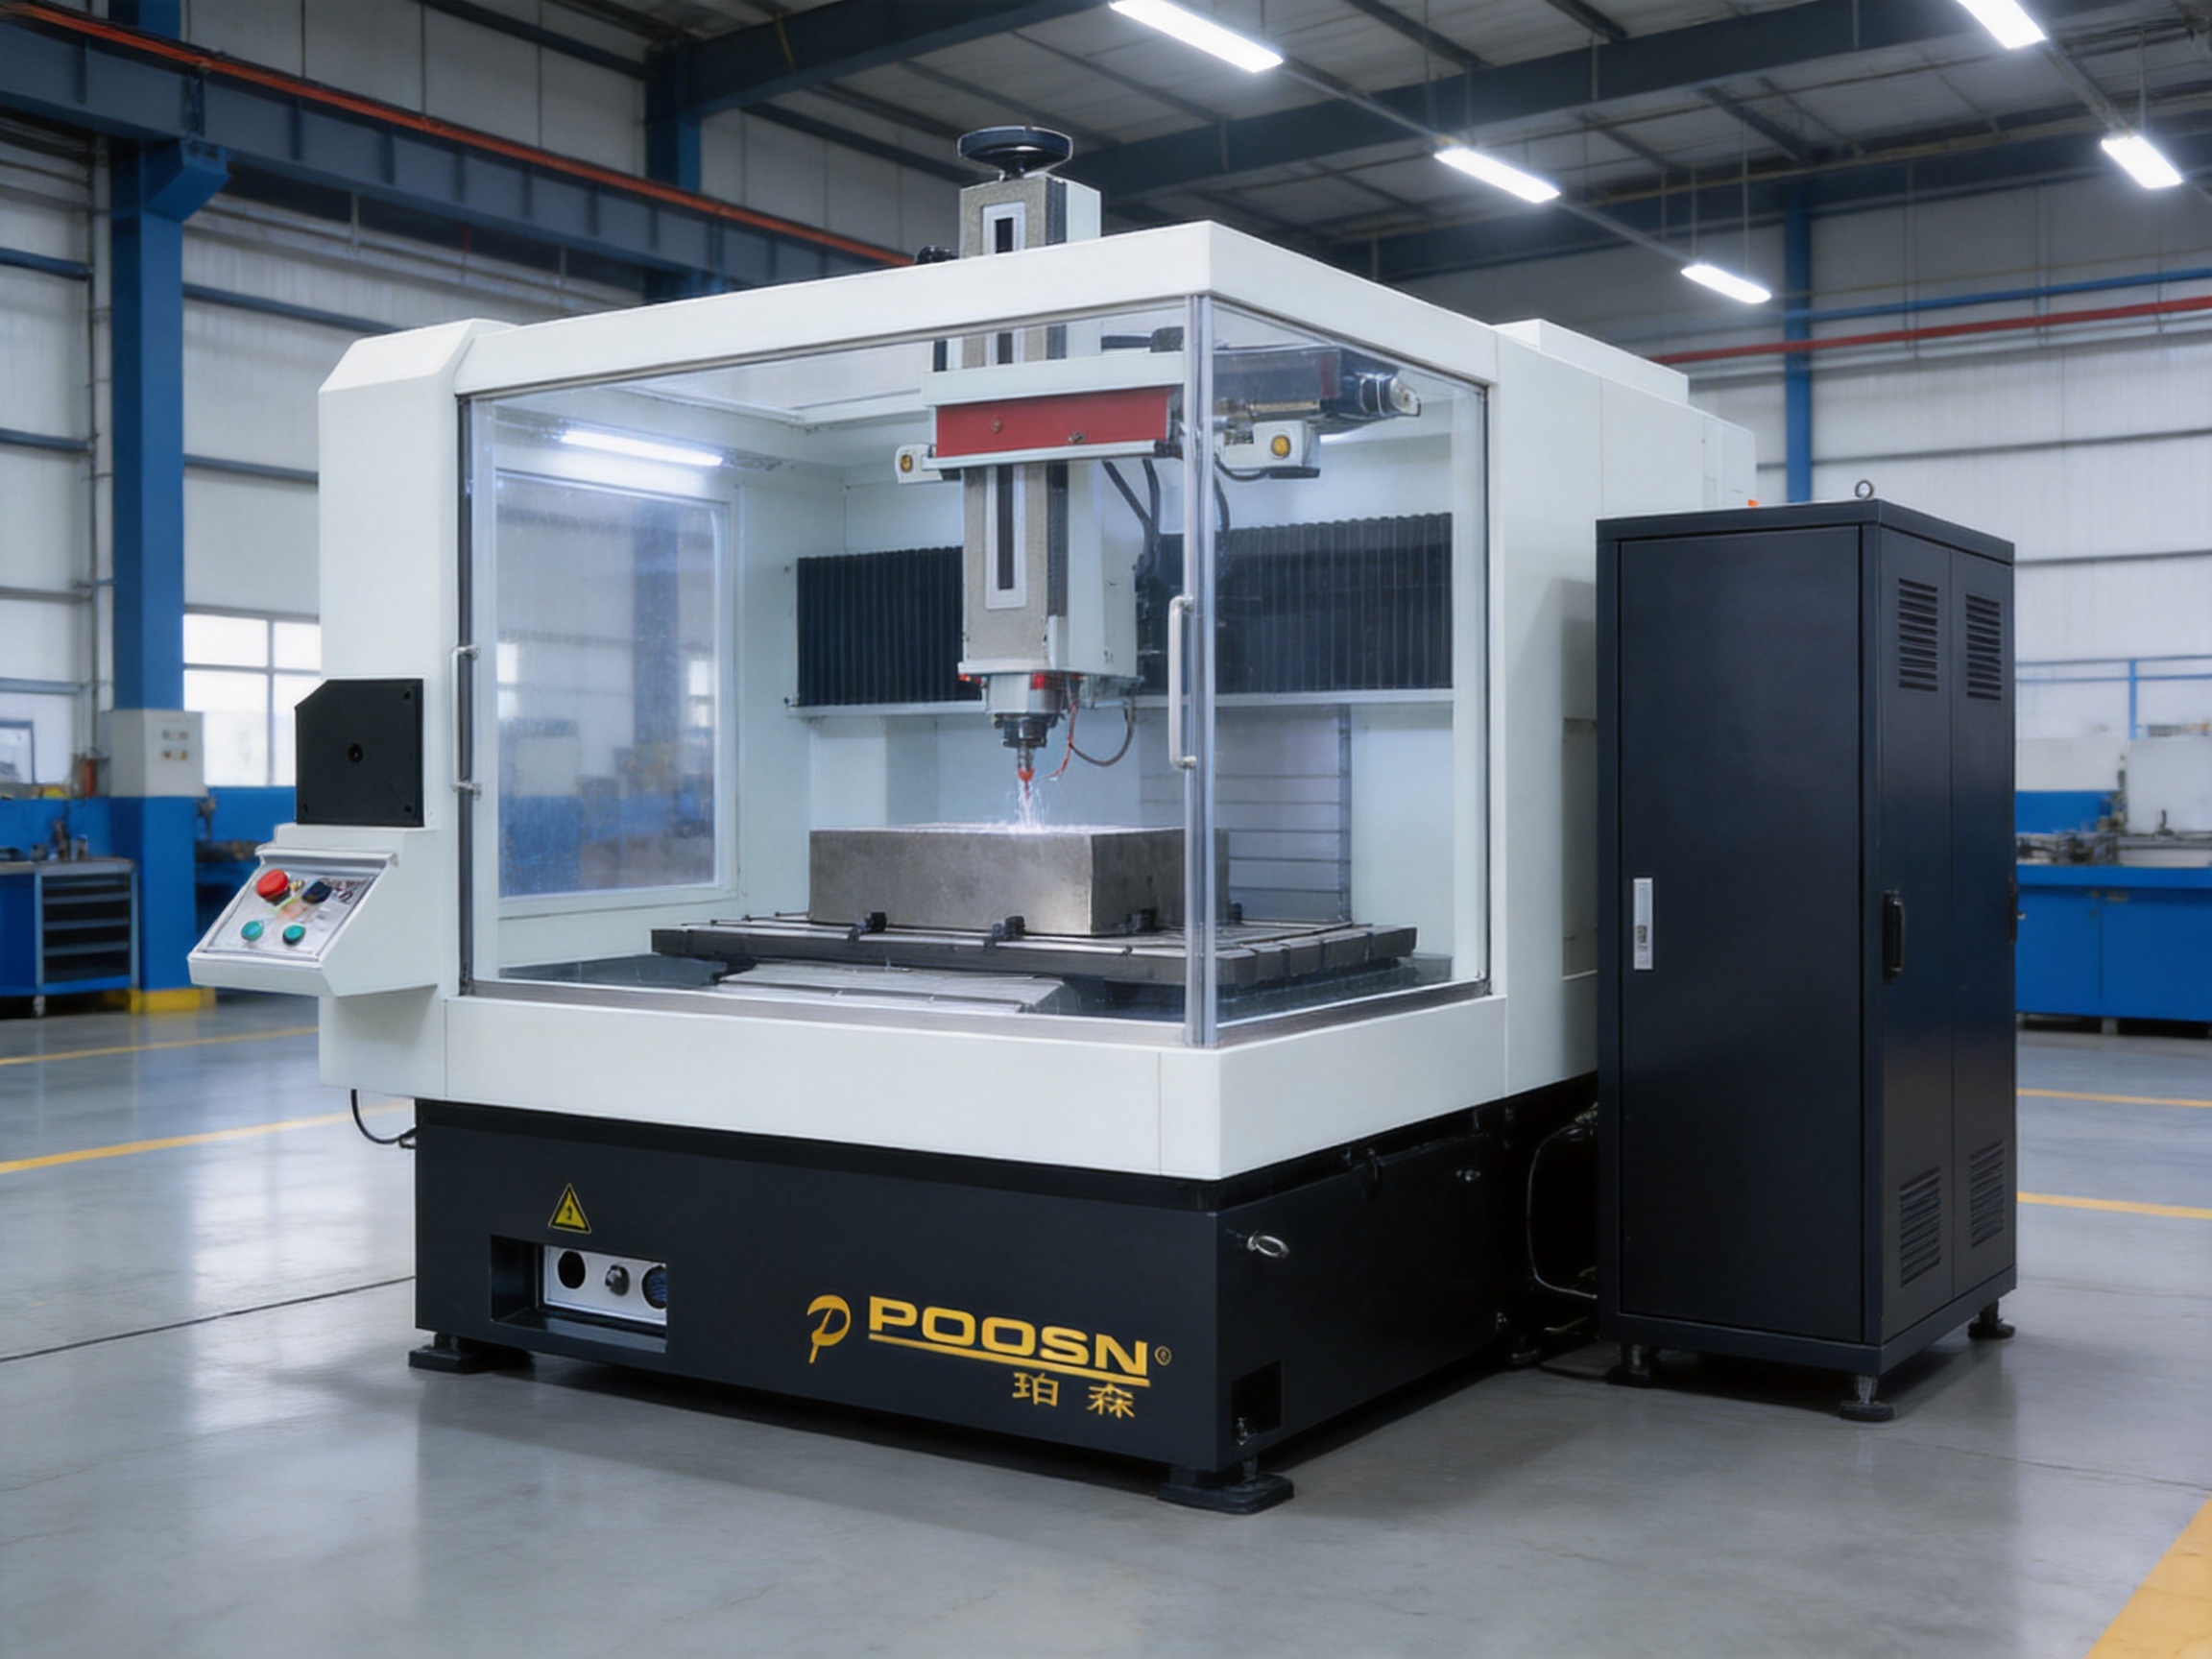
12. Control Cabinet and Operator Experience
A wire EDM machine’s value depends partly on how efficiently operators can convert drawings, programs, and process requirements into finished parts. The DK-7735 is equipped with a touchscreen-oriented control interface designed to simplify programming and machine operation. A clear interface can reduce the learning burden for new operators and help experienced technicians adjust parameters efficiently.
The control system supports four-axis simultaneous operation and provides access to functions required for profile cutting, taper cutting, compensation, parameter setting, and machine monitoring. The operator can configure the machining program according to the workpiece geometry and required process sequence.
An intuitive interface is particularly beneficial in job-shop environments, where operators may process different parts every day. Simple access to program management, coordinate setting, parameter selection, alarm information, and machine status can reduce setup time. It also helps standardize operating procedures between shifts.
The standard ZH-K68 desktop cabinet provides a conventional workstation arrangement. The optional ZHZK-03 vertical cabinet can be selected when a different layout or installation preference is required. The final cabinet choice should consider available floor space, operator position, visibility of the machining area, and the preferred production workflow.
Automatic parameter adjustment functions can support process stability by modifying cutting conditions according to workpiece requirements. Such features are useful for reducing manual trial and error, but operators should still verify the result through first-piece inspection. Automated adjustments work best when the machine is correctly maintained and the input conditions are accurately defined.
13. Safety and Workshop Cleanliness
The DK-7735 includes a safety enclosure designed to protect the operator and help contain working fluid during machining. Enclosure protection is important because the wire EDM process involves electrical energy, moving mechanisms, and circulating dielectric fluid. Keeping the machining area enclosed also contributes to a cleaner and more organized workshop.
Safety procedures should include correct grounding, appropriate electrical installation, controlled access to moving areas, and compliance with site-specific operating rules. Operators should not bypass protective devices or open access panels while the machine is operating. Emergency stop functions and alarm indications should be checked according to the maintenance schedule.
Working fluid management is another safety and housekeeping consideration. Leakage, splashing, and contaminated fluid can create slip hazards or damage surrounding equipment. The enclosure and circulation system help control these risks, but the workshop should still provide suitable drainage, spill response, ventilation, and cleaning procedures.
Training is essential. Operators should understand wire threading, workpiece clamping, program verification, fluid inspection, filter maintenance, alarm handling, and emergency procedures. A well-designed machine is most effective when supported by a disciplined operating culture.
14. Manufacturing Strengths and Quality Assurance
The manufacturer of the DK-7735, Taizhou Xinchengyang Machinery Manufacturing Co., Ltd., specializes in electrical discharge machining, wire-cutting technology, special processing equipment, and related machine tools. Its product development and manufacturing activities are supported by technical personnel, processing equipment, testing methods, and product design capabilities focused on industrial wire EDM applications.
Manufacturing quality begins with the stability of the machine structure. Castings must be processed and aged appropriately, mounting surfaces must be machined accurately, and guide and transmission components must be installed with attention to alignment. These steps form the foundation for the machine’s geometric accuracy and long-term operating behavior.
Assembly quality is equally important. The relationship between the wire guides, worktable, axis drives, electrical system, flushing system, and control cabinet must be verified during machine integration. Correct assembly reduces the possibility of alignment errors that could otherwise appear as dimensional variation, taper inconsistency, or unstable wire travel.
Testing and inspection provide the final verification before shipment. The company states that its machine tools undergo positioning accuracy testing and are manufactured according to applicable national standards. Such testing helps confirm that the machine meets the intended technical specifications and provides customers with a more reliable starting point for installation and process validation.
The company has been involved in wire-cutting EDM since 1999, introduced the POOSN brand in 2003, and established Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. in 2017 with its own factory and registered capital of 60 million yuan. Its development history also includes cooperation with CNC technology partners, recognition for quality and reputation, and high-tech enterprise recognition in Taizhou.
Experience accumulated over many years can support continuous improvement in mechanical design, electrical control, process parameters, component selection, and service procedures. For a customer purchasing production equipment, this background is relevant because machine performance depends not only on the model’s published specifications but also on the manufacturer’s ability to build, test, support, and improve the equipment.
15. Advantages Over Conventional and Entry-Level Alternatives
The DK-7735 offers several practical advantages compared with compact or basic wire-cut EDM machines. Its larger X/Y travel allows the machining of more substantial components. Its 300 kg load capacity supports heavier workpieces. Its four-axis linkage allows tapered and variable-profile cutting. Its high-speed configuration supports faster rough machining and improved production capacity.
Compared with conventional mechanical cutting for hardened materials, wire EDM can provide greater freedom for narrow slots, complex internal contours, and detailed profiles. Because the cutting wire does not exert a conventional tool force on the workpiece, the process can reduce problems associated with tool deflection and cutting-force distortion. This is particularly useful for delicate profiles and parts requiring high geometric accuracy.
Compared with a machine that provides only two-axis movement, the DK-7735 can produce more sophisticated geometry without requiring a separate taper-cutting operation. This can reduce handling, improve reference consistency, and expand the types of customer work that a production department can accept.
Compared with a very large wire EDM platform, the DK-7735 may offer lower installation and operating requirements while still handling medium-sized parts. Its machine dimensions of approximately 1,650 × 1,250 × 1,830 mm and weight of about 1,100 kg provide a practical solution for workshops that have limited space or need to control infrastructure costs.
Its competitive position is therefore based on balance rather than one isolated specification. The machine combines capacity, accuracy, speed, flexibility, and maintainability in a format suited to a broad segment of industrial users. These attributes can help manufacturers reduce outsourcing, shorten delivery times, and improve internal control over precision machining.
16. Cost-Effectiveness in Batch Manufacturing
When evaluating a wire EDM machine, purchase price is only one part of the total cost. Production managers should also consider machining time, labor involvement, wire consumption, filter usage, maintenance, energy, rework, scrap, and the cost of delayed delivery. The DK-7735 is designed to improve this broader cost equation through efficient cutting and stable operation.
High cutting efficiency can reduce the direct machining time assigned to each part. Four-axis capability can reduce additional setups or secondary taper operations. Strong load capacity can prevent the need to divide large workpieces into smaller sections. Stable wire transport and discharge control can reduce unplanned interruptions. Together, these improvements can contribute to lower cost per finished component.
The machine may also support better utilization of skilled personnel. An accessible control interface and automatic adjustment functions can simplify routine operation, allowing experienced technicians to focus on process development, inspection, and difficult jobs rather than repeated manual corrections.
For batch production, the benefits become more significant as the number of parts increases. A validated program can be reused, while fixture references and process parameters can be standardized. This supports consistent output and makes production planning easier. The machine’s suitability for mold components, automotive parts, precision machinery, and aerospace-related work also allows a manufacturer to serve multiple sectors with one equipment platform.
Cost-effectiveness still depends on correct process planning. The machine should be selected according to the expected part size, material, thickness, tolerance, surface-finish requirement, annual volume, and available operator skill. Customers should request application confirmation and configuration advice before purchase to ensure that the selected machine and control cabinet match the intended workload.
17. Installation and Commissioning Considerations
Proper installation is necessary to obtain the accuracy and stability expected from the DK-7735. The machine should be placed on a stable foundation capable of supporting its weight and the dynamic effects of operation. The installation area should provide adequate access for loading, maintenance, electrical connection, fluid servicing, and operator movement.
Temperature stability is recommended for precision machining. Large changes in ambient temperature can affect the machine structure, workpiece, wire, and dielectric fluid. A clean environment with limited vibration, adequate ventilation, and protection from strong magnetic interference can further support reliable operation.
The electrical supply should comply with the specified three-phase 380 V ±10% requirement and local safety regulations. Grounding, circuit protection, cable routing, and cabinet ventilation should be completed by qualified personnel. The control cabinet should be positioned so that the operator can observe the machine and access controls without obstruction.
Commissioning should include leveling, axis movement checks, wire threading, guide alignment, fluid circulation, filter inspection, electrical verification, and test cutting. A sample workpiece can be used to confirm dimensional accuracy, surface quality, taper performance, and cutting stability. Production should begin only after the machine passes the customer’s internal acceptance criteria.
18. Maintenance and Service Support
Regular maintenance protects the performance of the DK-7735 and helps extend the service life of its moving and electrical components. Daily tasks may include cleaning the work area, checking fluid level and condition, inspecting the wire path, confirming lubrication, and removing accumulated debris.
Periodic maintenance should include checking ball screws, linear guides, wire guides, electrical connections, pumps, filters, seals, tension mechanisms, and cooling components. The frequency of inspection should reflect operating hours, material type, cutting thickness, environmental conditions, and production intensity.
High-quality working fluid and correct lubrication are important. Contaminated fluid can affect discharge stability and accelerate wear in the circulation system. Insufficient or unsuitable lubrication can increase friction and reduce the accuracy of axis movement. Maintenance personnel should follow the machine manual and use compatible consumables.
Technical support is another important part of equipment ownership. The manufacturer provides rapid response and professional technical assistance intended to support operational stability. Support may include installation guidance, operator training, troubleshooting, process advice, spare-parts coordination, and maintenance recommendations.
A long-term service relationship can reduce downtime and help customers obtain greater value from the machine. When a production issue occurs, accurate information about the material, thickness, wire, parameters, fluid condition, alarm message, and cut result can help technical personnel identify the cause more quickly.
19. Model Selection Within the DK-77 Series
The DK-7735 is part of a broader family of high-speed wire EDM machines. Selecting the appropriate model requires a comparison of table size, axis travel, maximum cutting thickness, load capacity, machine footprint, and expected future requirements.
| Model | Worktable Size | X/Y Travel | Maximum Load | Recommended Positioning |
| DK-7725 | 410 × 600 mm | 250 × 320 mm | 250 kg | Small and medium parts, precision molds, and small-batch production |
| DK-7735 | 500 × 750 mm | 350 × 450 mm | 300 kg | Medium-sized components, larger molds, and flexible production |
| DK-7745 | 570 × 850 mm | 450 × 550 mm | 400 kg | Large parts, high-precision molds, and demanding industrial components |
| DK-7745F | 570 × 950 mm | 450 × 650 mm | 500 kg | Extra-large workpieces and heavy precision components |
The DK-7735 is appropriate when the DK-7725 does not provide enough working range or load capacity, but the capacity of the DK-7745 or larger models is not yet necessary. If a customer expects future growth in part size, it may be advisable to consider additional clearance and load requirements rather than selecting a machine based only on current orders.
For very large workpieces, the series includes models such as the DK-7755F, DK-7763F, DK-7780F, and DK-77100F. These machines provide progressively larger worktables, greater travel, and load capacities ranging from 600 kg to 1,200 kg. Customizable options are available for DK-77100 and above machines, subject to technical confirmation.
20. Recommended Workflow for New Customers
A successful DK-7735 project should begin with a technical review. Customers should provide representative drawings, material information, thickness, tolerance requirements, desired surface finish, taper requirements, production volume, and available workshop conditions. This information allows the machine configuration and process expectations to be evaluated realistically.
The next step is configuration selection. Customers should confirm the preferred control cabinet, electrical requirements, wire and dielectric arrangements, workholding method, and any special customization needs. If a part includes unusual geometry or particularly demanding tolerances, sample cutting or technical consultation may be appropriate before finalizing the order.
After installation, operators should receive training covering safety, programming, workpiece setup, wire threading, parameter selection, fluid management, alarm response, and preventive maintenance. A documented standard operating procedure can improve consistency between operators and shifts.
Production validation should use a first article or trial batch. The customer can inspect dimensions, taper, surface finish, repeatability, and cycle time against the agreed requirements. Once the process is approved, programs and setup records should be stored for future production.
21. Customization and OEM/ODM Capability
Different industries often require different machine configurations. Workpieces may have unusual dimensions, heavy fixtures, specialized cutting requirements, or specific control preferences. The manufacturer provides customization services intended to align machine performance with special customer requirements.
Customization may involve application-specific process advice, cabinet selection, layout preferences, workholding considerations, and other technical details subject to feasibility review. OEM and ODM cooperation can be useful for distributors, industrial equipment integrators, and companies developing a dedicated production solution.
A customized solution should begin with a clear specification. The customer and manufacturer should define working range, load, cutting thickness, taper, accuracy, surface finish, production volume, installation conditions, software requirements, and acceptance standards. Clear documentation helps prevent misunderstandings and ensures that the delivered machine matches the intended application.
The value of customization is greatest when it solves a real production problem. It should not add unnecessary complexity. A well-designed custom solution can improve workflow, reduce manual handling, support a particular product family, or make the equipment easier for operators to maintain.
22. Quality Management and Corporate Experience
The company’s development history reflects a long-term focus on wire-cut EDM technology. Since 1999, it has specialized in electrical discharge wire cutting. The POOSN brand was introduced in 2003, followed by cooperation with Bingfeng CNC in 2007 to expand market coverage. In 2009, the company was recognized as an Advanced Unit for Quality and Reputation.
Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. was established in 2017 and built its own factory. In 2018, the company obtained a patent related to a fully automatic CNC machine tool using plate-type winding and suction-type adhesive technology. In 2021, it was recognized as a High-Tech Enterprise in Taizhou.
This experience supports the company’s ability to manage product development, mechanical production, electrical integration, testing, and after-sales service. Its products are sold throughout China, with selected models exported to Southeast Asia, West Asia, Europe, and the Americas.
The company states that it follows a quality-first and customer-oriented approach. Its stated mission is to help customers improve competitiveness and optimize manufacturing processes through wire-cutting machines characterized by efficiency, precision, and stability. This philosophy is reflected in the DK-7735’s emphasis on practical production performance rather than only laboratory specifications.
23. Environmental and Operational Responsibility
Responsible machine operation includes managing energy, working fluid, filters, wire waste, and maintenance materials. A stable process can reduce scrap and rework, which lowers the material and energy consumed per acceptable part. Efficient cutting can also reduce the machine hours required for a given production target.
Working fluid should be handled according to local regulations and the supplier’s safety instructions. Used filters, contaminated fluid, and wire waste should be collected and disposed of through approved procedures. The machine area should remain clean to protect employees, equipment, and the surrounding environment.
Preventive maintenance also supports responsible production. Components that are correctly lubricated and kept clean can operate more efficiently and remain serviceable for longer. Avoiding premature component replacement reduces maintenance cost and material consumption.
24. Practical Competitive Summary
The DK-7735 competes effectively by combining capabilities that are often separated among different machine categories. It provides a larger work envelope than compact models, a higher load capacity than many basic platforms, four-axis taper capability, high-speed cutting, and a structure designed for extended industrial operation.
Its 350 × 450 mm X/Y travel allows medium-sized parts to be cut with fewer compromises. Its 300 kg load rating supports heavier mold and machinery components. Its 450 mm maximum cutting thickness provides flexibility for thick plates and substantial workpieces. Its maximum cutting efficiency of 16,000 mm²/h supports production-oriented machining.
The machine also offers process features that influence total performance: digital pulse control, precision ball screws, linear guides, wire-tension control, multi-stage filtration, cooling, path optimization, automatic gap compensation, and four-axis linkage. These features help address the practical causes of poor productivity, wire breakage, inconsistent finish, and dimensional variation.
For many manufacturers, the strongest advantage is the balance between capability and investment. The DK-7735 can serve a wide range of parts without the space and infrastructure demands of the largest WEDM machines. At the same time, it offers more capacity and flexibility than a small machine that may quickly become a bottleneck as product requirements expand.
25. Frequently Asked Questions
Q1: What is the worktable size of the DK-7735?
The DK-7735 has a worktable size of approximately 500 × 750 mm. Its X-axis travel is 350 mm and its Y-axis travel is 450 mm. These dimensions provide a larger operating range for medium-sized components and molds.
Q2: What is the maximum workpiece load?
The maximum worktable load is 300 kg. The workpiece should be distributed and supported correctly, and the complete load should include fixtures, support plates, and other items placed on the table.
Q3: What is the maximum cutting thickness?
The maximum cutting thickness listed for the DK-7735 is 450 mm. Actual results depend on the material, geometry, flushing, wire, electrical parameters, and required surface quality.
Q4: Can the machine cut tapered profiles?
Yes. The DK-7735 uses X, Y, U, and V axes with four-axis linkage. Its listed maximum cutting taper is ±6°/80 mm. The actual taper capability should be evaluated against the workpiece thickness and geometry.
Q5: Is the DK-7735 suitable for mass production?
Yes. Its high cutting efficiency, stable wire transport, automated parameter functions, and four-axis control make it suitable for batch and mass production. Process validation and correct maintenance are necessary to achieve consistent results.
Q6: What materials can the DK-7735 process?
The machine is suitable for electrically conductive materials such as steel, stainless steel, aluminum, and copper. Customers should confirm special alloys, unusual thicknesses, and demanding surface-finish requirements through a technical application review.
Q7: What surface finish can the machine achieve?
The optimal surface roughness is listed as Ra ≤ 2.5 μm under suitable cutting conditions. Finishing passes, stable dielectric circulation, correct wire alignment, and appropriate electrical parameters are important when a high-quality surface is required.
Q8: Which control cabinets are available?
The standard configuration uses the ZH-K68 desktop cabinet. The ZHZK-03 vertical cabinet is available as an optional configuration. The best choice depends on the workshop layout, operating preferences, and production requirements.
Q9: Does the machine automatically adjust cutting parameters?
The machine includes intelligent control functions that can automatically adjust cutting parameters according to workpiece requirements. Operators should still verify the process through test cutting and inspection, especially for new materials or demanding tolerances.
Q10: What installation conditions are recommended?
The machine should be installed on a stable, load-bearing foundation in a clean area with adequate ventilation and limited vibration. Stable temperature, proper grounding, suitable electrical power, and protection from strong magnetic interference are recommended for precision operation.
Q11: How can wire breakage be reduced?
Wire breakage can be reduced through correct tension, stable discharge parameters, clean guides, effective flushing, appropriate wire selection, and regular inspection of the wire transport system. Dielectric fluid condition is also important.
Q12: How does the machine support long-term operation?
The reinforced cast-iron structure, aging treatment, precision transmission components, cooling and filtration system, and maintenance access points support long-term operation. Regular cleaning, lubrication, fluid management, inspection, and timely replacement of consumables remain essential.
26. Conclusion
The DK-7735 CNC High-Speed Wire EDM Machine is a versatile production platform for manufacturers that need larger-format cutting, four-axis flexibility, and reliable precision. Its 350 mm X-axis travel, 450 mm Y-axis travel, 450 mm cutting thickness, 300 kg load capacity, and worktable size of 500 × 750 mm make it well suited to medium-sized molds, dies, mechanical components, automotive parts, aerospace-related workpieces, and batch production.
Its competitive value comes from the combination of large workpiece adaptability and efficient cutting. Digital discharge control, precision ball screws, high-rigidity linear guides, wire-tension management, integrated filtration and cooling, path optimization, and automatic gap compensation work together to support stable machining. Four-axis linkage further expands the machine’s usefulness by enabling taper cutting and complex upper/lower profile relationships.
The manufacturing capabilities and long experience of Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. add another important dimension. Through structural manufacturing, electrical integration, accuracy testing, customization, and technical support, the company provides more than a standalone machine. It provides an equipment solution intended to improve production capacity, reduce process cost, and maintain consistent machining quality.
For customers comparing high-speed wire EDM equipment, the DK-7735 should be evaluated according to the complete production requirement: workpiece dimensions, weight, material, thickness, geometry, tolerance, surface finish, annual volume, installation environment, and service expectations. When these factors align with its capabilities, the DK-7735 can serve as a dependable core machine for precision manufacturing and long-term industrial growth.
References
1. Taizhou Xinchengyang Machinery Manufacturing Co., Ltd., DK-77 High-Speed Wire EDM Product Technical Materials.
2. Taizhou Xinchengyang Machinery Manufacturing Co., Ltd., DK-7735 Product Specifications and Application Information.
3. GB/T 7926-2015, Accuracy Requirements and Inspection Principles for Wire-Cut Electrical Discharge Machining Tools.
4. International Electrotechnical Commission, Technical Principles of Electrical Discharge Machining and Dielectric Processing.
5. General technical literature on CNC wire electrical discharge machining, pulse power control, wire transport, dielectric filtration, and precision machine-tool maintenance.
Product: DK-7735 CNC High-Speed Wire EDM Machine (4-Axis, 300kg Load)
-
Phone
+86-0523-86268788 +86-13815960366 +86-13912191163Email
[email protected]Address
No. 366, Yusheng Road Jiulong Town, Hailing District Taizhou City, China
Copyright © Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. All Rights Reserved.
Custom edm machine for sale
wholesale edm machine manufacturers
