

 English
 русский
 عربى


Lu Qianwen — Overseas Sales Manager
Home / Author / Lu Qianwen — Overseas Sales Manager / DK60BC Medium-Speed Wire EDM Machine: High-Capacity Precision for Large and Heavy Workpieces
DK60BC Medium-Speed Wire EDM Machine: High-Capacity Precision for Large and Heavy Workpieces
2026-09-28
Modern toolmaking and precision manufacturing increasingly require a wire electrical discharge machining solution that can combine large working capacity, stable cutting performance, reliable accuracy, and economical operation. The DK60BC CNC medium-speed wire EDM machine is designed for precisely this purpose. With a maximum cutting thickness of 800 mm, a maximum worktable load of 800 kg, X/Y travel of 600 × 800 mm, and four-axis X, Y, U, and V linkage, it is positioned as the largest and most capable model in its medium-speed wire-cut EDM series.
The machine is intended for manufacturers that process oversized molds, heavy industrial components, aerospace parts, complex dies, and thick electrically conductive materials. Instead of being limited to small or medium workpieces, the DK60BC provides the mechanical structure, worktable capacity, wire-guiding stability, and control functions required for demanding large-format applications.
Its performance is supported by an X8/AUTOCUT control system, optimized wire feeding, high-precision linear guide support, optional linear scale feedback, multiple-cut capability, and an adaptive discharge power supply. These features allow the DK60BC to address both productivity and surface-quality requirements. It can perform efficient rough cutting while also supporting finishing passes for improved accuracy, dimensional consistency, and surface condition.
Behind the machine is a manufacturer with experience in wire-cut EDM development dating back to 1999. Through continuous investment in product design, casting treatment, machining, inspection, electrical control, and customer support, the company has developed a product portfolio covering medium-speed, high-speed, and large-taper wire EDM equipment. The DK60BC represents the company’s approach to combining proven manufacturing experience with modern CNC control and process automation.
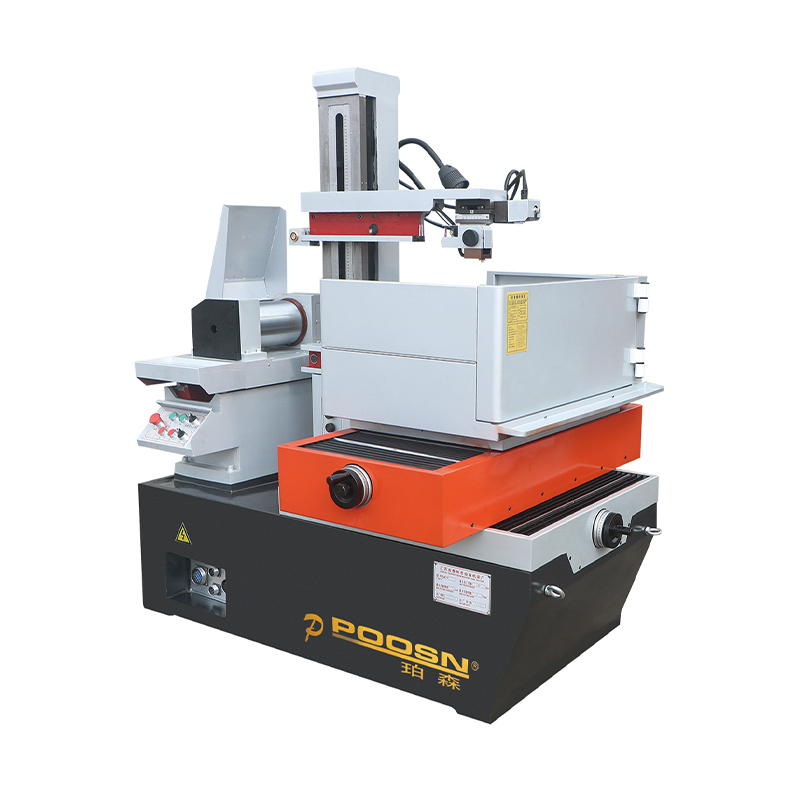
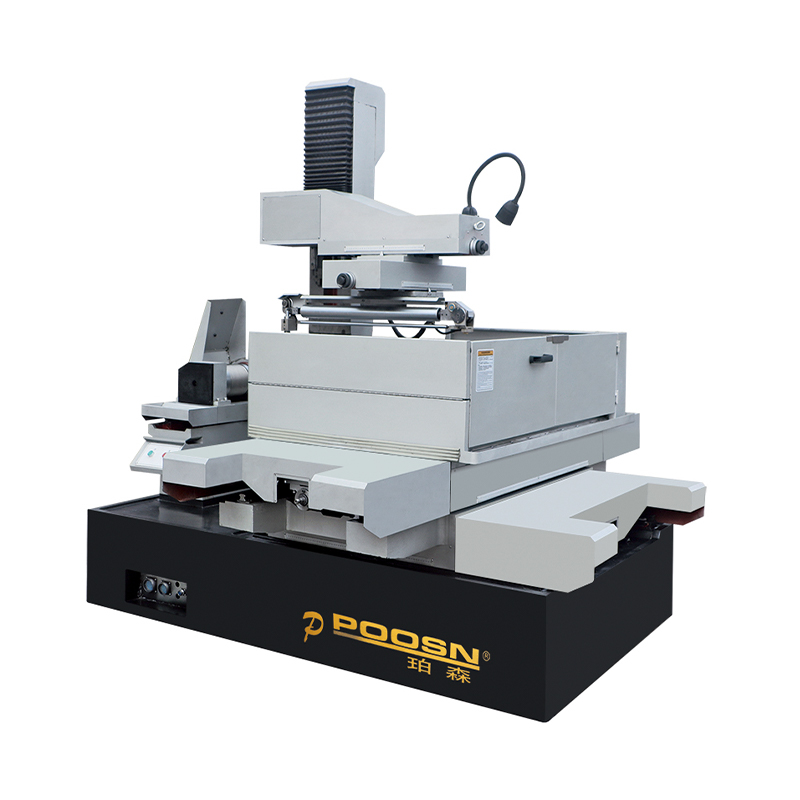
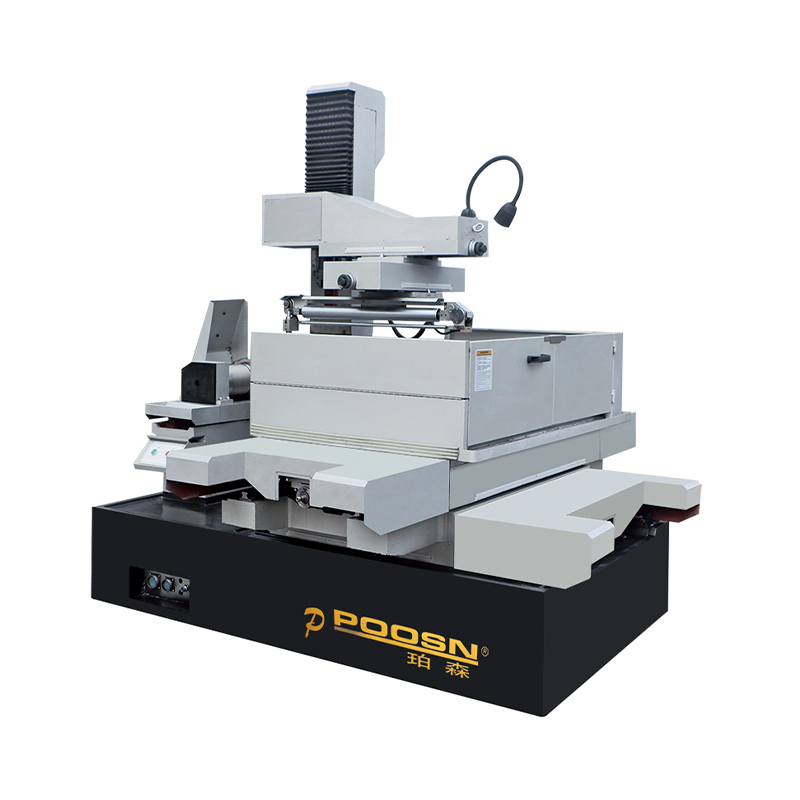
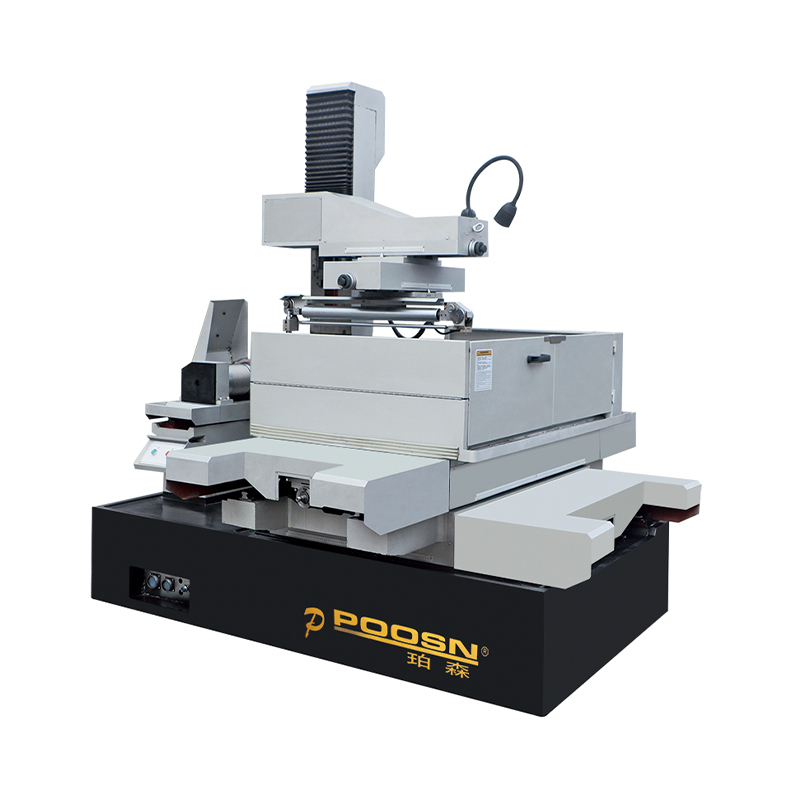
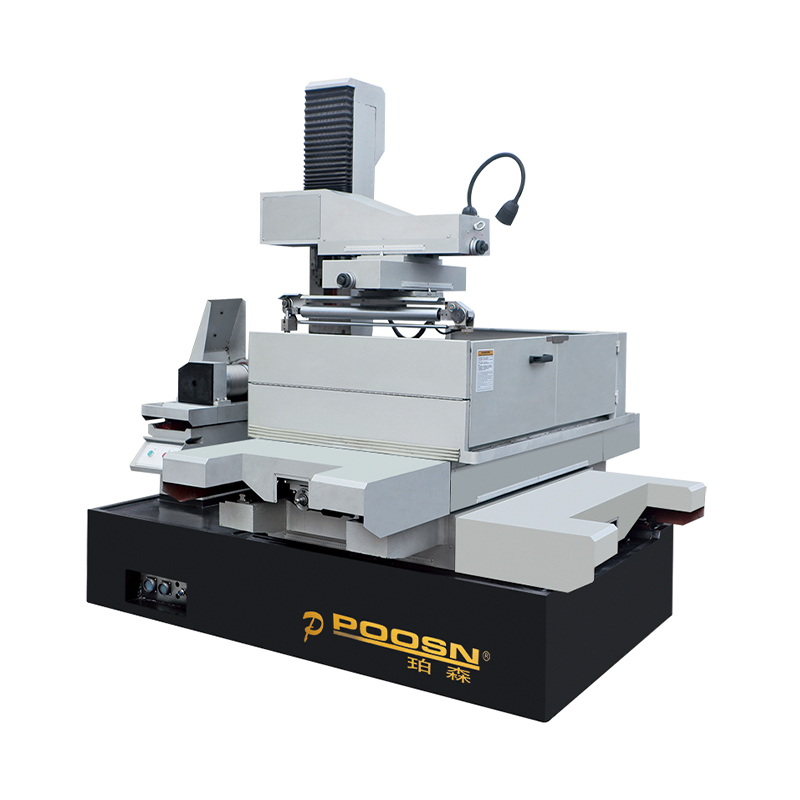
DK60BC CNC Medium-Speed Wire EDM Machine (800kg Load, 800mm Thickness)
Content
- 1 1. The Role of Medium-Speed Wire EDM in Modern Manufacturing
- 2 2. DK60BC Capacity for Oversized Workpieces
- 3 3. Mechanical Architecture and Structural Stability
- 4 4. Adaptive Pulse Power and Discharge Control
- 5 5. Wire Feeding, Tension, and Guide Technology
- 6 6. Multi-Cut Processing and Surface Quality
- 7 7. Taper Cutting and Four-Axis Linkage
- 8 8. CNC Control and Operator Efficiency
- 9 9. Manufacturing Strengths Behind the Product
- 10 10. Comparison with Conventional High-Speed Wire-Cut Machines
- 11 11. Comparison with Smaller Models in the Same Series
- 12 12. Application Areas
- 13 13. Operating Environment and Installation Considerations
- 14 14. Consumables, Maintenance, and Operating Cost
- 15 15. Customization Options
- 16 16. Quality Assurance and International Service
- 17 17. Recommended Selection Process
- 18 18. Conclusion
- 19 Questions and Answers
- 19.1 Q1: What type of production is the DK60BC designed for?
- 19.2 Q2: What is the main advantage of the DK60BC over smaller DK-BC models?
- 19.3 Q3: Can the DK60BC cut hardened steel and carbide?
- 19.4 Q4: Does the machine support multiple finishing cuts?
- 19.5 Q5: What is the standard taper capability?
- 19.6 Q6: What control system does the DK60BC use?
- 19.7 Q7: Is linear scale feedback available?
- 19.8 Q8: What surface roughness can the DK60BC achieve?
- 19.9 Q9: Does the machine require a climate-controlled workshop?
- 19.10 Q10: What after-sales support is provided?
- 19.11 Q11: Can the DK60BC be customized?
- 19.12 Q12: What information should a customer provide when requesting a quotation?
- 20 References
- 21 Product: DK60BC CNC Medium-Speed Wire EDM Machine (800kg Load, 800mm Thickness)
1. The Role of Medium-Speed Wire EDM in Modern Manufacturing
Wire electrical discharge machining removes electrically conductive material through controlled electrical discharges between a continuously moving electrode wire and the workpiece. Because the process does not depend on conventional mechanical cutting force, it can machine hardened steels, tool steels, carbide, titanium alloys, stainless steels, copper alloys, aluminum alloys, and other conductive materials regardless of their mechanical hardness.
This characteristic is especially valuable in moldmaking and precision component production. A hardened die block that would require extensive grinding or milling can often be cut directly by wire EDM after heat treatment. Internal profiles, narrow slots, intricate contours, sharp corners, and taper features can be produced without applying significant cutting pressure to the workpiece.
Medium-speed wire EDM occupies an important position between traditional high-speed wire-cut machines and premium slow-feed wire EDM systems. Traditional high-speed machines are often selected for economical rough cutting and general-purpose production. Slow-feed machines can provide excellent surface quality and high precision, but they generally involve higher initial investment, consumable costs, and operating requirements. A modern medium-speed system seeks to combine practical operating cost with improved accuracy and multiple-pass finishing.
The DK60BC is designed around this balanced manufacturing model. Its wire feed system supports controlled reciprocating operation, while its control system can coordinate roughing, semi-finishing, and finishing strategies. This makes the machine suitable for companies that need more than basic blanking but do not want to dedicate every application to a high-cost slow-wire machine.
Large workpieces introduce additional challenges. As thickness increases, flushing becomes more difficult, wire deflection becomes more significant, and heat and debris can influence the discharge gap. The machine must maintain rigidity and wire tension over a substantial cutting depth. The DK60BC addresses these issues through its reinforced structure, high-pressure flushing options, wire-guiding components, stable tension management, and process compensation functions.
2. DK60BC Capacity for Oversized Workpieces
The most visible advantage of the DK60BC is its large work envelope. The machine provides an X-axis travel of 600 mm and a Y-axis travel of 800 mm. Its worktable measures approximately 840 × 1,160 mm, while the processing slot is approximately 860 × 1,200 mm. These dimensions provide the space needed for large molds, plates, dies, fixtures, and heavy industrial components.
The maximum rated cutting thickness is 800 mm. This capability allows the DK60BC to process workpieces that are outside the practical range of many smaller medium-speed wire machines. Thick workpieces are common in heavy machinery, large-scale stamping dies, forging tools, aerospace structures, and specialized industrial tooling.
Workpiece mass is equally important. The maximum worktable load is 800 kg, giving manufacturers the ability to load substantial components without dividing them into smaller sections or using additional support arrangements. A high load rating can also reduce setup compromises, particularly when the workpiece must be mounted with fixtures, clamping plates, reference blocks, or auxiliary supports.
The large capacity does not mean that the machine is intended only for rough industrial cutting. Its stated linear accuracy of 0.005 mm and taper accuracy of 0.01 mm support precision applications involving large molds and close-fitting components. The machine is also specified for a maximum cutting efficiency of approximately 10,000 to 16,000 mm²/h, depending on operating conditions, workpiece material, thickness, control cabinet selection, and cutting strategy.
A large machine must maintain geometric stability under load. For this reason, the DK60BC uses a high-rigidity body structure and reinforced casting design. Long-duration aging treatment is applied to cast components to reduce internal stress and help maintain dimensional stability during prolonged operation. High-strength resin sand casting and reinforced ribs contribute to vibration damping, rigidity, and long-term accuracy.
These design choices are particularly important when cutting large sections. Even small structural movements can become visible as dimensional variation, taper deviation, poor perpendicularity, or inconsistent surface patterns over a long cutting path. A rigid and properly stabilized machine body creates a more reliable foundation for accurate motion control.
2.1 Principal DK60BC specifications
| Parameter | DK60BC Specification |
|---|---|
| Worktable size | 840 × 1,160 mm |
| X/Y travel | 600 × 800 mm |
| Processing slot size | 860 × 1,200 mm |
| Maximum cutting thickness | 800 mm |
| Maximum worktable load | 800 kg |
| U/V travel | 60 × 60 mm |
| Maximum standard taper | ±6° / 80 mm |
| Electrode wire diameter | 0.18 mm with wire guide |
| Wire feed speed | 1–11 m/s, frequency controlled |
| Maximum wire storage length | Approximately 350 m |
| Maximum cutting efficiency | 10,000–16,000 mm²/h |
| Best stated surface roughness | Ra ≤ 2.5 μm |
| Controlled axes | X, Y, U, and V four-axis linkage |
| Machine weight | Approximately 2,500 kg |
| Overall host dimensions | 2,400 × 2,065 × 2,200 mm |
3. Mechanical Architecture and Structural Stability
Mechanical stability is fundamental to wire EDM performance. The wire may be extremely fine, but the cutting path can be long, the workpiece can be heavy, and the process can last for many hours. Any weakness in the machine frame, guide system, worktable, or transmission assembly can affect final geometry.
The DK60BC uses a reinforced machine body developed for large workpieces. Its cast structure is designed to resist deformation under table loading and cutting forces generated by flushing and wire movement. Although wire EDM produces little conventional cutting force, hydraulic pressure, wire tension, thermal variation, and the mass of the workpiece still influence machine behavior.
Long-duration aging treatment of castings is an important manufacturing step. Newly cast metal can contain internal stresses that may gradually release during machining or service. If these stresses are not controlled, the machine structure may experience slow dimensional movement. Aging helps stabilize the material before precision machining and assembly.
The company’s manufacturing process combines casting, aging, precision machining, component assembly, electrical integration, and final inspection. Each stage influences the next. A carefully designed control system cannot compensate fully for an unstable casting, and a rigid casting cannot deliver its potential without properly aligned guideways and transmission components.
The DK60BC is equipped with high-precision linear guide support. Compared with conventional sliding guide systems, linear guides can reduce friction, improve motion response, and provide consistent movement over the full travel range when correctly installed and maintained. This is advantageous for both straight-line cutting and complex interpolated paths.
Transmission components are optimized to reduce mechanical lag. During wire EDM, the machine must respond to changes in path direction and cutting conditions without introducing excessive positional error. Reduced backlash and improved transmission response help the electrode wire follow the programmed contour more accurately.
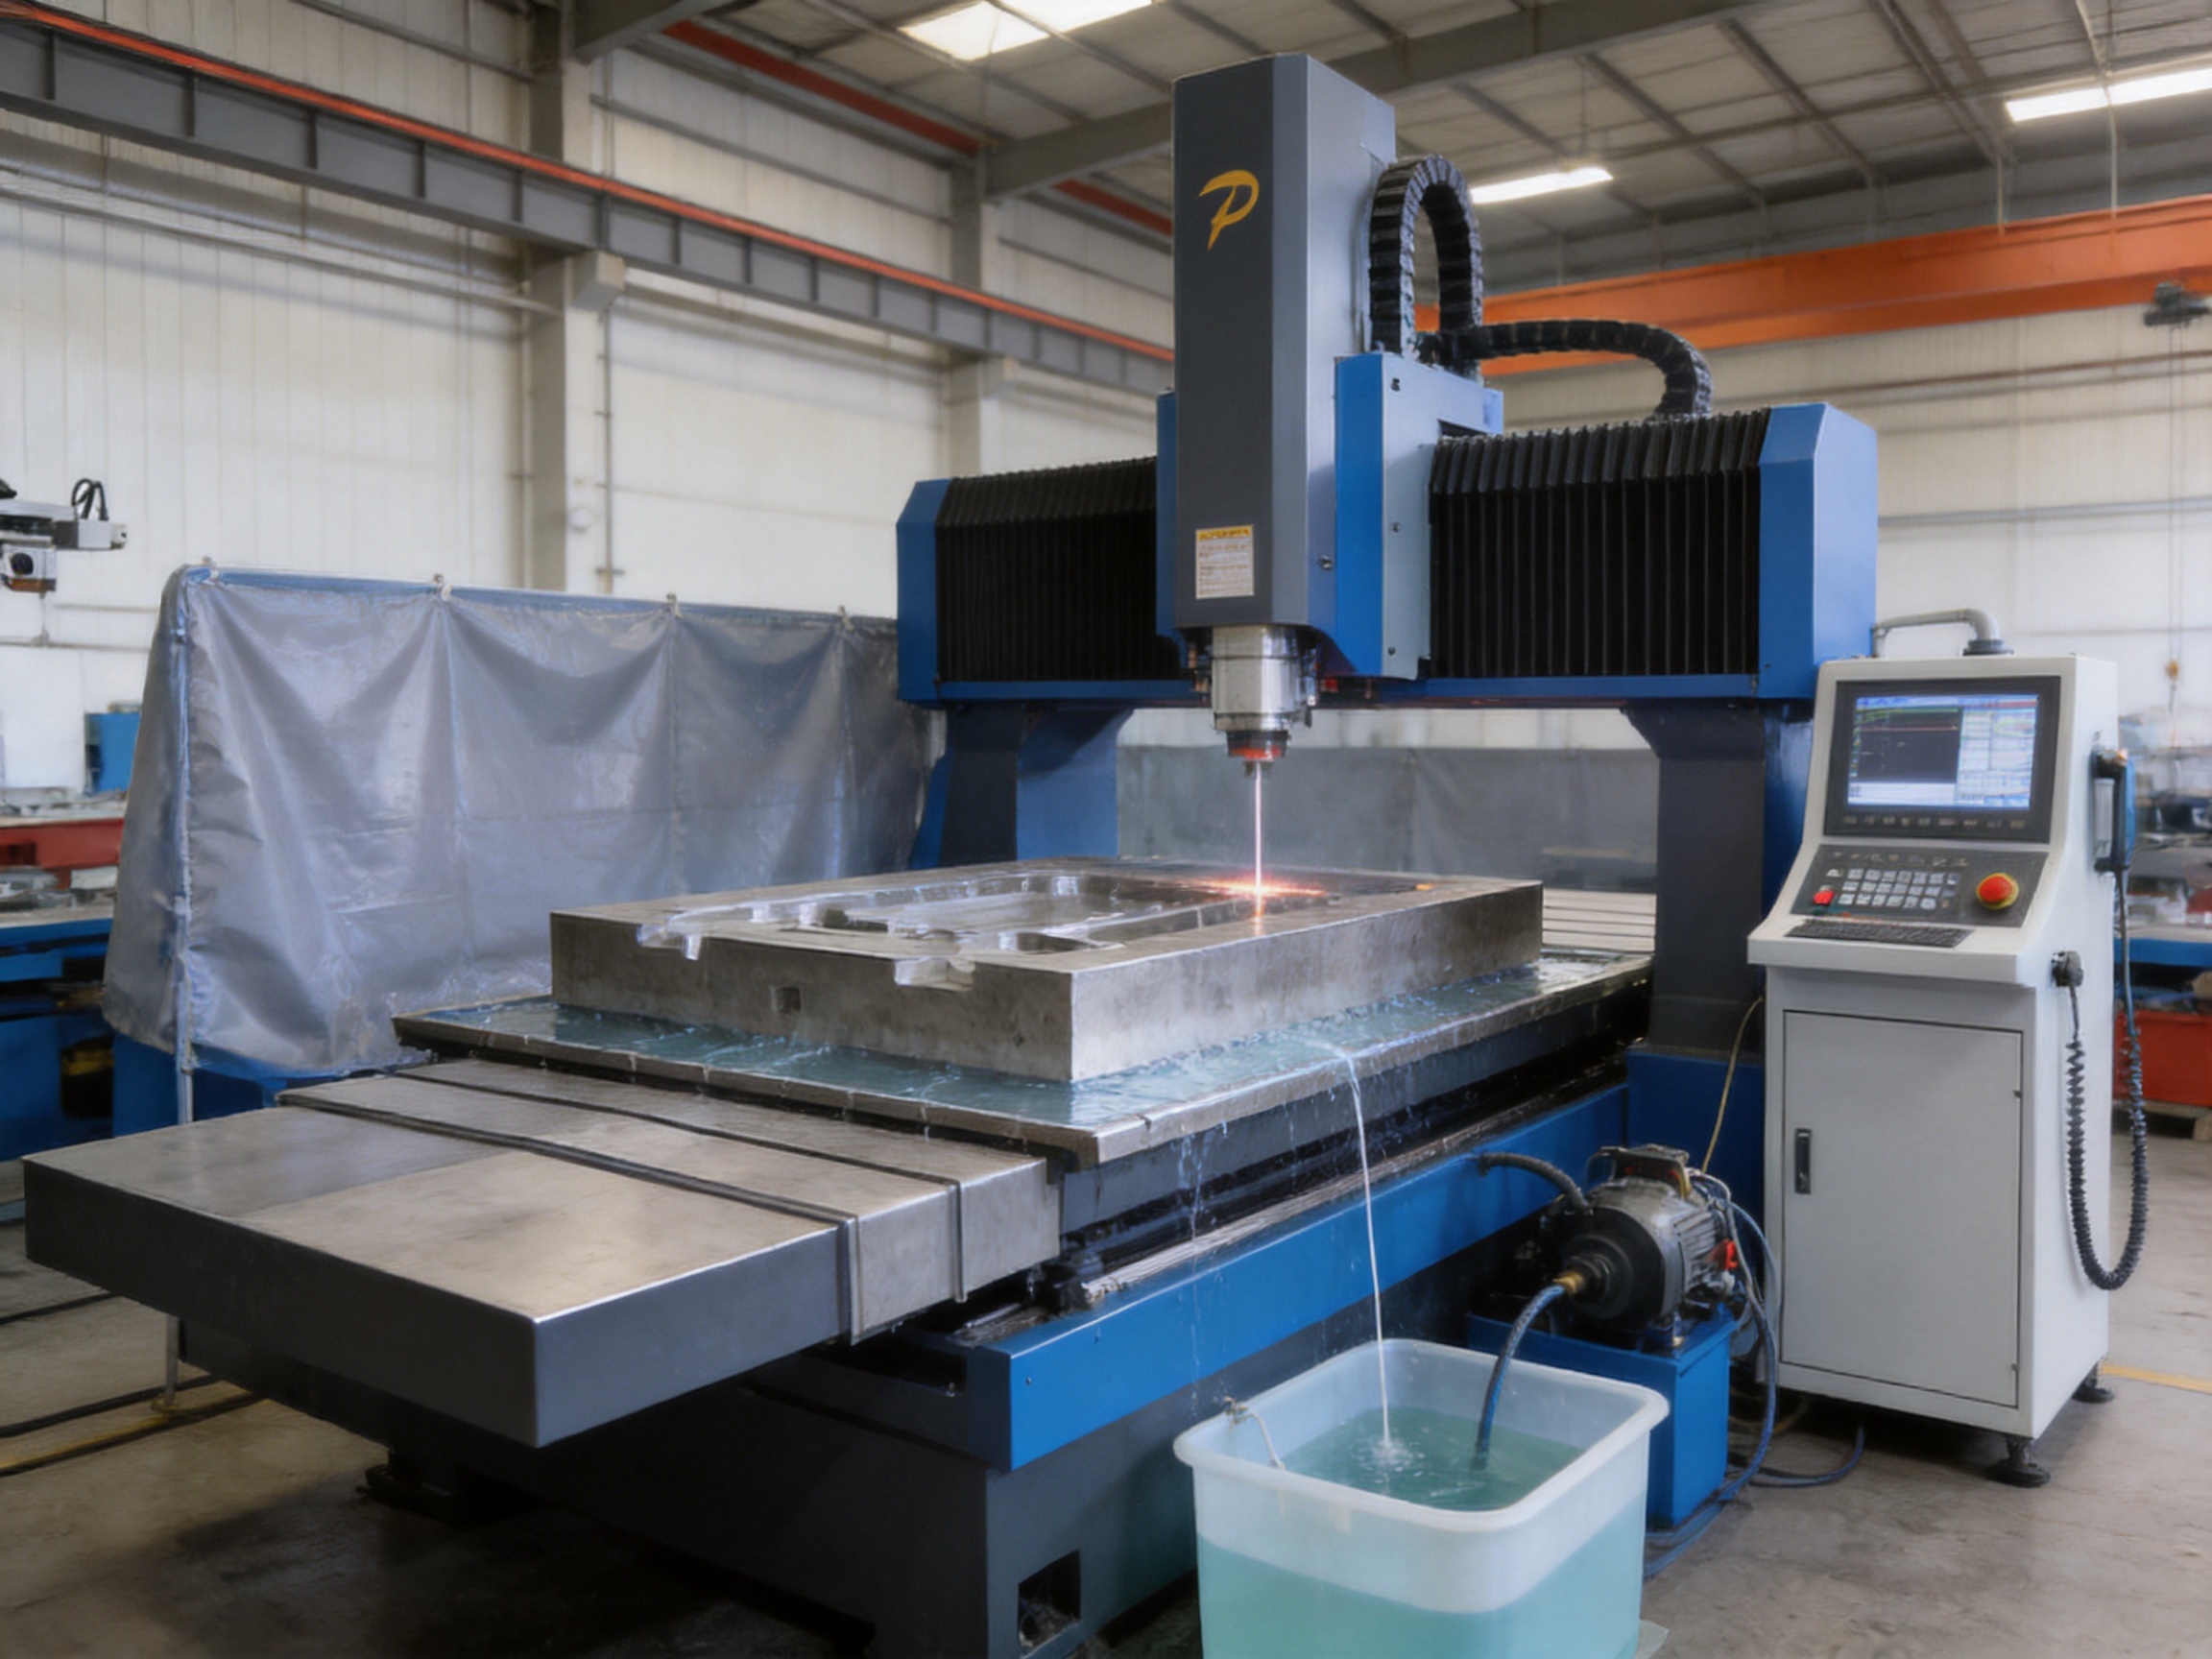
For customers requiring enhanced feedback, a linear scale is available as an option. A scale-based feedback system can provide additional information about actual axis position and support higher-level compensation. This option is especially relevant to manufacturers producing large precision molds, close-tolerance dies, and components where repeatability is more important than basic cutting capacity alone.
4. Adaptive Pulse Power and Discharge Control
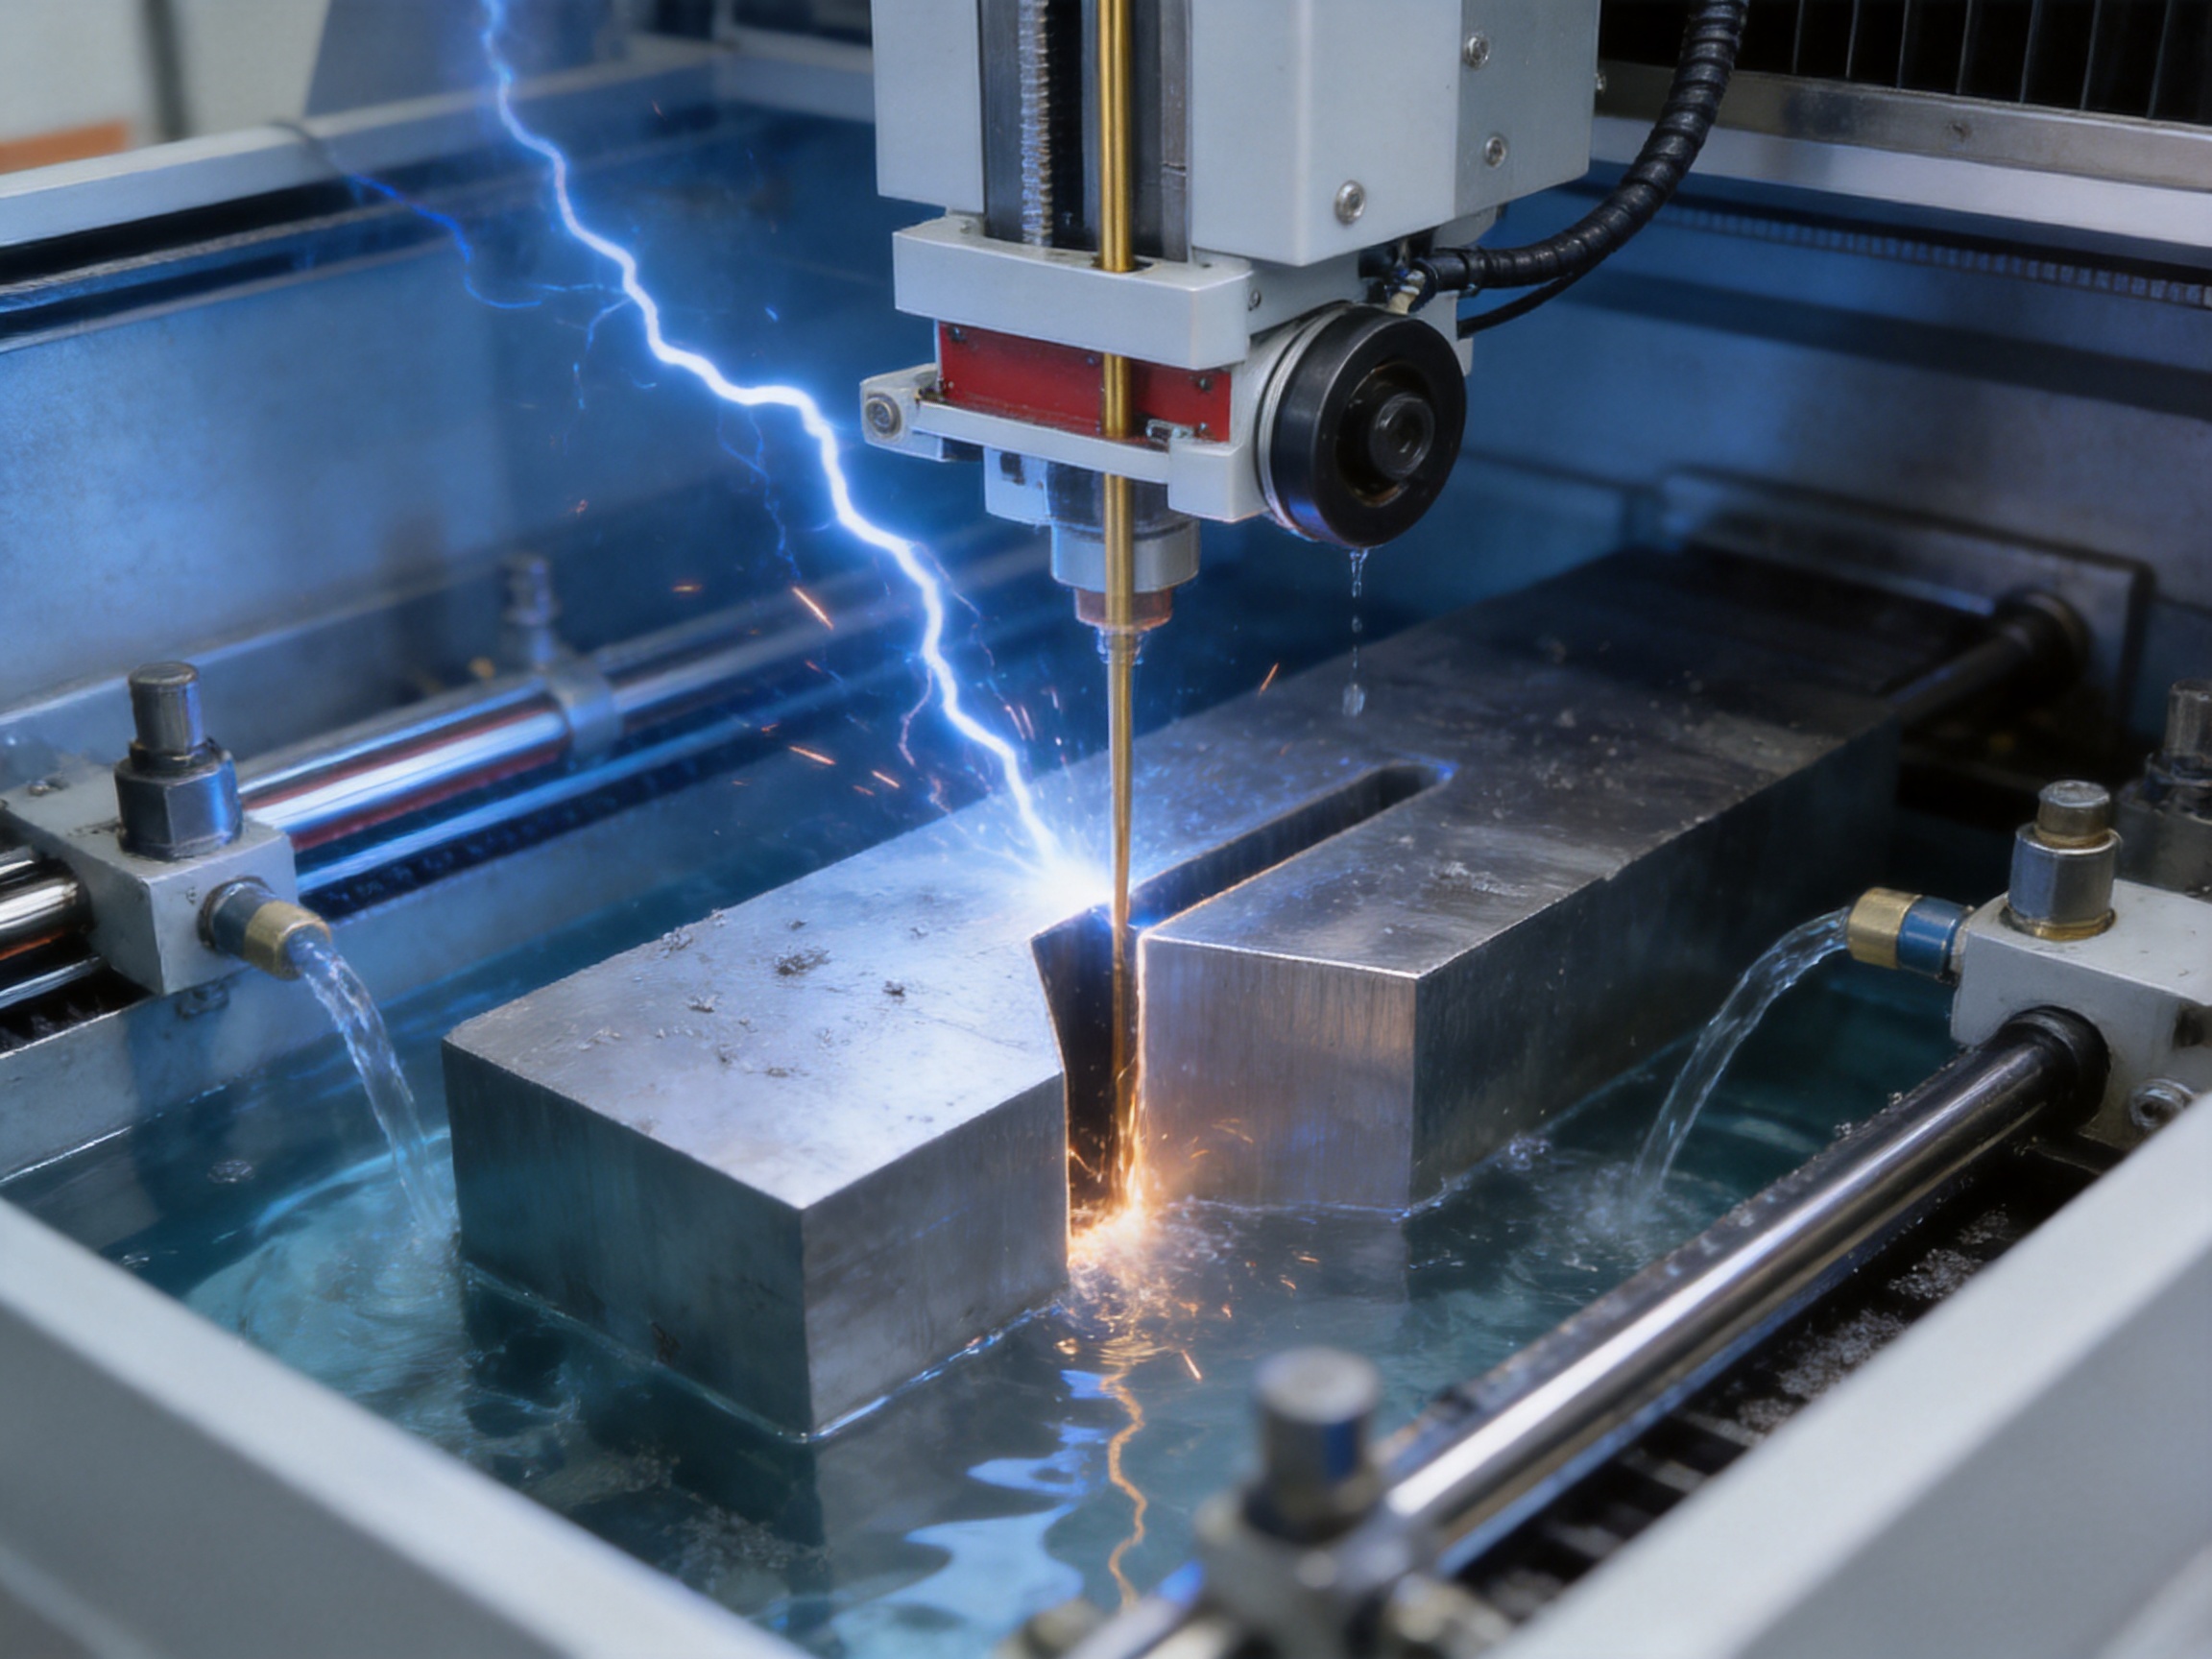
The quality and productivity of wire EDM depend heavily on the stability of the electrical discharge. Each spark must remove material efficiently without causing excessive wire breakage, unstable arcing, deep recast layers, or unacceptable surface damage. The DK60BC uses an adaptive pulse power supply that monitors the discharge gap and adjusts pulse energy according to process conditions.
During rough cutting, the system can prioritize material removal. Higher-frequency or higher-energy pulses are used to remove material efficiently and maintain practical production rates. Roughing is normally focused on creating the required profile while leaving a controlled allowance for subsequent finishing passes.
During finishing, the system can reduce pulse energy and apply finer discharge conditions. Lower-energy pulses help improve surface quality and reduce the thickness of the recast layer. This transition from high-productivity roughing to controlled finishing is one of the central advantages of a modern medium-speed wire EDM platform.
Real-time discharge monitoring can also help reduce the risk of unstable machining. If the gap condition changes because of debris accumulation, workpiece thickness, flushing variation, or a change in material, the controller can adjust feed and discharge parameters. This adaptive approach is more reliable than operating with fixed settings under every condition.
The maximum processing current is specified as 6 A, with an electrical capacity of 2.5 KVA. The standard power supply is 3N 380 V with a tolerance of ±10 percent. Actual installation should always be confirmed against local electrical regulations, site conditions, grounding requirements, and the final machine configuration.
Electrical stability is also affected by the dielectric system. The DK60BC uses water-based dielectric processing supported by filtration and flushing. A clean dielectric environment helps stabilize the spark gap and reduces the influence of conductive debris. Optional high-pressure water equipment can improve flushing in deep or thick cutting applications.
5. Wire Feeding, Tension, and Guide Technology
Wire movement is a major factor in dimensional accuracy and surface consistency. The DK60BC uses a controlled wire feeding system with a stated feed speed range of 1 to 11 m/s. The frequency-controlled system allows the machine to adapt wire movement to the selected process conditions.
The standard electrode wire diameter is 0.18 mm with a wire guide. The wire storage length is approximately 350 m, while the maximum travel of the wire drum is approximately 180 mm. These specifications support continuous operation and practical wire management during production.
A constant-tension dynamic compensation system is used to reduce wire vibration and movement instability. When the wire reciprocates through the cutting zone, tension can vary because of acceleration, deceleration, friction, guide contact, and changes in the cutting load. Dynamic compensation helps keep the wire aligned and reduces the possibility of visible stripe interference or inconsistent kerf geometry.
Wire stability becomes even more important when cutting thick workpieces. Inside an 800 mm section, the wire must maintain its intended trajectory over a substantial distance. Wire lag or deflection can affect perpendicularity, especially when flushing pressure is high or debris evacuation is difficult. Reinforced guide wheel assemblies, precision wire guides, waterproof guide wheels, and stable tension management work together to reduce these effects.
The machine also incorporates easy wire-threading waterproof guide wheel design. This simplifies setup and helps protect guiding components from the working fluid environment. Gem water nozzles and other guide-related components are included in the machine configuration shown for the series.
For certain thick-workpiece applications, users may consider a larger wire diameter or a dedicated thick-workpiece process mode, provided that the final configuration and process parameters are confirmed with the manufacturer. Wire diameter, workpiece thickness, material conductivity, flushing, cutting speed, and desired surface quality must be considered together rather than adjusted independently.
6. Multi-Cut Processing and Surface Quality
A central advantage of the DK60BC over basic high-speed wire-cut equipment is its support for multiple cutting passes. A typical process may include rough cutting, semi-finishing, and one or more finishing passes. Each pass removes a controlled amount of material and progressively improves contour accuracy and surface condition.
Single-pass cutting can be highly productive for blanking, but it may produce more visible machining marks and a rougher surface. Multiple cuts allow the finishing process to remove the disturbed material left by roughing. They can also correct small geometric errors and improve the fit of mating components.
The machine is specified with an optimal surface roughness of Ra ≤ 2.5 μm under suitable conditions. Actual results depend on the material, thickness, cutting height, flushing, wire condition, programming strategy, electrical parameters, and number of finishing passes. As with all EDM equipment, published values should be interpreted as process capabilities rather than guaranteed results for every application.
For moldmaking, surface consistency can be as important as average roughness. A stable wire path, controlled discharge, clean dielectric, and rigid machine structure help minimize irregular marks across the cut surface. This is particularly valuable for punch and die components, inserts, precision templates, and parts that require reliable assembly clearance.
The DK60BC can support applications that require both throughput and finish quality. A manufacturer may use high-efficiency settings for roughing and then apply lower-energy finishing conditions where appearance, edge quality, and dimensional accuracy are critical. This flexible production approach allows the machine to serve more than one role within a workshop.
7. Taper Cutting and Four-Axis Linkage
The DK60BC includes U/V taper control with 60 × 60 mm travel and X, Y, U, and V four-axis linkage. Its standard maximum cutting taper is specified as ±6° over 80 mm. Taper cutting enables the top and bottom profiles of a workpiece to differ according to a programmed angle or contour.
Taper capability is useful in stamping dies, extrusion tooling, forming tools, slanted inserts, and components requiring draft or clearance. It can also support the production of profiles where the upper and lower contours are intentionally offset.
Accurate taper cutting requires more than simply tilting the wire. The control system must coordinate X/Y movement with U/V movement while accounting for workpiece thickness, wire position, guide geometry, and the programmed profile. Mechanical rigidity and stable wire tension are also essential because taper errors can become more visible over thick sections.
Optional large-taper configurations may be available for applications requiring angles beyond the standard specification. Such applications should be reviewed by the manufacturer’s engineering team because large taper cutting can require changes to the wire frame, guide arrangement, flushing approach, and process parameters.
8. CNC Control and Operator Efficiency
The DK60BC uses an X8/AUTOCUT programming and control system. The control platform is designed to simplify programming, machining setup, process monitoring, and multi-pass cutting management. Depending on the final configuration, the control cabinet may be supplied as the standard ZHZK-03 model or an optional ZHZ-09G model.
Graphical programming functions can support the import and processing of complex profiles. Where available in the selected configuration, DXF or DWG data can reduce the need for manual coordinate entry. This can help shorten setup time and reduce programming mistakes when producing intricate contours.
Automatic edge finding and centering functions can also assist workpiece alignment. Correct datum setting is particularly important for large components, where a small setup error can affect a long cutting path. Simplified positioning functions can reduce dependence on manual measurement and make repeat jobs more consistent.
Process databases and parameter libraries help operators select cutting conditions according to material type and workpiece thickness. While experienced technicians remain valuable, a structured database can reduce the amount of trial and error required for common materials such as tool steel, stainless steel, carbide, copper alloys, aluminum alloys, and titanium alloys.
The controller can support roughing and finishing routines, adaptive feed control, real-time discharge monitoring, USB data transfer, and network connectivity depending on the installed system. These functions support a more organized production environment and make it easier to transfer programs between design, CAM, and machining workstations.
Operational simplicity is especially valuable when a workshop has multiple machines or when operators have different levels of experience. The manufacturer states that operators with basic CNC knowledge can become proficient after suitable training. English operating documentation and remote technical training can further support overseas customers.
9. Manufacturing Strengths Behind the Product
The performance of a large wire EDM machine depends on the manufacturing system used to produce it. Product specifications alone do not reveal how consistently a machine will perform over time. Casting quality, machining accuracy, assembly discipline, electrical testing, calibration, and final test cutting all influence the delivered result.
The manufacturer has specialized in electrical discharge wire cutting since 1999 and established its current corporate entity in 2017. Its product development history includes medium-speed wire-cutting EDM machines, high-speed wire-cutting machines, large-taper models, and special processing equipment. This product breadth provides experience across different cutting speeds, mechanical layouts, control systems, and application requirements.
Manufacturing begins with a machine structure capable of supporting the intended load and travel range. High-strength resin sand castings and reinforced ribs are used to improve rigidity and vibration damping. Castings undergo aging treatment before precision machining so that the structural material is more stable during later assembly and operation.
Precision machining establishes the reference surfaces for guideways, tables, transmission components, and other critical assemblies. Proper alignment is essential because errors in the base or guide installation can influence positioning, straightness, squareness, and taper performance.
After mechanical assembly, the electrical and control systems are integrated and tested. The machine’s power supply, CNC controller, motors, sensors, wire transport system, flushing equipment, and safety functions must work as a coordinated system. The manufacturer’s production process includes comprehensive inspection from incoming components through final machine assembly.
Before shipment, machines undergo positioning accuracy testing. The company also describes the use of laser interferometer verification and ballbar circularity testing for relevant configurations. These tests provide a structured method for checking axis positioning behavior, repeatability, and circular interpolation performance.
Final test cutting is another important quality-control step. A machine can pass static inspection and still require adjustment under actual discharge conditions. Test cutting helps verify wire movement, electrical stability, flushing, control response, and the relationship between programmed geometry and finished workpiece geometry.
This full-process approach is valuable for customers purchasing large equipment remotely. A machine weighing approximately 2,500 kg and measuring 2,400 × 2,065 × 2,200 mm requires significant installation planning. Receiving a machine that has already been assembled, calibrated, and test-cut can reduce commissioning risk and shorten the time needed to begin production.
10. Comparison with Conventional High-Speed Wire-Cut Machines
The DK60BC belongs to a medium-speed wire EDM category, while the manufacturer also offers high-speed wire-cut products. The two categories serve different production priorities.
High-speed wire-cut machines are often selected for economical rough cutting, general-purpose profiles, and high-volume blanking. Their sliding guide systems and single-pass-oriented operation can provide a practical solution where surface quality requirements are moderate and initial investment must be controlled.
The DK60BC emphasizes linear guide support, multiple-cut capability, large workpiece capacity, and improved finishing. It is therefore more appropriate for precision molds, thick components, and applications where surface quality and dimensional stability are important after rough cutting.
The supplied comparison identifies a maximum cutting speed of up to 180 mm²/min for the DK-BC medium-speed series and up to 120 mm²/min for the DK-77 high-speed series. It also describes medium-speed surface roughness in the Ra 0.8–1.2 μm range under particular process conditions, compared with Ra 1.6–2.5 μm for high-speed equipment. The detailed DK60BC series specification separately lists Ra ≤ 2.5 μm as its best stated surface roughness. Actual values depend on the specific model, control system, material, thickness, and number of passes.
| Feature | DK-BC Medium-Speed Approach | Traditional High-Speed Approach |
|---|---|---|
| Primary focus | Precision cutting and finishing | Economical rough cutting and blanking |
| Guide system | Linear guide support | Sliding guide system in the comparison series |
| Multiple cuts | Supported for roughing and finishing | Primarily single-pass operation |
| Large workpiece capability | DK60BC supports up to 800 kg and 800 mm thickness | Depends on individual model |
| Typical application | Precision molds, thick dies, heavy industrial parts | General profiles, blanking, high-volume rough work |
| Surface-quality potential | Improved through controlled finishing passes | Usually more dependent on single-pass conditions |
These categories should not be viewed as mutually exclusive. A factory may use high-speed machines for initial blanking and medium-speed equipment for precision finishing. However, manufacturers that regularly process thick, heavy, and high-value workpieces may prefer the DK60BC as a more complete production platform.
11. Comparison with Smaller Models in the Same Series
The DK60BC is the largest model in the DK-BC family. The DK35BC, DK45BC, and DK50BC provide similar general technology in smaller working envelopes and lower load capacities. Choosing among them should be based primarily on workpiece size, thickness, weight, required travel, and future production plans.
| Model | X/Y Travel | Maximum Thickness | Maximum Load | Typical Application |
|---|---|---|---|---|
| DK35BC | 350 × 450 mm | 450 mm | 300 kg | Small precision parts, dies, and electrodes |
| DK45BC | 450 × 600 mm | 450 mm | 400 kg | Medium molds and mechanical components |
| DK50BC | 500 × 700 mm | 650 mm | 600 kg | Large molds and thick workpieces |
| DK60BC | 600 × 800 mm | 800 mm | 800 kg | Oversized molds and heavy industrial parts |
The smaller models may be more economical when workpieces are consistently compact. Selecting a machine that is too large can increase floor-space, installation, and operating requirements without providing practical benefits. Conversely, selecting a machine that is too small can force workpiece repositioning, additional fixtures, or outsourcing when a larger job arrives.
The DK60BC is the logical choice when production includes extra-large molds, thick plates, heavy dies, aerospace components, or machinery parts approaching the upper limits of the medium-speed series. It also gives a workshop more flexibility for future projects that may exceed current workpiece dimensions.
12. Application Areas
12.1 Large-scale mold manufacturing
Large molds often contain complex contours, deep sections, narrow openings, and hardened materials. The DK60BC can cut large mold components while maintaining controlled wire movement and supporting multiple finishing passes. Its worktable capacity is suitable for large die plates, inserts, and oversized mold elements.
For moldmakers, the ability to perform rough and finish operations on one platform can simplify production planning. It reduces the need to transfer a component between separate machines and helps maintain a consistent datum throughout the cutting process.
12.2 Aerospace components
Aerospace manufacturing requires dimensional reliability, traceable process control, and the ability to work with materials such as titanium alloys, nickel-based alloys, hardened steels, and other conductive engineering materials. Wire EDM is useful for components with intricate profiles or sections that are difficult to machine with conventional cutting tools.
The DK60BC’s large capacity, adaptive discharge control, and optional feedback systems make it suitable for aerospace suppliers that need to process large and complex conductive parts. Actual aerospace qualification requirements must be addressed through the customer’s own quality system and process validation procedures.
12.3 Heavy machinery
Heavy machinery components may be thick, hardened, and difficult to mount on smaller machines. With an 800 kg load rating and 800 mm maximum cutting thickness, the DK60BC is designed for demanding heavy-component work. Applications may include industrial tooling, large machine components, forming parts, and specialized mechanical structures.
12.4 Tool and die production
Tool steels and hardened die materials are among the most common wire EDM applications. The DK60BC can process materials such as D2, A2, H13, SKD11, and other electrically conductive tool steels. It can also handle carbide and conductive alloys where conventional milling would create excessive tool wear or require complex clamping.
12.5 General precision components
The machine is not limited to very large parts. Where a manufacturer values a large work envelope, high load rating, and stable precision, the DK60BC can produce templates, precision plates, fixtures, punches, inserts, and custom components. Its capacity can be particularly useful for job shops that receive varied orders.
13. Operating Environment and Installation Considerations
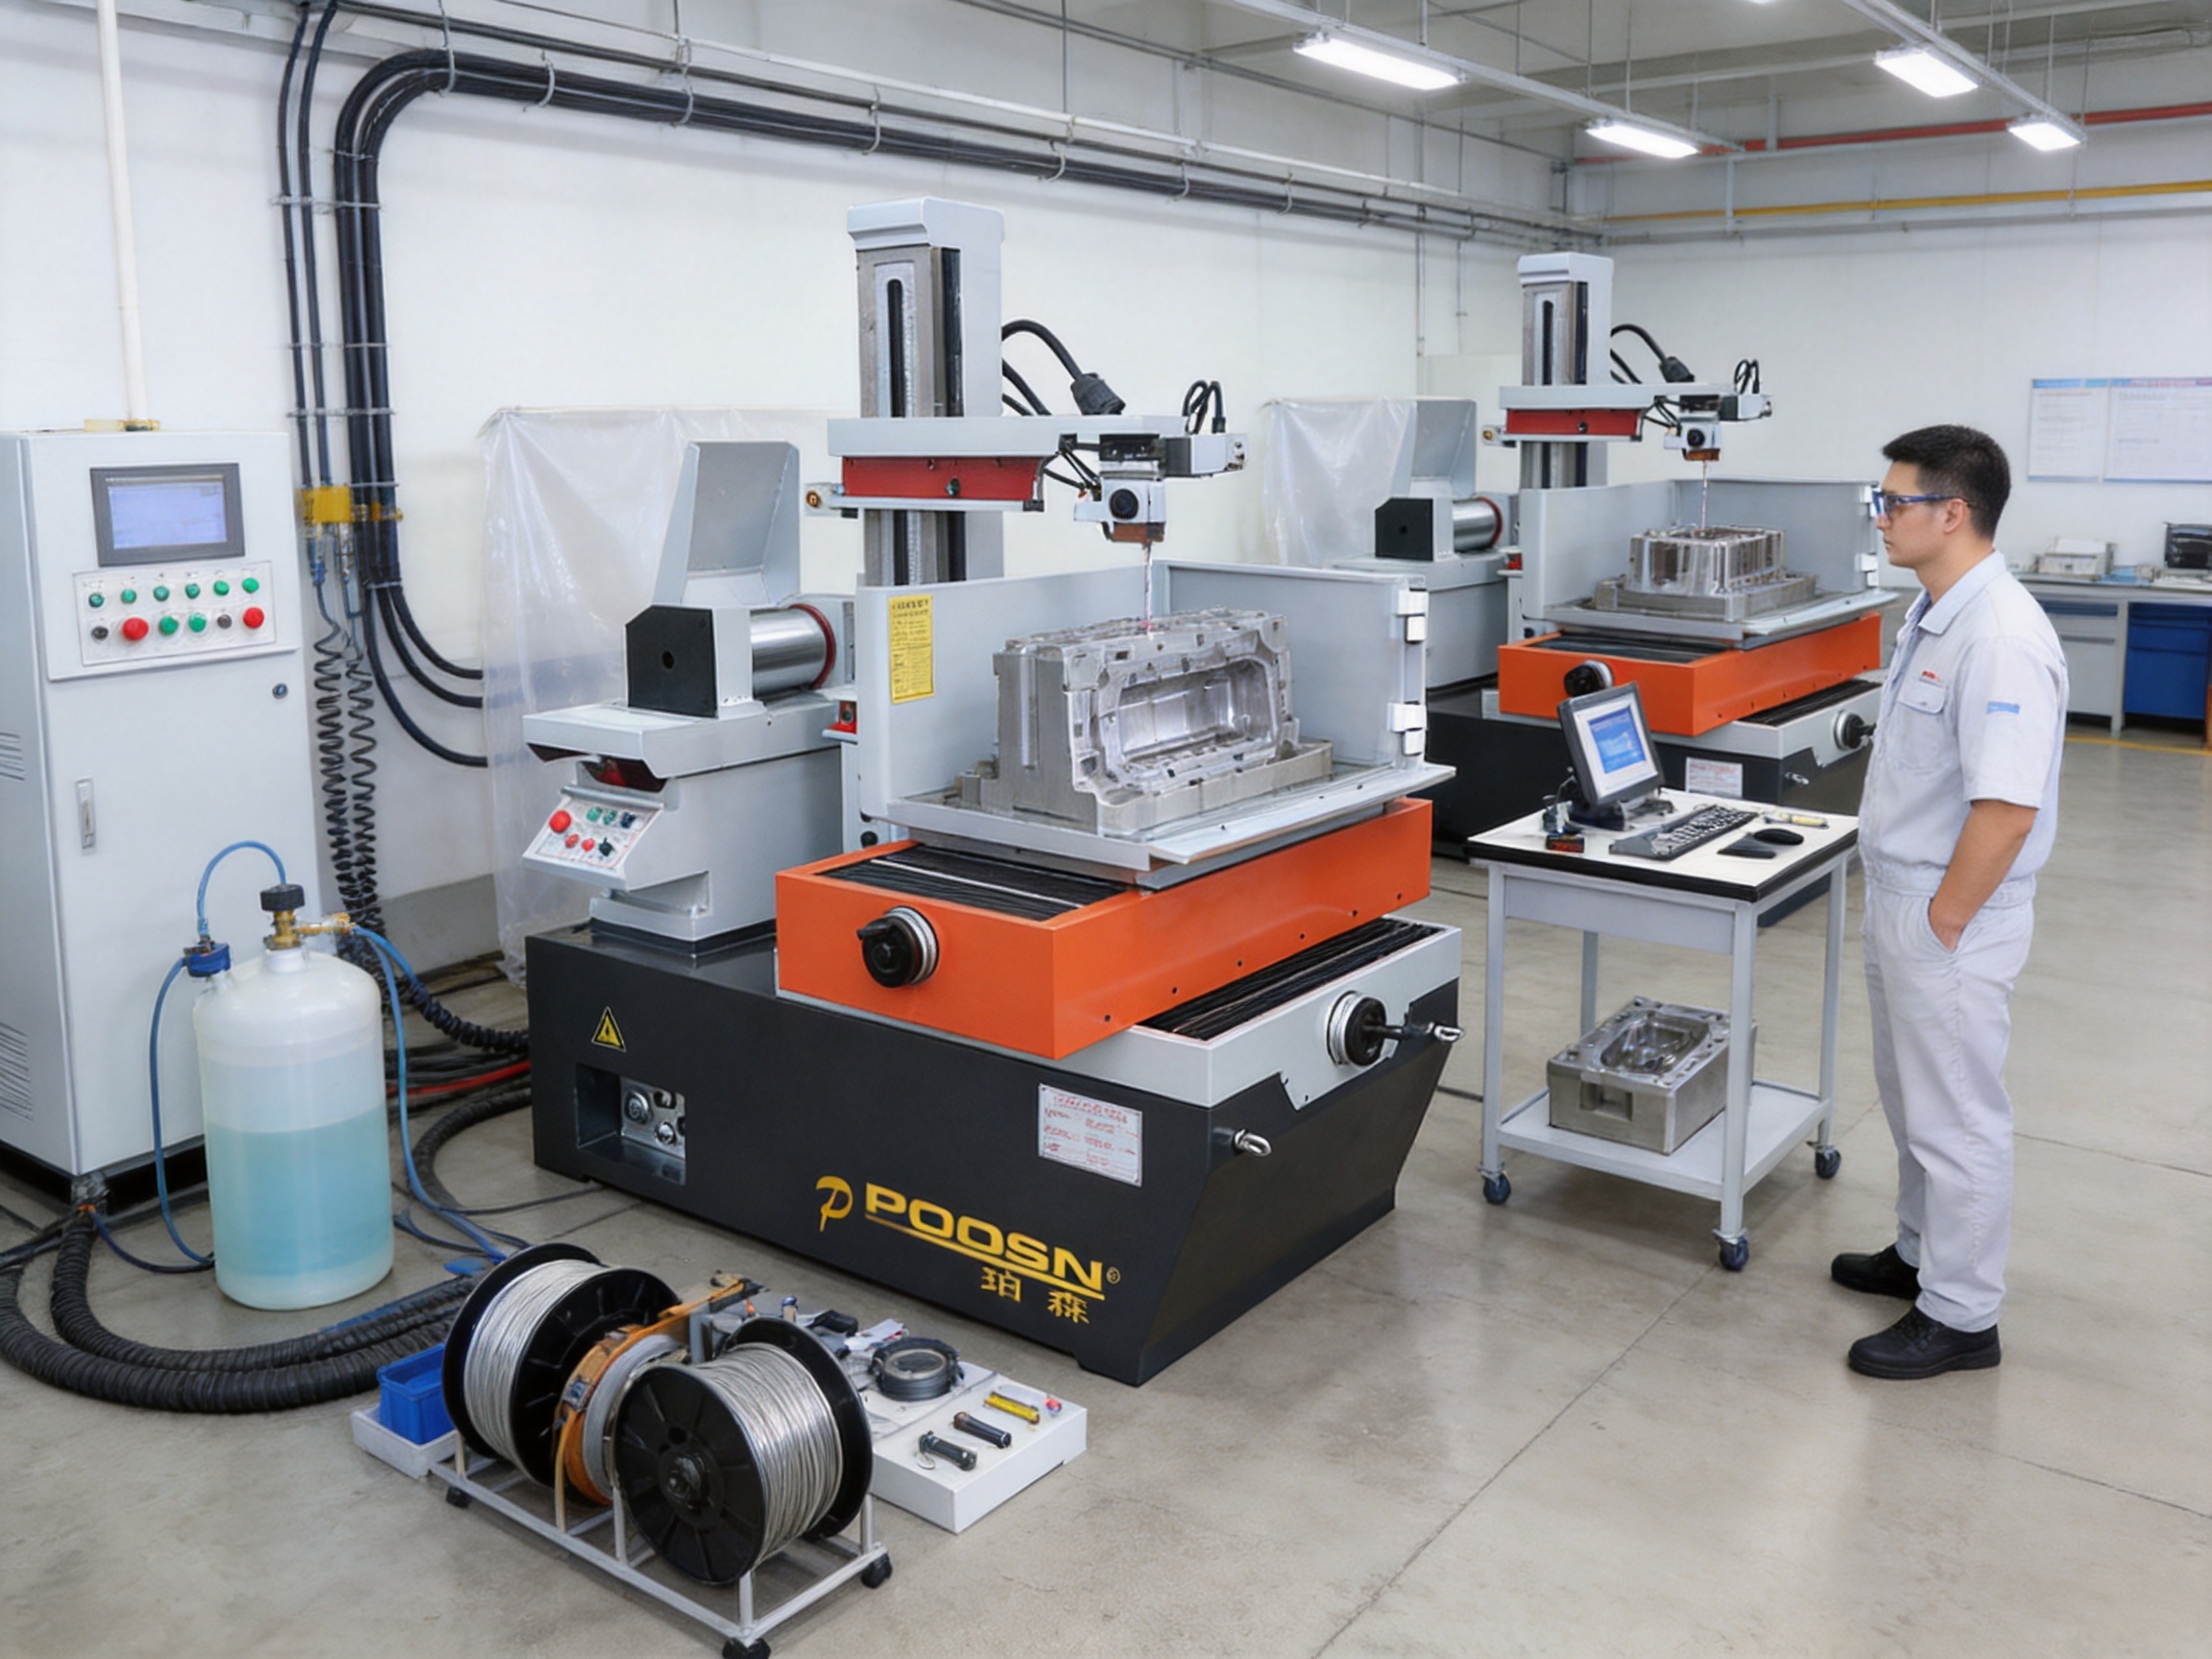
Although the DK60BC is designed for general industrial use, installation quality has a direct effect on performance. The machine should be placed on a suitable foundation capable of supporting its approximately 2,500 kg weight and operating loads. Adequate clearance is required for workpiece loading, maintenance, electrical access, wire replacement, and movement around the machine.
A clean, stable power supply and proper grounding are important for the controller and discharge power system. The installation should follow the electrical requirements of the final machine configuration and local regulations. Voltage fluctuations, poor grounding, and electrical interference can affect control reliability and discharge stability.
Temperature variation should also be considered. The machine is described as suitable for general workshop environments, with an operating range stated in the supplied material as approximately 5–40°C. For the highest precision requirements, particularly tolerances below several micrometers, a temperature-controlled environment is recommended.
Temperature control is not only about operator comfort. Thermal expansion affects the machine structure, guideways, table, workpiece, and dielectric fluid. When a large machine and a large workpiece experience different temperatures, dimensional relationships can change during a long cutting cycle. Stable workshop conditions improve repeatability.
Ventilation should be adequate, and the working area should be kept clean. Dielectric management, filtration, and waste handling should follow the manufacturer’s maintenance instructions. Regular checks of water quality, filters, pumps, nozzles, guide wheels, wire tension, and electrical connections help maintain reliable production.
14. Consumables, Maintenance, and Operating Cost
One of the practical benefits of medium-speed wire EDM is the potential for lower operating cost compared with imported premium slow-feed systems. The supplied information identifies molybdenum wire, guide wheels, guide nozzles, water-based dielectric fluid, and ion-exchange resin as typical consumables.
| Consumable | Typical Service Interval or Life | Maintenance Purpose |
|---|---|---|
| Molybdenum wire, 0.18 mm | Approximately 40–80 continuous operating hours | Provides the cutting electrode |
| Guide wheels | Approximately 6–12 months | Maintains stable wire guidance |
| Guide nozzles | Approximately 3–6 months | Supports flushing and wire positioning |
| Water-based dielectric fluid | Replace approximately every 2–3 months | Maintains discharge and flushing conditions |
| Ion-exchange resin | Approximately 3–6 months | Helps control water conductivity |
These are indicative intervals rather than universal replacement schedules. Actual life depends on cutting hours, material, thickness, water quality, contamination, flushing pressure, wire tension, and maintenance discipline. Operators should monitor cutting stability, surface condition, wire breakage, conductivity, filtration pressure, and guide wear.
Good maintenance protects accuracy as well as cost. Worn guide wheels can increase wire vibration. Blocked filters can reduce flushing. Degraded dielectric quality can destabilize the discharge gap. Incorrect tension can affect straightness and surface consistency. A preventive maintenance program is therefore essential for maintaining the machine’s original performance.
The manufacturer states that the DK-BC series can offer substantially lower consumable costs than imported brands such as Sodick and Makino. The exact comparison depends on machine configuration, local prices, production volume, and process requirements, but the use of economical wire and practical maintenance components can be an important advantage for cost-sensitive manufacturers.
15. Customization Options
The DK60BC can be configured for different production priorities. Standard equipment includes high-precision linear rail support, an environmentally focused waterproof cover, the X8/AUTOCUT control system, and the standard control cabinet arrangement. Optional features can be selected according to application requirements.
A high-pressure water tank can improve flushing for deep, thick, or difficult-to-clean cuts. Linear scales can provide additional axis-position feedback. AC servo drives can be selected instead of standard X/Y stepper drives where the customer requires a different motion-control configuration.
The optional ZHZ-09G control cabinet may provide additional control capabilities according to the final system specification. Other potential options described in the supplied material include automatic wire threading, a large-taper wire frame, closed-loop glass scales, extended travel, a rotary table, and certification packages for specific markets.
Automatic wire threading can be valuable for multi-cavity molds and unattended production. A large-taper upgrade may be suitable for extrusion dies or components requiring substantial angular variation. A rotary table can support specialized cylindrical or spiral cutting applications, subject to engineering review.
Customization should be discussed before order confirmation because options may affect machine dimensions, electrical requirements, delivery schedule, software configuration, and installation procedures. The manufacturer indicates that standard models may be available with a lead time of approximately 15–25 days, while custom configurations may require an additional 10–15 days. Final lead times should be confirmed for each order.
16. Quality Assurance and International Service
The company’s quality philosophy is based on inspection throughout the production lifecycle rather than relying solely on final inspection. Incoming components, castings, machined surfaces, guide systems, electrical assemblies, and completed machines are checked according to internal and applicable national standards.
Positioning accuracy testing is performed before shipment. Laser interferometer verification can help confirm axis positioning accuracy and repeatability, while ballbar testing can identify circular interpolation behavior. These measurements support more objective machine acceptance and help technicians complete final adjustments.
Export customers also require practical service after the machine leaves the factory. The manufacturer provides remote technical support and maintains spare-part resources for international users. Modular machine design allows many maintenance tasks to be performed by local technicians with remote guidance.
The stated warranty period is 12 months from shipment. Critical spare parts may be dispatched by express courier, and lifetime remote technical support is offered through online communication. Customers should confirm warranty exclusions, response procedures, installation responsibilities, and spare-part terms in the final sales agreement.
The company’s products have been supplied within China and exported to Southeast Asia, West Asia, Europe, and the Americas. International experience is valuable because export customers often require different electrical standards, documentation, packaging, certification, language support, and shipping arrangements.
For transportation, the machine can be shipped by full-container sea freight, less-than-container-load sea freight, or rail freight for selected regions. Typical transit estimates are approximately 25–45 days for full-container sea freight, 30–50 days for less-than-container-load freight, and 25–35 days for rail freight, depending on destination and logistics conditions.
17. Recommended Selection Process
Before selecting the DK60BC, buyers should prepare a clear application profile. The most important information includes maximum workpiece length, width, height, weight, material type, hardness, required contour accuracy, surface-finish target, taper requirement, expected production volume, and available installation space.
Workpiece dimensions should be evaluated together with clamping and flushing requirements. A component may fit within the nominal travel but still require additional space for fixtures, reference edges, support blocks, or clearance around the guide system. Heavy parts should be assessed for safe loading and stable support.
Material conductivity and thickness influence cutting conditions. Hardened tool steel, carbide, titanium, copper, and aluminum may require different discharge parameters, wire speeds, flushing strategies, and finishing schedules. Customers should provide representative drawings or sample workpieces when requesting a technical recommendation.
Surface finish requirements should be stated clearly. If the component requires only functional blanking, a high-productivity single roughing strategy may be adequate. If the part is a precision mold insert or a close-fitting die, multiple finishing passes and optional feedback equipment may be more appropriate.
Taper requirements also require early consideration. Standard DK60BC taper capability is specified as ±6° over 80 mm. If the design requires large taper angles, the customer should request a special configuration before production planning. Large-taper machining may affect the wire frame and control strategy.
Finally, buyers should consider future needs. A machine should not be selected only for today’s average job if the workshop expects to expand into large moldmaking, aerospace subcontracting, or heavy machinery components. The DK60BC’s high capacity can provide additional production flexibility, provided the customer has sufficient floor space, lifting equipment, electrical capacity, and operator resources.
18. Conclusion
The DK60BC CNC medium-speed wire EDM machine is engineered for manufacturers that need high-capacity wire cutting without giving up precision-oriented processing. Its 600 × 800 mm X/Y travel, 800 mm maximum cutting thickness, 800 kg table load, four-axis linkage, and large work envelope make it a strong solution for oversized and heavy workpieces.
Its advantages are not based on capacity alone. The machine combines a rigid aged casting structure, linear guide support, controlled wire feeding, dynamic tension compensation, adaptive pulse power, high-pressure flushing options, multiple-cut processing, and X8/AUTOCUT CNC control. Together, these systems help the DK60BC move beyond basic rough cutting and address the requirements of large precision molds, thick dies, aerospace components, and heavy industrial parts.
Compared with conventional high-speed wire-cut equipment, the DK60BC places greater emphasis on finishing capability, wire-path stability, and large-workpiece precision. Compared with smaller models, it provides substantially greater thickness, load, and travel capacity. Compared with premium imported equipment, it offers a practical medium-speed architecture with potentially lower consumable and ownership costs.
The manufacturing foundation behind the machine is equally significant. Decades of wire-cut EDM experience, casting stabilization, precision machining, full-process inspection, laser-based accuracy verification, test cutting, export service, and remote technical support contribute to a more complete equipment solution.
For companies processing large conductive workpieces and seeking an economical path to repeatable wire EDM production, the DK60BC offers a combination of size, stability, automation, and application flexibility. Its final performance will depend on proper installation, suitable process parameters, regular maintenance, and correct configuration, but its design provides the technical foundation for demanding modern manufacturing work.
Questions and Answers
Q1: What type of production is the DK60BC designed for?
The DK60BC is designed for extra-large molds, heavy machinery components, aerospace parts, thick dies, large tooling, and other electrically conductive workpieces requiring a maximum cutting thickness of up to 800 mm and a maximum table load of up to 800 kg.
Q2: What is the main advantage of the DK60BC over smaller DK-BC models?
The DK60BC provides the largest working range and load capacity in the series. It offers 600 × 800 mm X/Y travel, an 800 mm maximum cutting thickness, and an 800 kg maximum worktable load. It is intended for workpieces that exceed the practical capacity of the DK35BC, DK45BC, or DK50BC.
Q3: Can the DK60BC cut hardened steel and carbide?
Yes. Wire EDM can process electrically conductive materials regardless of conventional hardness. Typical materials include tool steels, stainless steels, cemented carbide, titanium alloys, copper alloys, aluminum alloys, and selected conductive high-temperature materials.
Q4: Does the machine support multiple finishing cuts?
Yes. The DK-BC medium-speed series supports multiple-cut processing. Roughing, semi-finishing, and finishing passes can be programmed to improve dimensional accuracy and surface quality compared with a basic single-pass operation.
Q5: What is the standard taper capability?
The standard taper device provides U/V travel of 60 × 60 mm and a maximum stated taper of ±6° over 80 mm. Larger taper angles may be available with an optional large-taper configuration and should be confirmed with the manufacturer’s engineering team.
Q6: What control system does the DK60BC use?
The machine uses an X8/AUTOCUT programming and control system. The standard control cabinet is specified as ZHZK-03, with ZHZ-09G available as an option. The final functions depend on the selected configuration.
Q7: Is linear scale feedback available?
Yes. Linear scale feedback is listed as an optional feature. It can be considered for applications that require enhanced position feedback, repeatability, and higher confidence in precision machining.
Q8: What surface roughness can the DK60BC achieve?
The series specification lists an optimal surface roughness of Ra ≤ 2.5 μm. Other supplied comparison data describes lower Ra values for particular DK-BC process conditions. Actual performance depends on material, thickness, flushing, electrical parameters, wire condition, and the number of finishing passes.
Q9: Does the machine require a climate-controlled workshop?
The machine is designed for general workshop conditions, but a stable temperature-controlled environment is recommended for the highest precision work. Temperature stability becomes increasingly important when machining large workpieces or tolerances of only a few micrometers.
Q10: What after-sales support is provided?
The manufacturer provides a 12-month warranty from shipment, remote technical support, spare-parts assistance, operating documentation, and online training support. Specific warranty and service conditions should be confirmed in the final purchase agreement.
Q11: Can the DK60BC be customized?
Potential options include a high-pressure water tank, linear scales, servo drives, large-taper equipment, automatic wire threading, extended travel, rotary-table configurations, advanced control cabinets, and certification packages. Custom requirements should be reviewed before ordering.
Q12: What information should a customer provide when requesting a quotation?
The customer should provide workpiece dimensions, maximum thickness, weight, material, desired accuracy, surface finish, taper angle, production volume, drawings, power conditions, destination country, and any requirements for automation, certification, or special control functions.
References
1. Technical specification data supplied for the DK60BC and DK-BC medium-speed wire EDM series.
2. Product information concerning the X8/AUTOCUT CNC control system, wire feeding system, taper device, and machine configurations.
3. GB/T 7926-2015, applicable accuracy requirements and testing principles for wire-cut electrical discharge machine tools.
4. Manufacturer-provided information regarding casting aging, precision machining, laser interferometer verification, ballbar testing, and final machine inspection.
5. Manufacturer-provided application information for large molds, aerospace components, heavy machinery parts, tool steels, carbide, stainless steel, titanium alloys, and other conductive materials.
6. Manufacturer-provided comparison data for medium-speed and high-speed wire-cut EDM machine applications.
Product: DK60BC CNC Medium-Speed Wire EDM Machine (800kg Load, 800mm Thickness)
-
Phone
+86-0523-86268788 +86-13815960366 +86-13912191163Email
[email protected]Address
No. 366, Yusheng Road Jiulong Town, Hailing District Taizhou City, China
Copyright © Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. All Rights Reserved.
Custom edm machine for sale
wholesale edm machine manufacturers
