

 English
 русский
 عربى


Lu Qianwen — Overseas Sales Manager
Home / Author / Lu Qianwen — Overseas Sales Manager / PS50C Heavy-Duty CNC Wire-Cut EDM Machine for Large and Thick Workpieces
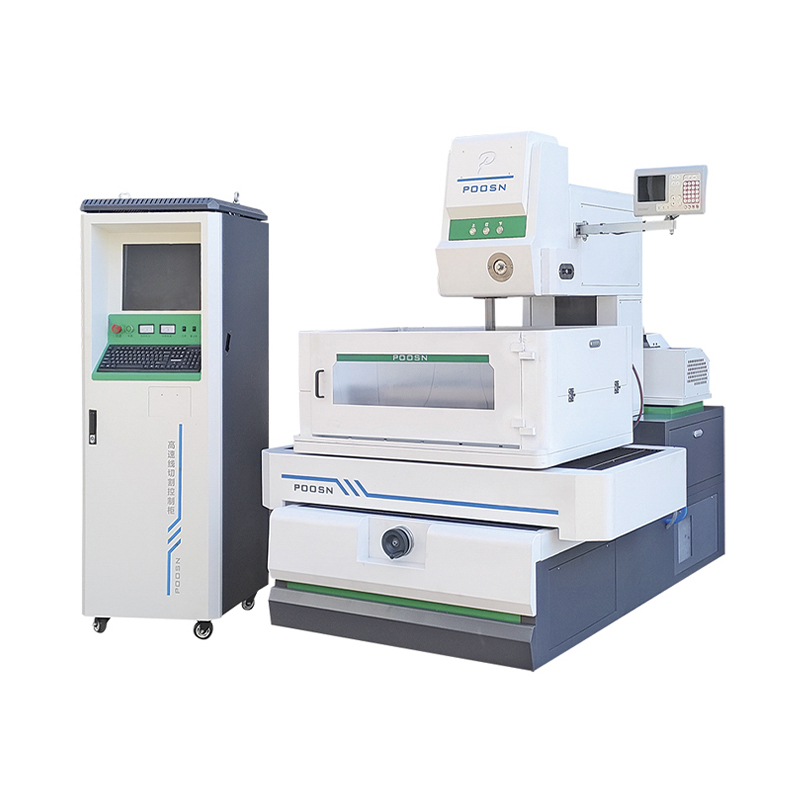
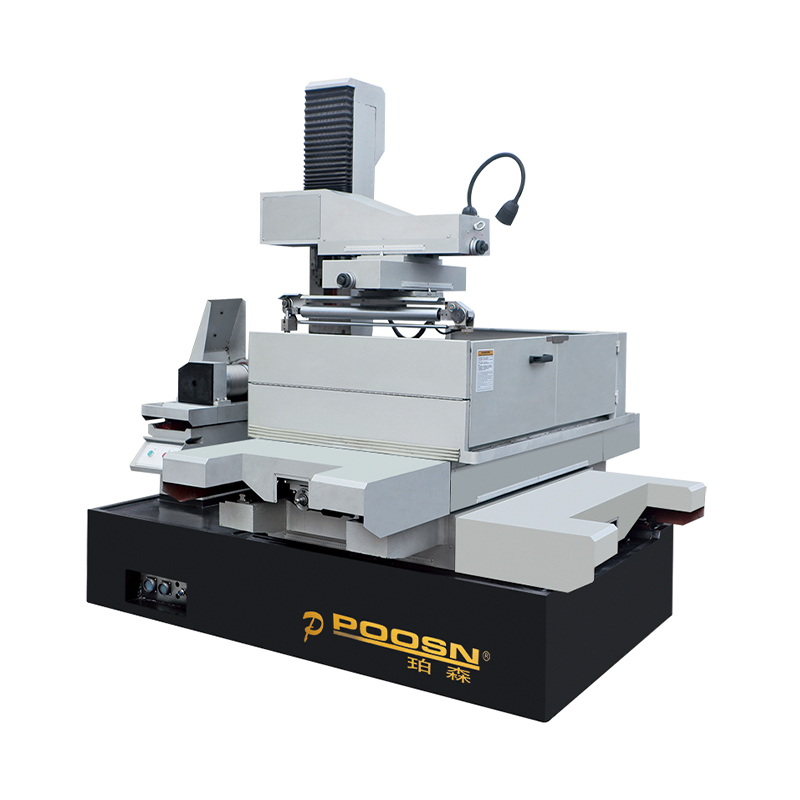
PS50C Heavy-Duty CNC Wire-Cut EDM Machine for Large and Thick Workpieces
2026-08-31
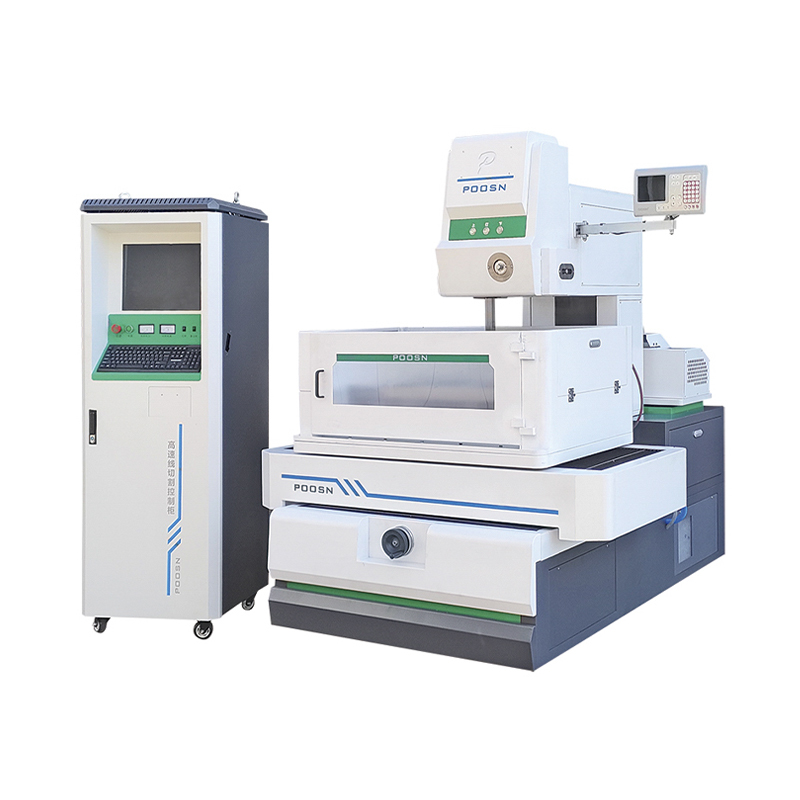
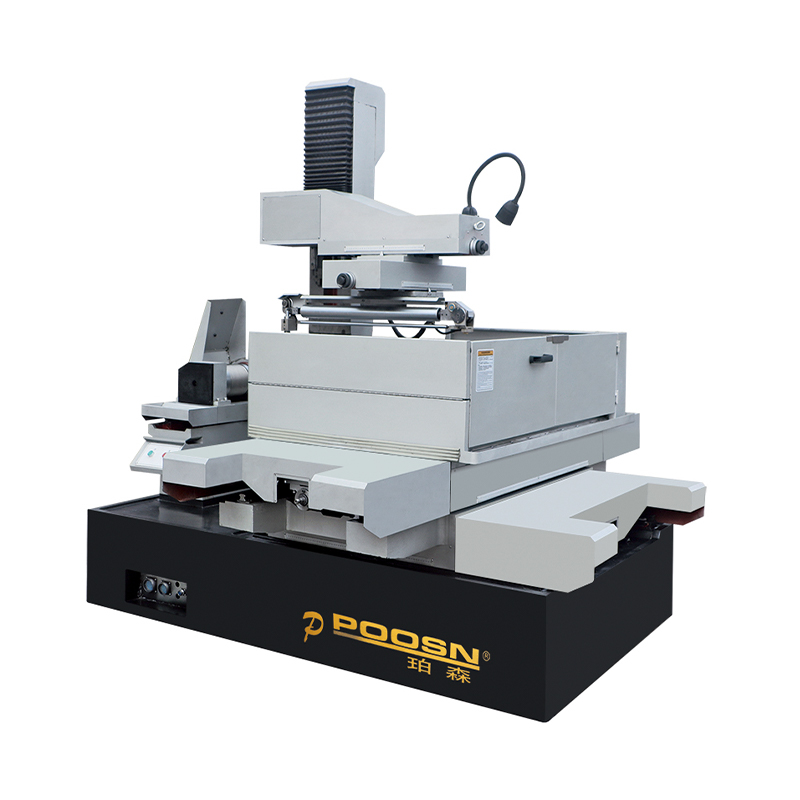
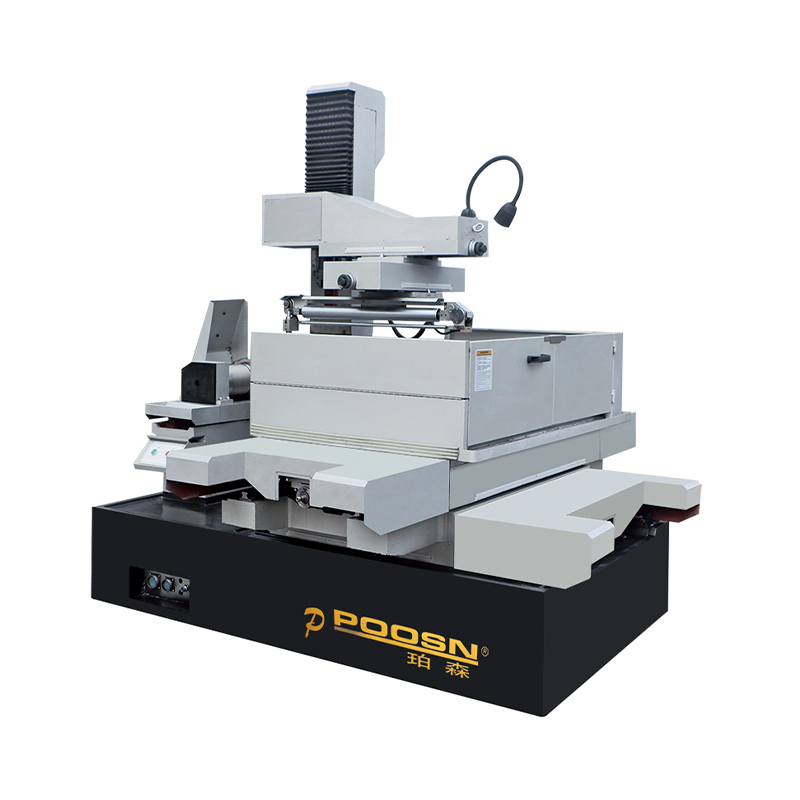
Modern mold manufacturers, aerospace suppliers, precision engineering companies, and heavy-equipment producers increasingly require machining systems that can combine large working capacity, reliable long-cycle operation, accurate contour generation, and manageable operating costs. The PS50C medium-speed wire-cut electrical discharge machining machine is designed for precisely this production environment. It provides a large machining envelope, high load capacity, thick-material cutting capability, four-axis linkage, taper-cutting functions, and a rigid mechanical structure intended for demanding industrial use.
Unlike a basic wire-cut EDM machine developed primarily for small components, the PS50C is configured for large and heavy workpieces. Its 500 by 700 millimeter X-Y travel, 600 kilogram maximum worktable load, and maximum cutting thickness of 350 millimeters allow manufacturers to process molds, dies, structural components, and other complex parts that may exceed the practical capacity of smaller machines. At the same time, the machine retains the essential advantages of medium-speed wire EDM, including economical operation, multi-pass finishing, flexible programming, and high adaptability to conductive materials.
The PS50C is manufactured by Taizhou Xinchengyang Machinery Manufacturing Co., Ltd., a specialist producer with experience in electrical discharge wire cutting since 1999. The company has developed a broad product portfolio covering medium-speed wire-cut EDM, high-speed wire-cut EDM, and large-taper wire-cut EDM equipment. Its manufacturing approach combines mechanical design, electrical discharge technology, control systems, precision assembly, and application support to provide complete machining solutions rather than a machine frame alone.
This article examines the PS50C in detail, explains its principal technologies, compares its advantages with common competing machine categories, and describes how the manufacturer’s production and quality-control practices support stable performance in real industrial applications.
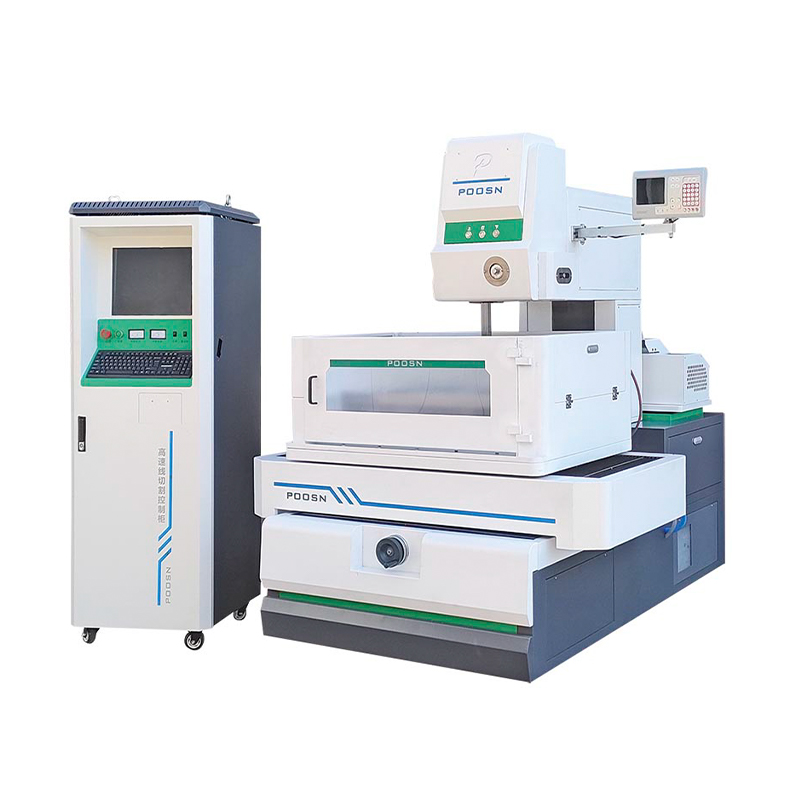
PS50C Heavy-Duty CNC Wire Cut EDM Machine for Large & Thick Workpieces
Content
- 1 1. The Role of Large-Format Medium-Speed Wire EDM
- 2 2. Principal Technical Specifications
- 3 3. Rigid Mechanical Structure for Long-Term Accuracy
- 4 4. Wire Feeding and Tension Control
- 5 5. Pulse Power Supply and Cutting Efficiency
- 6 6. CNC Control and Intelligent Programming
- 7 7. Flushing, Filtration, and Working-Fluid Management
- 8 8. Advantages Compared with Competing Machine Categories
- 9 9. Manufacturing Strengths of the Producer
- 10 10. Applications in High-Value Manufacturing
- 11 11. Customization and Configuration Options
- 12 12. Installation, Operation, and Maintenance Considerations
- 13 13. Production Efficiency and Cost Control
- 14 14. Quality, Sustainability, and Service
- 15 15. Selecting the Appropriate Model
- 16 16. Recommended Evaluation Process for Buyers
- 17 17. Questions and Answers
- 17.1 Q1: Is the PS50C suitable for larger workpieces?
- 17.2 Q2: What is the maximum workpiece weight?
- 17.3 Q3: What is the maximum cutting thickness?
- 17.4 Q4: Can the PS50C cut tapered profiles?
- 17.5 Q5: What surface finish can the PS50C achieve?
- 17.6 Q6: Is the machine suitable for mass production?
- 17.7 Q7: How does the PS50C compare with the PS45C?
- 17.8 Q8: Does the machine require a controlled environment?
- 17.9 Q9: Is automatic wire threading available?
- 17.10 Q10: What type of wire does the PS50C use?
- 17.11 Q11: What control systems are available?
- 17.12 Q12: Can the PS50C be customized?
- 17.13 Q13: What industries use this machine?
- 17.14 Q14: What support does the manufacturer provide?
- 18 18. Conclusion
- 19 References
- 20 Product: PS50C Heavy-Duty CNC Wire Cut EDM Machine for Large & Thick Workpieces
1. The Role of Large-Format Medium-Speed Wire EDM
Wire-cut EDM removes conductive material through controlled electrical discharges between a continuously moving electrode wire and the workpiece. Because the cutting force is effectively negligible, the process is especially useful for hardened steels, tool steels, carbide-related applications, conductive alloys, and complex profiles that would be difficult to produce through conventional milling, sawing, or broaching.
Medium-speed wire EDM occupies an important position between conventional high-speed reciprocating-wire machines and premium low-speed wire EDM systems. It uses a reusable wire-recirculation concept, commonly based on molybdenum wire, while providing CNC control, automatic or assisted wire management, programmable cutting conditions, and multi-cut finishing. This operating concept can offer an attractive balance between acquisition cost, productivity, precision, and consumable expense.
However, not every medium-speed machine is suitable for large components. A machine may offer acceptable precision on small workpieces but lack the structural rigidity, table size, fluid capacity, guide system, or load-bearing performance needed for large and thick parts. Processing a large workpiece also places greater demands on thermal stability, wire tension, flushing, axis synchronization, and long-duration reliability.
The PS50C addresses these challenges through a large T-shaped machine bed, high-strength castings, imported linear guides, ball screws, a regulated wire-feeding system, a high-efficiency pulse power supply, and a working table rated for loads up to 600 kilograms. These features are intended to maintain cutting stability when the machine is operating near the upper end of its work envelope.
1.1 Designed for large and heavy components
The machine’s worktable measures 740 by 1,060 millimeters, while its X-Y travel reaches 500 by 700 millimeters. The processing slot measures approximately 740 by 1,150 millimeters. This configuration offers more practical room for positioning large molds, dies, plates, and mechanical components than compact medium-speed machines.
A maximum worktable load of 600 kilograms further distinguishes the PS50C from entry-level systems. Load capacity is not only a matter of whether a workpiece can physically be placed on the table. It also affects positioning safety, table movement, guideway loading, axis response, and long-term mechanical stability. A machine with a suitable load rating gives users greater flexibility when installing fixtures, clamping devices, support blocks, and heavy workpieces.
1.2 Suitable for thick material cutting
The PS50C has a maximum cutting thickness of 350 millimeters. Thick-section cutting is demanding because the wire must remain adequately supported throughout the cut, dielectric flushing must remove debris from a deep kerf, and discharge conditions must remain stable from the upper surface to the lower surface. Any instability can result in wire vibration, inaccurate geometry, poor surface condition, or wire breakage.
The machine’s wire guide arrangement, tensioning technology, high-pressure water system, and pulse power control are intended to work together during thick-material processing. Actual performance depends on material type, thickness, workpiece geometry, flushing conditions, wire condition, cutting strategy, and selected electrical parameters. Nevertheless, the PS50C provides the physical capacity and control functions required for this class of application.
2. Principal Technical Specifications
The following table summarizes key published specifications for the PS50C and places them alongside related models in the same product family. The comparison demonstrates the progressive increase in worktable size, travel, cutting thickness, and load capacity across the series.
| Specification | PS35C | PS45C | PS50C | PS60C |
| Worktable size | 550 x 826 mm | 650 x 926 mm | 740 x 1060 mm | 840 x 1160 mm |
| X-Y travel | 350 x 500 mm | 450 x 600 mm | 500 x 700 mm | 600 x 800 mm |
| Processing slot size | 545 x 910 mm | 645 x 1010 mm | 740 x 1150 mm | 840 x 1250 mm |
| Maximum cutting thickness | 280 mm | 280 mm | 350 mm | 430 mm |
| Maximum worktable load | 300 kg | 400 kg | 600 kg | 800 kg |
| Maximum cutting taper | Plus or minus 6 degrees per 80 mm | Plus or minus 6 degrees per 80 mm | Plus or minus 6 degrees per 80 mm | Plus or minus 6 degrees per 80 mm |
| Electrode wire diameter | 0.18 mm | 0.18 mm | 0.18 mm | 0.18 mm |
| Wire feed speed | 1 to 11 m/s | 1 to 11 m/s | 1 to 11 m/s | 1 to 11 m/s |
| Maximum cutting efficiency | 10000 to 16000 mm2/h | 10000 to 16000 mm2/h | 10000 to 16000 mm2/h | 10000 to 16000 mm2/h |
| Number of controlled axes | Four-axis linkage | Four-axis linkage | Four-axis linkage | Four-axis linkage |
| Machine weight | 1600 kg | 2000 kg | 2200 kg | 2700 kg |
The PS50C occupies a practical middle position in the family. It offers substantially more capacity than the PS35C and PS45C while remaining smaller and more accessible than the PS60C for facilities that do not require the largest available machine. For manufacturers processing large molds, heavy plates, and medium-to-large production batches, this balance can be more valuable than simply selecting the biggest available model.
3. Rigid Mechanical Structure for Long-Term Accuracy
Machine rigidity is a fundamental factor in wire EDM performance. Although the cutting process does not involve a conventional cutting tool applying mechanical force, the machine still experiences vibration, movement from the wire drive system, hydraulic or fluid-flow effects, thermal variation, and repeated acceleration and deceleration of the axes. These influences become more significant as workpiece size, cutting height, and machining duration increase.
3.1 High-strength resin-sand castings
The PS50C uses high-strength resin-sand castings. This casting method supports the production of dense, stable structural components with controlled geometry. The machine structure is designed to provide sufficient mass and rigidity for large workpieces while helping reduce deformation during long machining cycles.
Proper casting is only the beginning of structural accuracy. The manufacturer also applies aging treatment technology to improve the long-term consistency of the castings. Aging helps relieve internal stresses that may otherwise cause gradual dimensional movement after machining. For a wire EDM machine, this is especially important because even small structural changes can influence guide alignment, axis accuracy, taper geometry, and repeated positioning.
3.2 T-shaped bed design
The PS50C uses a T-shaped bed rather than a conventional narrow or strip-shaped bed. The worktable is supported within the boundaries of the base, which helps limit overhang and reduces the risk of deformation when heavy workpieces are loaded. The design also improves the relationship between the worktable, guideways, and primary machine frame.
This structural concept is particularly relevant for large workpieces. When a heavy component is placed far beyond the effective support area, the table can be more vulnerable to deflection. By keeping the table movement within the base structure, the T-shaped bed helps create a more stable platform for precision cutting.
3.3 Guideways, ball screws, and bearings
High-precision linear guides and ball screws are used for the machine’s motion mechanisms. The taper device also uses linear guides and ball screw pairs, supporting smooth and controlled U and V axis movement. Imported Japanese EZO bearings are applied to the motion mechanisms to support low-friction movement and stable rotational performance.
These components work with pitch-error compensation and servo control to improve positioning accuracy. The stated linear accuracy reaches 0.003 millimeters under the applicable testing conditions, while the test-piece processing accuracy is listed as 0.01 millimeters. As with all machine tools, actual results depend on installation, calibration, environmental stability, workpiece preparation, and process parameters.
The worktable can be equipped with grating scales for real-time, full-stroke position monitoring. Direct position feedback helps the control system detect actual axis movement rather than relying solely on motor rotation. This is advantageous when the machine is processing large travel distances or when high repeatability is required over extended operating periods.
4. Wire Feeding and Tension Control
The electrode wire is the active machining tool in a wire-cut EDM process. Its condition, straightness, tension, speed, and guidance directly influence cutting accuracy, surface finish, productivity, and the likelihood of wire breakage. For this reason, the PS50C places considerable emphasis on the wire-feeding and tension-control system.
4.1 Adaptive constant-tension mechanism
Basic weight-based tensioning systems may respond slowly when tension fluctuates. During high-speed reciprocating motion, changes in wire resistance, direction, acceleration, debris conditions, and cutting height can produce temporary variations in wire tension. If the system does not compensate quickly, the wire may vibrate or deviate from the intended cutting path.
The PS50C can be equipped with an adaptive constant-tension wire-tightening mechanism. This system is designed to respond dynamically to tension changes and reduce variations in electrode-wire force. Maintaining more consistent tension is especially valuable during thick cutting and taper cutting, where the wire has a longer active span and is more sensitive to instability.
Automatic spring wire tension is included as a machine performance feature. An automatic double-sided tightening mechanism helps prevent molybdenum-wire vibration and reduces the possibility of one-sided loosening. By tightening the wire from both sides, the mechanism supports more balanced wire positioning through the machining zone.
4.2 Wire guide wheel design
The machine uses a waterproof gem guide wheel with a 40 millimeter single-sided gemstone guide wheel configuration. The guide wheel is intended to support easy threading, long service life, and high precision. The guide wheel is also designed for convenient replacement, simplifying routine maintenance and reducing downtime.
A liftable gem wire guide is available as a feature of the system. By bringing the wire guide closer to the workpiece surface, the design can reduce wire vibration and improve machining accuracy and surface finish. It also allows the cutting-height range to be adjusted without completely rethreading the wire, making setup and manual operation more efficient.
4.3 Automatic threading and operator safety
One-touch motorized automatic threading reduces the manual effort required to prepare the machine. This is useful when operators must change workpieces frequently, restart after a wire break, or prepare a new job under production pressure. Automatic threading can also reduce the risk of inconsistent manual threading and lower the physical workload associated with repetitive setup tasks.
The machine’s wire drum has a maximum travel of 180 millimeters, while the maximum wire storage length is approximately 320 meters. The standard electrode wire diameter is 0.18 millimeters when used with the appropriate wire guider. Wire feed speed is frequency controlled within a range of approximately 1 to 11 meters per second.
5. Pulse Power Supply and Cutting Efficiency
Electrical discharge performance determines how effectively the machine converts electrical energy into controlled material removal. A suitable pulse power supply must deliver sufficient energy for rough cutting while also allowing finer, lower-energy pulses for finishing operations. It must protect the wire from excessive thermal loading and maintain a stable discharge gap as the cutting conditions change.
The PS50C uses a patented, environmentally conscious pulse power supply designed to provide low electrode wear, high processing speed, low surface roughness, and improved energy efficiency. The full series is equipped as standard with either a high-speed power supply or a nanosecond power supply, depending on the selected configuration.
5.1 Rough cutting and finishing performance
During rough machining, the control system can prioritize material removal and use higher-energy discharge conditions. The objective is to establish the primary contour efficiently while maintaining wire-breakage protection and acceptable geometric control.
During finishing, the system can apply lower-energy pulses and multi-cut strategies. These operations progressively improve surface condition, reduce the recast layer, and refine the final contour. The stated optimal surface roughness is Ra 1.2 micrometers or better under multi-cutting conditions. The final result depends on the material, thickness, number of passes, flushing, wire condition, and selected process parameters.
5.2 Reduced electrode wear
Lower electrode wear provides several practical benefits. It supports more stable wire geometry, helps reduce consumable costs, and can reduce the frequency of wire-related interruptions. The pulse circuit is designed to control the current waveform smoothly, which is particularly important when cutting thick plates or operating at higher current levels.
By balancing discharge energy and wire protection, the machine can support efficient rough cutting without sacrificing the stability required for finishing. This balance is one of the main advantages of a well-developed medium-speed EDM platform compared with a simple machine that relies on limited preset electrical conditions.
5.3 Directional switching and wire-drive life
Imported frequency converters are used to support smooth directional switching in the wire-drive system. Smooth reversal reduces mechanical shock and can help extend the service life of drive components, bearings, guide wheels, and related transmission parts. It also contributes to more consistent wire motion, which can influence surface finish and cutting stability.
6. CNC Control and Intelligent Programming
The PS50C is equipped with an industrial control computer intended for stable operation in a production environment. The standard programming system is identified as X8 or AUTOCUT, while additional software options such as CAXA CAM2019 or TCAM may be selected according to customer requirements.
6.1 Four-axis linkage
The machine provides X, Y, U, and V four-axis linkage. X and Y control the main worktable movement, while U and V control the taper device. Coordinated movement of these axes enables the machine to produce tapered profiles, upper and lower contour differences, and complex geometries that cannot be generated through simple two-axis cutting.
The U and V axis travel is listed as 60 by 60 millimeters for the tapering device. The machine can achieve a maximum cutting taper of plus or minus 6 degrees over 80 millimeters, depending on the workpiece configuration and process conditions. The U and V axes use P-grade linear guides, with optional combinations of servo motors, linear guides, and ball screws available for customers requiring enhanced taper-axis performance.
6.2 Position monitoring and compensation
Real-time position monitoring through grating scales can improve the control system’s awareness of actual axis position across the full stroke. Pitch-error compensation helps correct predictable mechanical deviations, while servo systems can respond to small path errors during complex contouring.
For molds and precision components, these functions are important because the finished part is often evaluated not only by dimensional size but also by geometric form, positional accuracy, corner quality, and the consistency of repeated features. A stable control architecture helps reduce form and position errors associated with mechanical lag and uneven axis response.
6.3 Data exchange and production integration
LAN and USB interfaces support practical data exchange between the machine and the wider production environment. Operators can transfer programs, save machining data, back up process files, and organize job information more efficiently. The intelligent programming system is designed to simplify G-code generation, reducing the time required to move from a CAD drawing or process plan to machine operation.
For production departments running multiple part families, organized program management can improve repeatability. It allows proven cutting parameters and compensation values to be retained and reused, while reducing the possibility of manual transcription errors.
7. Flushing, Filtration, and Working-Fluid Management
Effective flushing is essential in wire EDM. The dielectric fluid must remove eroded particles from the discharge gap, cool the machining zone, and help maintain a stable electrical environment. In thick workpieces, debris removal becomes more difficult because the cutting channel is deeper and the distance between the upper and lower guides is greater.
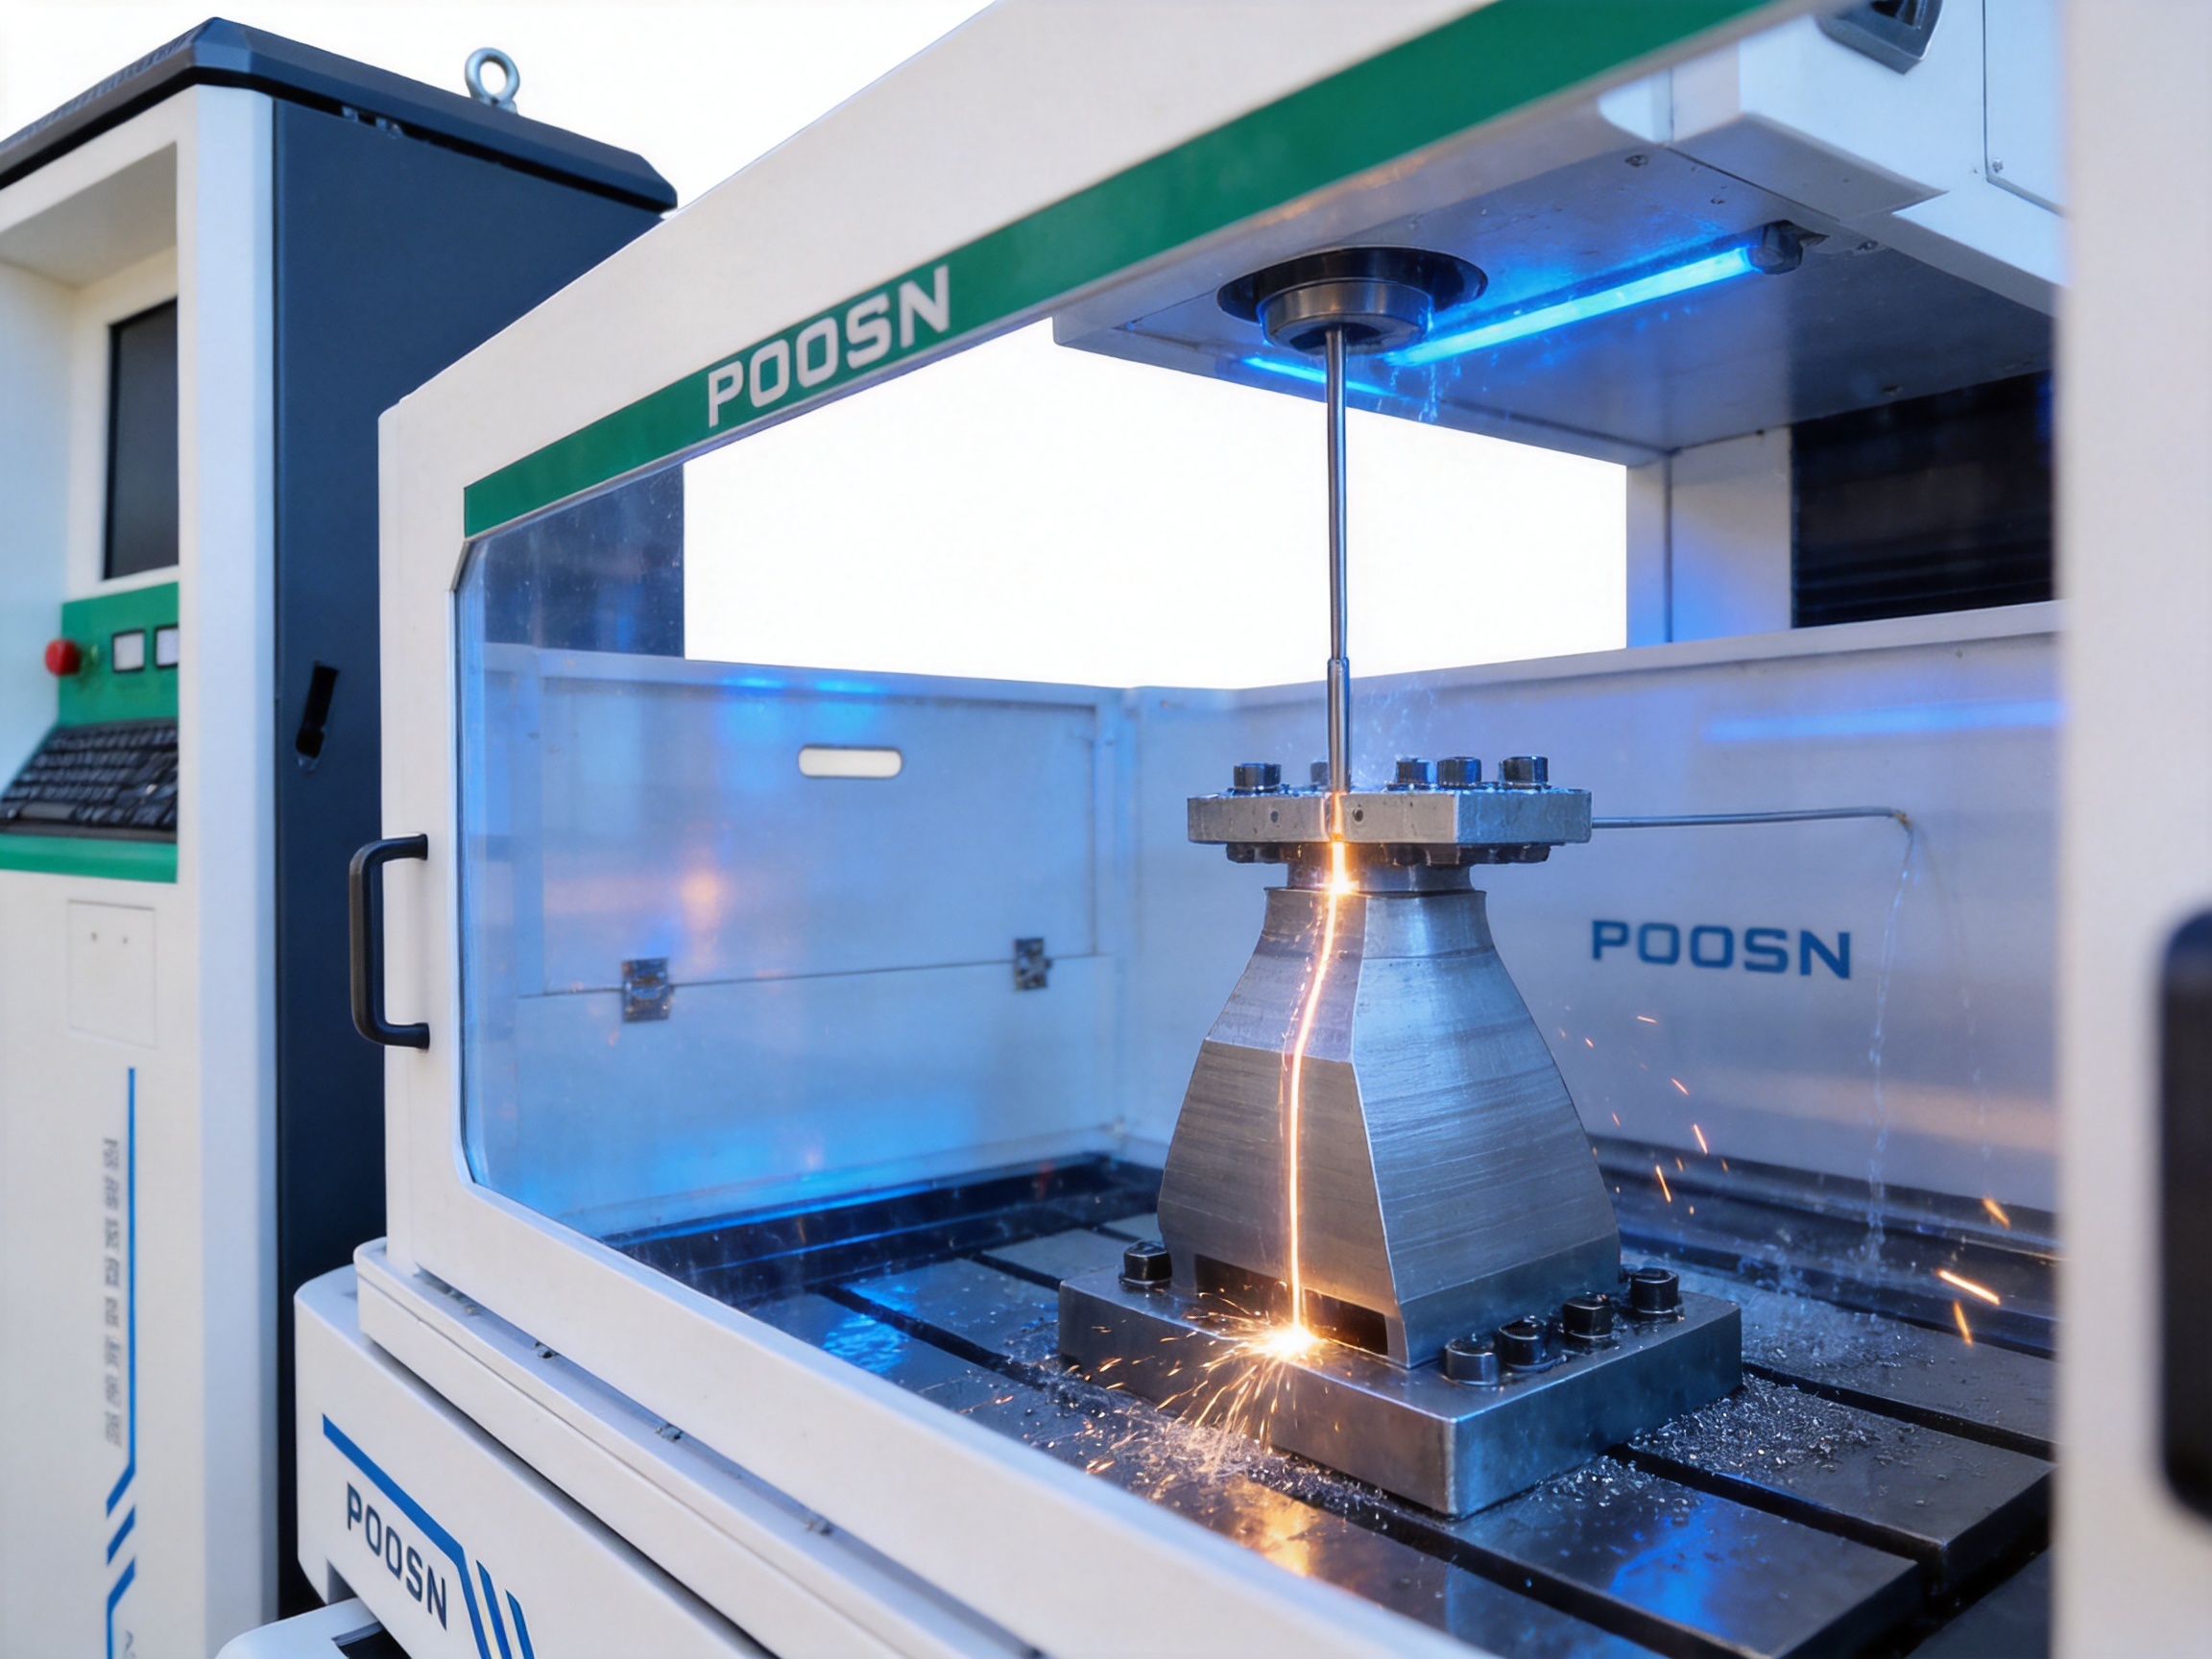
The PS50C includes automatic tracking water spraying during the cutting process. By directing working fluid toward the active machining area, the system supports debris removal and discharge stability. Automatic tracking helps maintain effective flushing as the cutting path changes, reducing the need for constant manual adjustment.
The high-pressure water tank has a capacity of 80 liters and uses paper-core filtration. Filtration helps remove suspended machining particles from the working fluid. Cleaner fluid can contribute to more stable cutting conditions, reduce the risk of secondary discharges, and extend the useful life of pumps, valves, and other fluid-system components.
Fluid management also affects workshop cleanliness. The machine incorporates an anti-splash design intended to reduce working-fluid splatter during operation. A cleaner machining area improves operator comfort, reduces housekeeping requirements, and helps protect nearby electrical and mechanical equipment.
7.1 Process optimization before delivery
The manufacturer reports that simulated machining tests are conducted before equipment delivery. Such testing can help confirm machine operation, validate selected configurations, and shorten the customer’s break-in period. It can also provide an opportunity to review basic process settings before installation at the customer’s facility.
For large and expensive workpieces, process preparation is particularly valuable. A machine may be mechanically capable of cutting a part, but successful production also depends on workholding, flushing direction, wire threading, cutting order, offset management, and finishing strategy. Pre-delivery technical preparation helps reduce the risk of avoidable commissioning delays.
8. Advantages Compared with Competing Machine Categories
The PS50C should be evaluated against the actual needs of a production application rather than against a single general definition of “precision.” Different wire EDM categories are optimized for different combinations of price, speed, surface finish, wire consumption, workpiece size, and automation. Within this context, the PS50C offers several important advantages.
8.1 Compared with compact medium-speed EDM machines
Compact machines are often attractive for small parts, limited floor space, and lower initial investment. However, they may have restricted travel, lower table capacity, smaller fluid systems, and reduced cutting thickness. Attempting to process large workpieces on such equipment can require complicated repositioning or may simply be impossible.
The PS50C provides a larger worktable, 500 by 700 millimeter X-Y travel, 350 millimeter cutting thickness, and 600 kilogram load capacity. This allows users to keep large components in a single setup more often, reducing the need for repositioning and the associated risk of accumulated alignment errors.
8.2 Compared with basic high-speed wire EDM machines
High-speed wire EDM machines can be cost-effective for general-purpose cutting, but some basic models may offer fewer advanced position-feedback functions, less refined tension control, or limited taper-axis performance. The PS50C combines medium-speed operation with grating-scale monitoring, four-axis linkage, optional constant tension, linear-guide taper mechanisms, and multi-cut control.
These features are beneficial when the application requires not only fast rough cutting but also repeatable finishing and complex profiles. The machine’s structure and control system are intended to bridge the gap between basic high-speed wire cutting and more specialized precision equipment.
Premium low-speed wire EDM machines can provide excellent accuracy, surface finish, and automated wire management, but their purchase price, wire consumption, service requirements, and operating costs may be significantly higher. For companies that need large-format processing and reliable precision but must also maintain a controlled investment and manageable consumable budget, a medium-speed platform can be a more practical choice.
The PS50C uses a reusable-wire concept, a high-efficiency pulse power supply, multi-cut capability, and a robust machine structure. This combination is intended to deliver a favorable balance between productivity and running cost. It may be especially suitable for manufacturers that require many cutting hours per day but do not need the complete automation architecture associated with the most expensive low-speed systems.
8.4 Compared with conventional mechanical cutting
Milling, sawing, and broaching can be highly productive for suitable shapes, but they apply mechanical forces and require cutting tools that wear against the workpiece. Hardened materials and intricate internal profiles may require multiple operations, specialized tooling, or extensive setup work.
Wire EDM cuts without direct mechanical contact. It can process hardened conductive materials after heat treatment and produce narrow kerfs, intricate contours, sharp internal corners, and complex openings. For large precision molds and difficult-to-machine components, these advantages can simplify the process route and reduce the need for secondary operations.
9. Manufacturing Strengths of the Producer
The performance of a machine tool is closely connected to the capabilities of the manufacturer. A product specification may list travel, load, and accuracy, but long-term customer value also depends on casting quality, assembly discipline, component selection, calibration, software development, process testing, and after-sales support.
9.1 Long-term specialization
Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. has specialized in electrical discharge wire cutting since 1999. Its POOSN brand originated in 2003, and the company has continued to develop medium-speed, high-speed, and large-taper machine series. Long-term specialization allows engineering teams to accumulate application knowledge related to wire tension, pulse discharge, flushing, taper cutting, machine rigidity, and operator requirements.
The company established its current manufacturing entity in 2017 with registered capital of 60 million yuan and built its own factory. It obtained a patent in 2018 for a fully automatic CNC machine tool featuring plate-type winding and suction-type adhesive technology. In 2021, it was recognized as a high-tech enterprise in Taizhou.
9.2 Integrated technical capabilities
The producer describes its capabilities as covering research and development, production, testing, and special processing technologies. This integrated structure is important because wire EDM performance depends on the coordination of several disciplines. Mechanical accuracy alone cannot compensate for unstable discharge control, and a sophisticated control system cannot fully overcome a poorly aligned machine frame.
For the PS50C, the relevant areas include resin-sand casting, aging treatment, precision machining, imported guideway and bearing integration, AC servo control, power-supply development, wire-drive design, filtration, taper mechanisms, and software configuration. Managing these elements as one product system can improve compatibility and reduce the uncertainty that may arise when components are selected without an integrated design philosophy.
9.3 Testing and positioning accuracy verification
The company states that each machine tool undergoes positioning accuracy testing. Such testing is essential for confirming axis response, repeatability, travel behavior, and the relationship between commanded and measured positions. It also provides a basis for final calibration and acceptance documentation.
In addition to positioning tests, simulated machining before shipment can help verify the interaction between mechanical movement, electrical discharge, wire transport, and fluid circulation. This type of testing is particularly useful for a large machine because transport, installation, leveling, and commissioning must preserve the alignment achieved during manufacturing.
9.4 Component standardization
Standardized component management can simplify maintenance and spare-parts planning. The company emphasizes the use of selected imported components, including linear guides, bearings, and servo-related elements, together with its own structural and electrical technologies. Standardized maintenance access, centralized lubrication, and replaceable guide-wheel components can help lower the technical barrier for service personnel.
For production users, the value of standardization appears over the entire service life of the machine. Easier parts identification, more predictable maintenance procedures, and responsive technical support can reduce downtime and improve the total cost of ownership.
10. Applications in High-Value Manufacturing
10.1 Large molds and dies
The PS50C is well suited to large injection molds, stamping dies, extrusion-related tooling, and other mold components requiring internal profiles, narrow slots, angled surfaces, or hardened-material processing. A large table and high load rating allow heavy mold plates to be mounted with appropriate support and clamping equipment.
Multi-pass cutting can be used to improve surface quality and contour precision. Taper capability supports mold features that require draft angles or different upper and lower contours. The machine can also help mold manufacturers reduce dependence on specialized mechanical cutters when producing narrow or complex openings.
10.2 Aerospace components
Aerospace manufacturing places strict demands on dimensional control, material traceability, surface integrity, and process repeatability. Conductive alloys and hardened materials may contain complex geometries that are difficult to machine with conventional tools. Wire EDM can provide a controlled, low-force method for producing profiles, slots, and precision openings.
The PS50C’s large work envelope is useful for fixtures and components that cannot be accommodated by compact equipment. Its stable wire tension, position monitoring, and multi-axis control support the production of demanding shapes. Aerospace users must still validate the process for each material and part specification, but the machine provides a strong platform for development and production work.
10.3 Heavy machinery and mechanical components
Heavy machinery manufacturers often process thick plates, large wear-resistant components, and structural parts with high material hardness. The PS50C’s 350 millimeter maximum cutting thickness and 600 kilogram table load make it appropriate for many such applications.
The non-contact cutting process reduces the risk of mechanical distortion associated with high cutting forces. This can be advantageous for parts that are difficult to clamp rigidly or whose geometry could be affected by conventional tool pressure. Careful support and fluid management remain essential, especially when processing tall workpieces.
10.4 Precision machinery and general industrial production
Precision machinery suppliers can use the PS50C for guide components, custom fixtures, mechanical plates, special gears, forming elements, and replacement parts. The machine is suitable for prototype work as well as small, medium, and larger batch production, provided that the workpiece size and material fall within the process requirements.
The machine’s cutting efficiency is specified at approximately 10000 to 16000 square millimeters per hour. Actual productivity varies according to material thickness, material composition, geometry, flushing, surface-finish targets, and the selected control-cabinet configuration. Even so, the range indicates that the PS50C is intended for more than occasional toolroom use; it is designed to support regular production.
11. Customization and Configuration Options
Large industrial components do not always conform to standard machine dimensions. The manufacturer therefore offers customization services for worktable dimensions, extended cutting depth, power configuration, and machining processes. Customized engineering can be valuable when the customer has a specialized production requirement that cannot be satisfied by a standard model.
11.1 Mechanical customization
Mechanical customization may include larger or modified worktable dimensions, increased cutting depth, special workholding provisions, or adjustments to suit a customer’s loading method. Each change must be evaluated in relation to machine rigidity, axis travel, flushing, safety, transport, and installation requirements.
11.2 Control and power options
The PS50C can be configured with different control-cabinet options. The control system, power supply, servo configuration, and software package influence cutting efficiency, surface finish, programming convenience, and automation compatibility. Customers should select these options according to part geometry, production volume, operator skill, and desired process capability rather than choosing solely on initial price.
11.3 Taper and lifting options
The taper device is equipped with linear guides and ball screw pairs as standard in the relevant series configuration. Optional U and V axis combinations, servo motors, and additional linear-guide or ball-screw configurations can be considered when the application places high demands on taper accuracy or dynamic response.
Linear-guide lifting is also available as an option. This can improve access to the workpiece surface and make wire-guide adjustment more convenient. Customers should discuss required cutting heights, taper angles, workpiece geometry, and threading procedures with the technical team before finalizing the machine configuration.
12. Installation, Operation, and Maintenance Considerations
Even a well-designed machine requires correct installation and disciplined operation. The PS50C should be placed in an environment with limited temperature fluctuation, controlled dust, adequate floor strength, and sufficient service clearance. Stable environmental conditions help protect geometric accuracy and reduce the effect of thermal expansion on long cutting cycles.
12.1 Workshop preparation
The installation area should provide the required electrical supply, water management, drainage or fluid-handling provisions, lifting access, and safe operator clearance. The listed power supply is 3N 380 volts with a tolerance of plus or minus 10 percent, while the electrical capacity is listed as 2.5 kVA for the specified configuration. Customers should confirm the final electrical requirements from the machine order documents because optional cabinets and accessories may change installation conditions.
The machine weight is approximately 2,200 kilograms for the PS50C. Foundations and floor loading must therefore be evaluated before delivery. Adequate space should also be reserved around the machine for filter replacement, guide-wheel maintenance, wire threading, electrical access, and workpiece loading.
12.2 Routine maintenance
Routine maintenance should include checking wire condition, guide-wheel wear, tension behavior, water pressure, filter condition, working-fluid cleanliness, lubrication, axis movement, and electrical connections. A centralized lubrication system for critical components such as guide rails and lead screws can simplify scheduled service.
Filters should be replaced at suitable intervals based on cutting hours and contamination levels. Dirty working fluid can reduce flushing efficiency and influence discharge stability. Operators should also inspect the wire guides and guide wheels for wear because worn guidance can affect kerf position, surface finish, and taper accuracy.
12.3 Operator training
The PS50C uses an interface designed to simplify programming and operation. A process database can help operators select initial cutting conditions for common materials and thicknesses. Nevertheless, proper training remains important. Operators should understand workpiece conductivity, threading, flushing, wire tension, offsets, compensation, multi-cut planning, wire-break recovery, and safe handling of working fluid.
Experienced operators can improve productivity by selecting the right cutting sequence. For example, a large internal opening may require consideration of entry-hole location, slug support, stress relief, flushing direction, and the order of rough and finish passes. These decisions are part of the complete machining solution and are not determined by machine hardware alone.
13. Production Efficiency and Cost Control
Production efficiency is influenced by more than maximum cutting speed. A machine must also minimize setup time, reduce wire breakage, maintain consistent quality, support repeatable programming, and remain available over long operating periods. The PS50C addresses these factors through automatic threading, constant-tension options, position monitoring, efficient pulse control, stable wire transport, and a large working capacity.
Large workpieces can often be processed in a single setup, reducing handling and alignment time. A higher table load rating allows robust fixtures and support systems to be used without approaching the machine’s mechanical limits. The ability to cut thick materials also reduces the need to divide a component into multiple operations.
Medium-speed EDM can provide lower consumable costs than many low-speed wire systems because the electrode wire is recirculated. The PS50C’s pulse-power design is intended to limit wire wear while maintaining cutting speed. Reduced wire consumption, stable multi-pass performance, and standardized spare parts can all contribute to lower operating costs.
The machine is also designed for long-duration operation, including production environments that operate continuously for extended shifts. Its high-strength structure, imported motion components, stable wire system, and fluid-management features support reliable operation. Continuous operation should always be managed according to the manufacturer’s maintenance schedule, environmental requirements, and safety instructions.
14. Quality, Sustainability, and Service
The manufacturer presents the PS50C as a machine developed not only for technical performance but also for practical sustainability. A low-energy standby mode and an efficient discharge circuit can reduce unnecessary electrical consumption. Improved filtration and fluid circulation can extend consumable service life and help maintain cleaner working conditions.
Green machining is increasingly connected with measurable production efficiency. Lower energy use, reduced wire waste, longer component life, fewer rejected parts, and less rework all contribute to a more sustainable manufacturing process. For a large machine operating many hours per day, even modest efficiency gains can accumulate into meaningful savings.
Service support is another important part of machine value. The producer provides rapid-response technical assistance, installation guidance, remote support, spare-parts supply, and process-related assistance. These services help customers maintain operational stability after installation and resolve issues before they become prolonged production interruptions.
A long-term support relationship is especially important for companies adopting large-format wire EDM for the first time. Correct leveling, parameter selection, filter management, wire installation, and process validation can significantly influence the results achieved during the first months of operation.
15. Selecting the Appropriate Model
The PS50C is part of a broader product family, so model selection should be based on workpiece size, weight, thickness, production volume, and required process flexibility.
15.1 PS35C
The PS35C is intended for smaller components and small-to-medium batch production. It is appropriate where compact dimensions, precision, and efficient processing are more important than maximum load capacity or large travel.
15.2 PS45C
The PS45C offers more table space and load capacity than the PS35C. It is suitable for medium-sized parts, larger molds, and precision components that require more working room but do not justify the full capacity of the PS50C.
15.3 PS50C
The PS50C is designed for large and heavy workpieces. Its 500 by 700 millimeter X-Y travel, 350 millimeter maximum cutting thickness, and 600 kilogram maximum table load make it an appropriate choice for demanding applications involving large molds, thick plates, aerospace-related components, and heavy mechanical parts.
15.4 PS60C
The PS60C is designed for extra-large workpieces and high-load components. With 600 by 800 millimeter X-Y travel, a maximum cutting thickness of 430 millimeters, and an 800 kilogram table load, it is better suited to applications that exceed the practical capacity of the PS50C.
When comparing models, users should consider future production requirements rather than only their current largest part. A machine with a modest capacity margin may become restrictive if product dimensions or fixture weight increase. At the same time, selecting a machine that is substantially larger than necessary may increase installation, floor-space, and operating costs. The PS50C is often a balanced selection for companies positioned between general-purpose and extra-large machining requirements.
16. Recommended Evaluation Process for Buyers
Before purchasing, buyers should prepare representative workpiece drawings, material information, thickness ranges, weight data, required tolerances, surface-finish targets, taper requirements, and expected monthly cutting hours. These details allow the manufacturer to recommend the correct control cabinet, power supply, servo options, worktable configuration, and software.
A cutting trial using customer material is highly recommended for critical applications. The trial can evaluate cutting speed, wire consumption, surface finish, corner quality, taper behavior, dimensional accuracy, and multi-pass repeatability. It can also reveal whether special flushing or fixturing arrangements are required.
Buyers should also request information about installation conditions, service intervals, spare-parts availability, training, warranty coverage, acceptance testing, and response procedures. These factors influence the machine’s total value as much as the initial specification sheet.
The PS50C is particularly attractive when the buyer values a combination of large capacity, medium-speed operating economy, multi-cut precision, thick-material capability, and customization support. It is not intended to replace every type of EDM machine, but it provides a strong solution for the specific production segment between compact wire cutting and premium automated low-speed systems.
17. Questions and Answers
Q1: Is the PS50C suitable for larger workpieces?
Yes. The machine provides an X-axis travel of 500 millimeters and a Y-axis travel of 700 millimeters. Its 740 by 1,060 millimeter worktable provides additional space for fixtures and large components. The machine is designed for applications requiring a broad processing range and increased load capacity.
Q2: What is the maximum workpiece weight?
The maximum listed worktable load is 600 kilograms for the PS50C. The actual safe loading arrangement must also consider the distribution of weight, fixture design, support points, and workpiece dimensions. Heavy components should be installed according to the manufacturer’s loading and safety instructions.
Q3: What is the maximum cutting thickness?
The PS50C has a maximum cutting thickness of 350 millimeters. Practical cutting performance depends on the material, workpiece shape, flushing conditions, wire status, cutting parameters, and required surface finish.
Q4: Can the PS50C cut tapered profiles?
Yes. The machine uses four-axis linkage through X, Y, U, and V axes. Its maximum listed cutting taper is plus or minus 6 degrees over 80 millimeters. Optional taper-axis configurations can be considered for applications requiring enhanced performance.
Q5: What surface finish can the PS50C achieve?
The stated optimal surface roughness is Ra 1.2 micrometers or better under multi-cutting conditions. The result depends on material, thickness, cutting strategy, number of finishing passes, wire condition, flushing, and electrical settings.
Q6: Is the machine suitable for mass production?
Yes. The PS50C is intended for medium-to-large production requirements. Its maximum listed cutting efficiency is approximately 10000 to 16000 square millimeters per hour. Automatic threading, stable wire tension, position monitoring, and long-cycle structural stability can help support production use.
Q7: How does the PS50C compare with the PS45C?
The PS50C provides a larger worktable, greater X-Y travel, a higher load rating, and increased maximum cutting thickness. It is better suited to large, heavy, or complex workpieces. The PS45C remains a suitable choice for medium-sized components where the additional capacity of the PS50C is not required.
Q8: Does the machine require a controlled environment?
The PS50C has strong environmental adaptability, but a workshop with limited temperature fluctuation, controlled dust, stable power, and proper floor support is recommended. Environmental control helps maintain dimensional stability and consistent cutting results.
Q9: Is automatic wire threading available?
Yes. One-touch motorized automatic threading is included as a machine feature. It reduces manual labor, improves setup convenience, and can make wire-break recovery more efficient.
Q10: What type of wire does the PS50C use?
The listed electrode wire diameter is 0.18 millimeters when used with the specified wire guider. The machine is configured for medium-speed wire cutting with a reusable wire-feeding system. Users should confirm compatible wire specifications with the manufacturer before selecting consumables.
Q11: What control systems are available?
The standard programming system is X8 or AUTOCUT. CAXA CAM2019 or TCAM can be selected as optional software according to application needs. The machine also includes LAN and USB interfaces for practical program and data exchange.
Q12: Can the PS50C be customized?
Customization is available for worktable dimensions, extended cutting depth, power configuration, selected control systems, and machining processes. Technical feasibility should be confirmed before ordering because custom changes can affect structure, fluid management, electrical capacity, transport, and installation.
Q13: What industries use this machine?
Typical applications include large mold manufacturing, precision dies, aerospace components, heavy machinery, precision machinery, industrial equipment, and thick conductive metal components. The suitability of the machine should be verified through a process trial when material or tolerance requirements are especially demanding.
Q14: What support does the manufacturer provide?
The manufacturer provides installation guidance, technical consultation, remote support, spare-parts assistance, and process-related service. Pre-delivery simulated machining tests may also be conducted to help shorten commissioning time.
18. Conclusion
The PS50C heavy-duty CNC wire-cut EDM machine is designed for manufacturers that need more than basic wire cutting. Its large work envelope, 600 kilogram worktable load, 350 millimeter cutting thickness, four-axis taper capability, constant-tension options, high-efficiency pulse power supply, and rigid T-shaped bed create a platform for large and thick workpieces.
Its principal competitive advantage is the balance it provides. Compared with compact medium-speed machines, it offers substantially greater capacity. Compared with basic high-speed machines, it adds more advanced position monitoring, tension control, taper guidance, and finishing capability. Compared with premium low-speed systems, it can offer a more economical medium-speed operating concept while retaining the precision functions required for demanding industrial work.
The machine’s value is reinforced by the manufacturing strengths of Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. The company’s long specialization in wire EDM, integrated technical capabilities, structural casting and aging processes, precision component selection, positioning accuracy testing, simulated machining, customization services, and after-sales support form an important part of the complete solution.
For companies producing large molds, thick plates, aerospace-related components, heavy mechanical parts, and precision industrial equipment, the PS50C offers a capable and adaptable route to higher production efficiency, stable dimensional performance, and controlled operating costs. Proper application evaluation, installation, training, and maintenance will allow the machine to deliver its full potential over a long service life.
References
1. Taizhou Xinchengyang Machinery Manufacturing Co., Ltd., PS-C Series Medium-Speed Wire-Cut EDM Machine Technical Specifications.
2. Taizhou Xinchengyang Machinery Manufacturing Co., Ltd., PS50C Product Information and Application Data.
3. International Organization for Standardization, ISO 230 Series, Test Code for Machine Tools.
4. International Organization for Standardization, ISO 14001, Environmental Management Systems.
5. International Electrotechnical Commission, Standards and Technical Guidance for Electrical Equipment Safety.
6. General technical literature on electrical discharge machining, wire electrode control, dielectric flushing, and multi-pass finishing.
7. General manufacturing engineering references concerning CNC positioning accuracy, machine-tool rigidity, guideway systems, and thermal stability.
Product: PS50C Heavy-Duty CNC Wire Cut EDM Machine for Large & Thick Workpieces
-
Phone
+86-0523-86268788 +86-13815960366 +86-13912191163Email
[email protected]Address
No. 366, Yusheng Road Jiulong Town, Hailing District Taizhou City, China
Copyright © Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. All Rights Reserved.
Custom edm machine for sale
wholesale edm machine manufacturers
