

 English
 русский
 عربى


Zhou Meiling — Technical Sales Consultant
Home / Author / Zhou Meiling — Technical Sales Consultant / DK-7745 CNC High-Speed Wire EDM Machine: Large-Format Precision, Four-Axis Flexibility, and Efficient Production
DK-7745 CNC High-Speed Wire EDM Machine: Large-Format Precision, Four-Axis Flexibility, and Efficient Production
2026-09-04
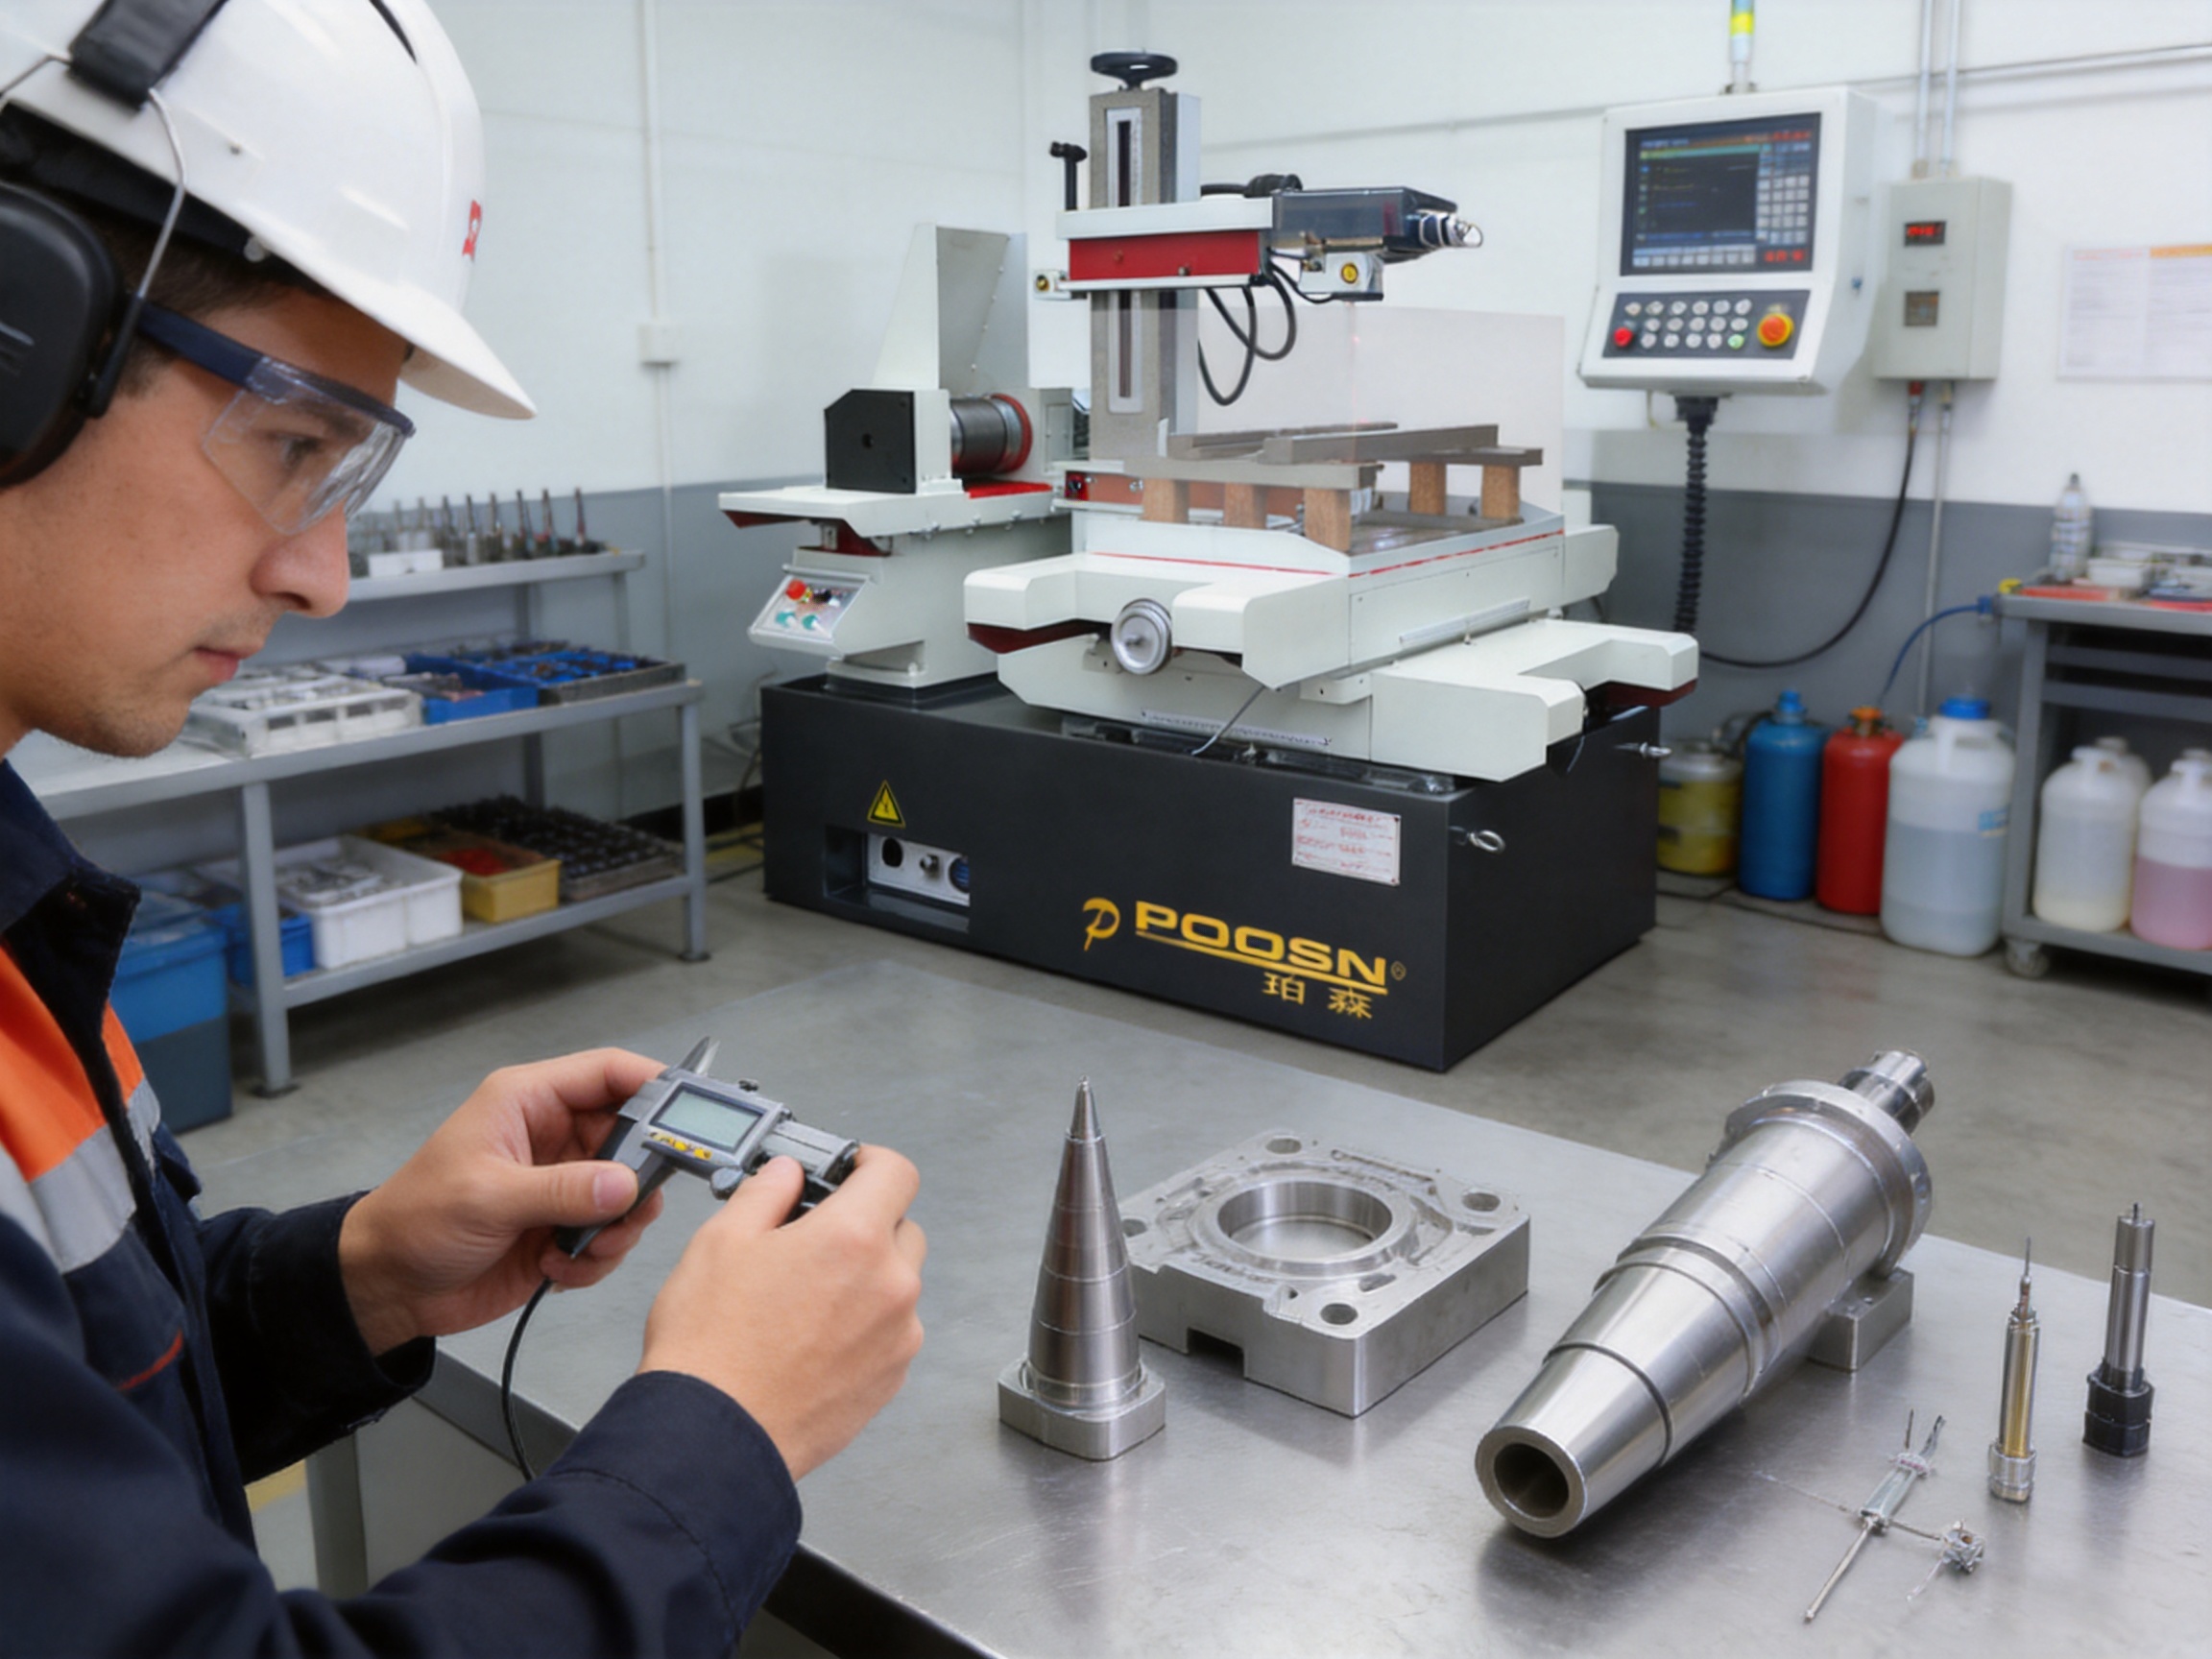
Modern mold manufacturers, precision component suppliers, aerospace subcontractors, automotive part producers, and electronic equipment companies increasingly require machining equipment that can combine large workpiece capacity with accurate contour cutting. Conventional milling can be limited when the workpiece is extremely hard, when a narrow slot or intricate profile is required, or when the required geometry contains sharp internal corners and narrow gaps. The DK-7745 CNC High-Speed Wire Electrical Discharge Machining machine is designed for these demanding conditions.
Positioned within the DK-77 high-speed wire-cut EDM range, the DK-7745 is a four-axis CNC machine developed for complex shapes, high-precision components, large molds, and production environments where dependable cutting performance is essential. Its design combines a rigid machine structure, high-speed reciprocating wire movement, four-axis linkage, a high-efficiency pulse power system, and a user-oriented CNC control cabinet. Together, these features provide a practical balance between machining speed, accuracy, workpiece capacity, operating cost, and long-term stability.
The machine is especially suitable for manufacturers that need more than a basic wire-cutting solution. It is intended to support repeatable production, large workpiece handling, taper cutting, complex contour interpolation, and the processing of conductive materials that are difficult or uneconomical to machine using conventional cutting methods.
Content
- 1 1. Product Positioning and Core Value
- 2 2. Main Technical Specifications
- 3 3. Four-Axis Machining for Complex Geometries
- 4 4. High-Speed Reciprocating Wire System
- 5 5. Structural Rigidity and Long-Term Stability
- 6 6. Electrical Discharge and Pulse Power Performance
- 7 7. Accuracy, Surface Finish, and Process Control
- 8 8. Workpiece Capacity and Heavy-Duty Machining
- 9 9. Competitive Advantages in the High-Speed WEDM Market
- 10 10. CNC Control and Operator Usability
- 11 11. Manufacturing Processes and Quality Assurance
- 12 12. Application Areas
- 13 13. Production Efficiency and Total Cost Considerations
- 14 14. Customization and Technical Support
- 15 15. Installation, Operation, and Maintenance Recommendations
- 16 16. Model Selection Within the DK-77 Range
- 17 17. Recommended Purchasing and Acceptance Checklist
- 18 18. Frequently Asked Questions
- 18.1 Q1: What is the maximum worktable load of the DK-7745?
- 18.2 Q2: What are the main accuracy specifications?
- 18.3 Q3: What is the maximum cutting thickness?
- 18.4 Q4: What is the maximum cutting efficiency?
- 18.5 Q5: Can the DK-7745 cut tapered profiles?
- 18.6 Q6: Which materials can be processed?
- 18.7 Q7: Is high-speed wire EDM less expensive to operate than low-speed wire EDM?
- 18.8 Q8: Is the DK-7745 suitable for mass production?
- 18.9 Q9: Is the CNC system difficult for new operators?
- 18.10 Q10: What control cabinets are available?
- 18.11 Q11: How does the machine maintain long-term stability?
- 18.12 Q12: Does the manufacturer provide customization?
- 19 19. Conclusion
- 20 References
- 21 Product: DK-7745 CNC High-Speed Wire EDM Machine (4-Axis, 400×600mm Travel)
1. Product Positioning and Core Value
The DK-7745 addresses a common manufacturing challenge: how to process large and complex conductive workpieces efficiently without sacrificing dimensional accuracy or surface quality. A machine with a small travel range may deliver good precision but require multiple setups for a large mold. A machine designed only for heavy cutting may lack the control resolution or structural stability needed for fine contours. The DK-7745 is engineered to occupy the middle and upper range of high-speed wire-cut EDM applications, offering substantial travel, a strong worktable, and high-speed electrical discharge cutting in a single platform.
Its four-axis configuration uses X, Y, U, and V axes, allowing the upper and lower wire guides to move in a coordinated manner. This four-axis linkage supports taper machining and enables the creation of profiles that are not limited to simple vertical cuts. As a result, the machine can process inclined surfaces, tapered mold features, and complex two-dimensional contours with greater flexibility than a basic two-axis wire-cut system.
The published product title identifies the DK-7745 as a machine with approximately 400 × 600 mm travel. The detailed model table for the DK-7745 family lists a 570 × 850 mm worktable and 450 × 550 mm X/Y travel. Because configurations may vary by production batch, control cabinet, and customer requirements, buyers should confirm the final travel specification, table configuration, and supplied accessories before placing an order. This clarification does not change the machine’s principal positioning: it is a large-workpiece, four-axis, high-speed WEDM platform for demanding precision applications.
In its standard configuration, the DK-7745 is specified with a maximum worktable load of 400 kg, a maximum cutting thickness of 450 mm, a maximum cutting taper of ±6° per 80 mm, and a cutting efficiency of approximately 10,000 to 16,000 mm² per hour depending on the CNC cabinet, material, thickness, wire, flushing conditions, and process parameters.
2. Main Technical Specifications
The following table summarizes the main specifications supplied for the DK-7745 and its related models. The broader model comparison is useful because it shows how the DK-7745 fits into the manufacturer’s high-speed wire EDM platform.
| Specification | DK-7725 | DK-7735 | DK-7745 | DK-7745F |
| Worktable Size | 410 × 600 mm | 500 × 750 mm | 570 × 850 mm | 570 × 950 mm |
| X/Y Travel Size | 250 × 320 mm | 350 × 450 mm | 450 × 550 mm | 450 × 650 mm |
| Maximum Cutting Thickness | 350 mm | 450 mm | 450 mm | 450 mm |
| Maximum Cutting Taper | ±6°/80 mm | ±6°/80 mm | ±6°/80 mm | ±6°/80 mm |
| Maximum Cutting Efficiency | 10,000–16,000 mm²/h | 10,000–16,000 mm²/h | 10,000–16,000 mm²/h | 10,000–16,000 mm²/h |
| Optimal Surface Roughness | Ra ≤ 2.5 μm | Ra ≤ 2.5 μm | Ra ≤ 2.5 μm | Ra ≤ 2.5 μm |
| Drive Type | X, Y, U, and V stepper drive; four-axis linkage | |||
| Standard Control Cabinet | ZH-K68 desktop cabinet | |||
| Optional Control Cabinet | ZHZK-03 vertical cabinet | |||
| Power Supply | 3N 380 V ±10% | |||
| Maximum Worktable Load | 250 kg | 300 kg | 400 kg | 500 kg |
| Machine Weight | 800 kg | 1,100 kg | 1,250 kg | 1,350 kg |
The DK-7745’s 400 kg worktable capacity is important for manufacturers processing large dies, thick plates, hardened steel components, and heavy conductive workpieces. Adequate loading capacity helps reduce the need to divide a component into smaller sections or use additional support fixtures. It also contributes to more stable workholding, provided that the workpiece is correctly supported and the total load is distributed according to the machine’s operating instructions.
The machine’s 450 mm maximum cutting thickness gives it a practical advantage over compact wire EDM equipment when the application involves thick mold plates, large stamping die sections, structural components, or tall workpieces. Actual results depend on material type, flushing, wire tension, power settings, and workpiece geometry, but the rated thickness establishes the machine as a serious solution for heavy and high-precision work.
3. Four-Axis Machining for Complex Geometries
A primary advantage of the DK-7745 over a conventional two-axis wire-cut machine is its four-axis interpolation capability. The X and Y axes control the main worktable movement, while the U and V axes control the relative position of the upper wire guide. By coordinating these axes, the CNC system can produce taper angles and profiles that vary along the cutting path.
This capability is particularly valuable in mold manufacturing. A die component may require a straight lower profile and a differently positioned upper profile, or it may need a controlled taper to assist part release. Without coordinated upper-guide movement, these geometries would require additional operations, special fixtures, or manual intervention. Four-axis wire cutting reduces setup complexity and improves the consistency of the resulting geometry.
The specified maximum taper is ±6° per 80 mm. This figure provides a useful reference for applications involving tapered punches, die inserts, slanted walls, and other inclined features. The achievable result in a particular workpiece depends on thickness, wire condition, material, flushing, guide alignment, programming accuracy, and the selected cutting strategy. For critical components, a trial cut and measurement process should be included during process planning.
Four-axis control also supports the machining of irregular profiles and complex contours. The wire electrode does not require a conventional cutting edge, so it can enter predrilled start holes and follow programmed paths through hardened conductive materials. Narrow slots, intricate outlines, internal corners, and delicate profiles can be produced without imposing the same mechanical cutting forces associated with milling or broaching.
For production departments, four-axis capability can improve process flexibility. The same machine can be used for simple vertical profiles, high-accuracy mold features, tapered components, and specialized shapes. This versatility helps reduce the number of dedicated machines required for a varied job mix.
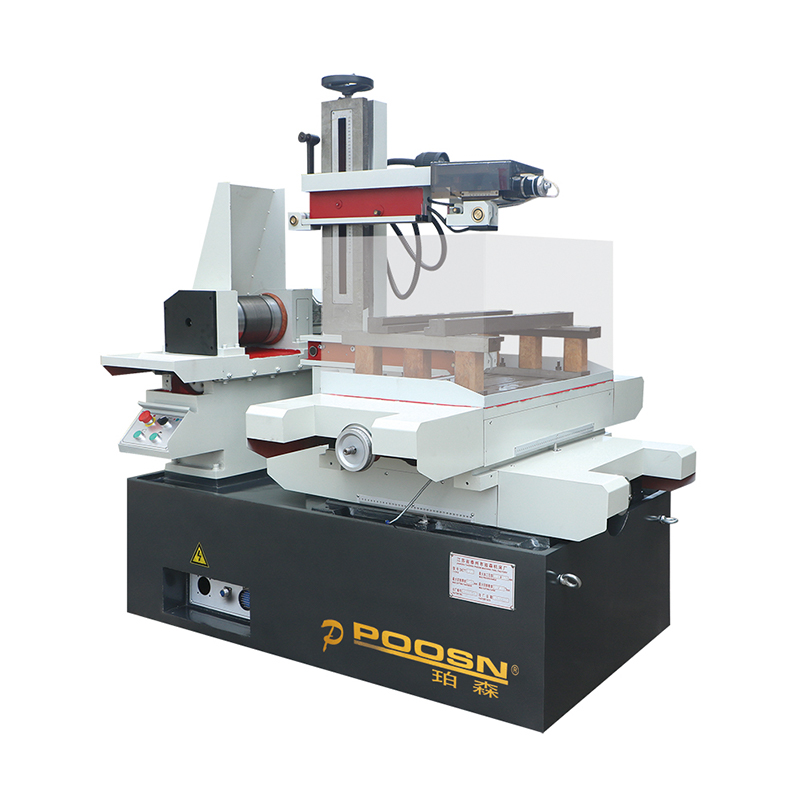
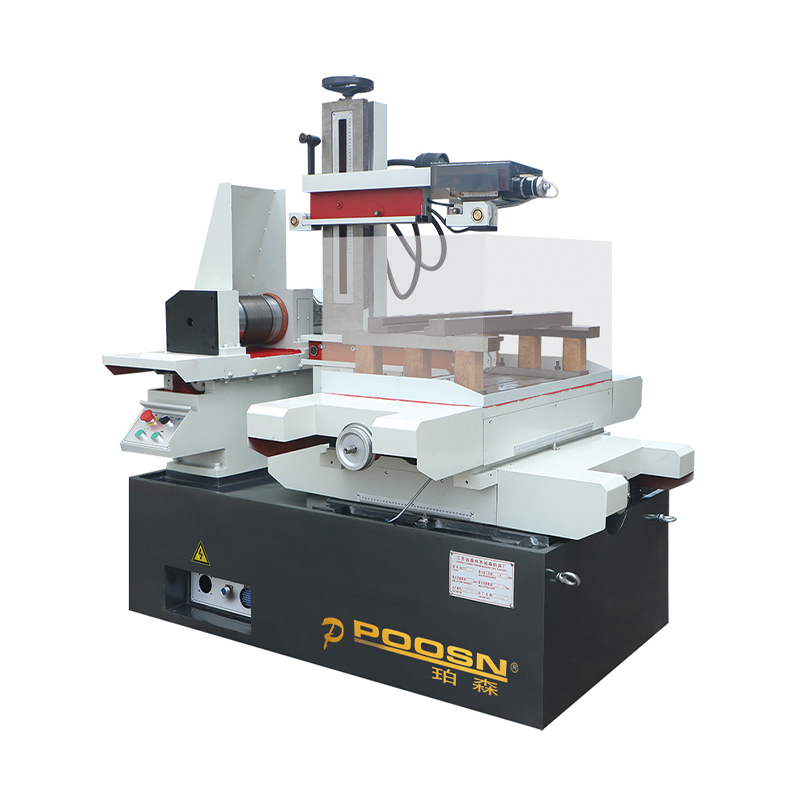
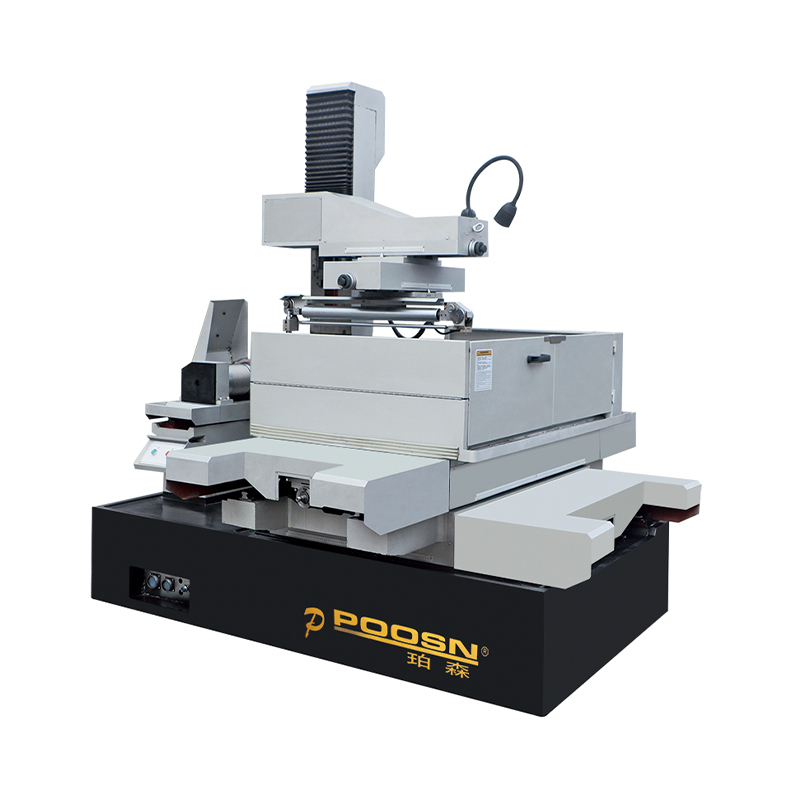
DK-7745 CNC High-Speed Wire EDM Machine (4-Axis, 400×600mm Travel)
4. High-Speed Reciprocating Wire System
The DK-7745 uses a high-speed reciprocating wire system, a characteristic feature of high-speed wire-cut EDM equipment. In this arrangement, the wire electrode travels back and forth through the machining zone rather than being consumed in a single continuous pass. The wire is supported and guided through a controlled path so that electrical discharges can remove material along the programmed contour.
Reciprocating wire technology offers an important operating-cost benefit. Because the wire can be reused for multiple passes, electrode consumption may be lower than in many low-speed wire EDM processes that use a continuously supplied single-use wire. The exact saving depends on cutting conditions, wire diameter, workpiece material, cutting thickness, flushing quality, and the number of passes. Nevertheless, the reusable-wire principle makes high-speed WEDM attractive for mold shops and component manufacturers that must control consumable expenses.
The wire feeding system is designed around a dynamically balanced wire drum and precision guide components. Dynamic balance is significant because vibration in the wire path can affect machining stability, surface quality, and dimensional consistency. A smoother wire movement helps maintain a more controlled discharge gap and reduces unwanted fluctuations during high-speed operation.
High-speed reciprocation also supports efficient material removal. The published maximum cutting efficiency is up to 16,000 mm²/h under suitable conditions, while typical performance with specified CNC cabinets is described within a range of approximately 10,000 to 16,000 mm²/h. This should be understood as a process-dependent value rather than a universal production guarantee. Material grade, thickness, workpiece shape, flushing, wire tension, pulse parameters, and required surface finish all influence the actual rate.
Compared with equipment designed primarily for slow finishing cuts, the DK-7745 is positioned toward a stronger combination of roughing productivity and practical finishing performance. It can remove material efficiently while using repeated cutting strategies to improve the final profile and surface condition. This makes the machine appropriate for both individual precision components and repeated mold production.
5. Structural Rigidity and Long-Term Stability
Precision wire EDM depends on more than the CNC controller. The machine bed, worktable, guide rails, wire guides, ball screws, electrical cabinet, and dielectric circulation system must function as an integrated system. If the structure deflects under load or thermal and mechanical vibration are not controlled, even an advanced control program cannot fully compensate for the resulting errors.
The DK-7745 uses a heavy-duty structure based on high-strength cast material. The supplied technical description emphasizes stress relief and aging treatment of the castings. These processes are intended to reduce internal stress and limit dimensional changes after machining. A stable bed provides a more reliable foundation for guide rail alignment and helps the machine maintain geometric accuracy during long production cycles.
Structural mass also contributes to vibration damping. During high-speed reciprocating wire movement, the machine is exposed to repeated dynamic forces. A rigid and vibration-resistant frame helps prevent these forces from being transferred excessively to the workpiece. This is especially important when machining thin ribs, narrow slots, fine corners, and high-value mold components where a small vibration pattern can affect the surface or edge condition.
The DK-7745 incorporates precision guide components and ball-screw transmission in its stated process architecture. Precision ball screws support controlled axis movement, while high-rigidity linear guides help maintain smooth travel over the available machining range. The combination is intended to provide repeatable positioning and stable motion during both long straight cuts and complicated interpolated contours.
The machine is specified according to GB/T 7926-2015 for machine accuracy. In addition, the manufacturer states that completed machines undergo positioning accuracy inspection before shipment. These practices demonstrate an emphasis on measurable geometric performance rather than relying only on component selection. Customers should request the applicable inspection record and acceptance criteria when defining a purchase specification.
6. Electrical Discharge and Pulse Power Performance
Wire EDM removes material through controlled electrical discharges between the wire electrode and the conductive workpiece. The workpiece is not cut by direct mechanical contact. Instead, a series of electrical pulses creates localized thermal energy that melts and vaporizes minute amounts of material. A dielectric fluid then helps cool the machining zone and carry away eroded particles.
The stability of the pulse power supply has a direct influence on cutting efficiency, wire breakage, dimensional accuracy, and surface finish. The DK-7745 is described as having a responsive internal power control module and an intelligent variable-frequency high-frequency generator. These systems are intended to adjust discharge conditions according to the changing machining gap and workpiece condition.
Stable pulse output is particularly important when cutting thick sections. A thick workpiece creates greater demands for flushing and debris removal, and unstable discharge conditions can increase the risk of short circuits or wire breakage. By maintaining a controlled pulse energy output and adapting the frequency characteristics, the system can help sustain the electrical discharge process over a longer cutting path.
The machine’s dielectric circulation and flushing system also contribute to process stability. Effective flushing removes eroded particles from the kerf, reduces the chance of secondary discharges, and helps control heat accumulation. When flushing is properly matched to workpiece thickness and cutting conditions, it can support higher productivity and a more consistent surface finish.
In practical production, operators should treat electrical settings, wire tension, flushing pressure, and cutting speed as a coordinated group. Increasing speed without providing adequate flushing may reduce stability. Excessive pulse energy may improve roughing performance but increase surface damage or wire stress. The DK-7745’s control architecture provides a platform for optimizing these variables according to the required result.
7. Accuracy, Surface Finish, and Process Control
The supplied product information states that the DK-7745 can achieve linear accuracy of up to 0.005 mm and taper accuracy of 0.015 mm under suitable conditions. These values indicate the machine’s intended precision class, although actual performance depends on calibration, thermal conditions, wire alignment, material, programming, workholding, and the operator’s process settings.
An optimal surface roughness of Ra ≤ 2.5 μm is listed for the range. This level is suitable for many mold and mechanical component applications, particularly where a controlled EDM surface is acceptable or where polishing and secondary finishing will follow. The final surface quality is influenced by the number of passes, pulse parameters, wire condition, flushing, material composition, and the required dimensional tolerance.
For critical production, a multi-pass strategy is often more appropriate than attempting to reach final size in a single cut. A rough cut can focus on efficient material removal, while skim or finishing cuts can refine the profile and improve the surface. The rigid structure and four-axis control of the DK-7745 allow the process engineer to create cutting programs appropriate to both stages.
Dimensional accuracy also depends on correct workpiece preparation. The workpiece must be conductive, securely supported, and accurately positioned. Start holes should be located according to the drawing and cut path. Workholding must prevent movement without obstructing wire travel or dielectric circulation. In thick workpieces, the operator should verify that the wire guides, flushing conditions, and machining height are suitable for the job.
When these conditions are controlled, the machine can deliver repeatable results across batches. Repeatability is particularly valuable in mold inserts and precision mechanical components, where multiple parts must match one another or fit with previously manufactured assemblies.
8. Workpiece Capacity and Heavy-Duty Machining
The DK-7745 has been designed for large and heavy workpieces. Its listed worktable size is 570 × 850 mm, and the maximum worktable load is 400 kg. This capacity allows manufacturers to process workpieces that would be difficult to accommodate on compact machines.
Large workpiece capacity creates several productivity benefits. First, it allows more components to be arranged in a single setup. Second, it reduces the need to divide large molds or plates into separate operations. Third, it can make nesting more efficient when several small or medium components must be cut from one plate. Fewer setups can reduce alignment errors, fixture costs, handling time, and operator intervention.
Large-format machining must always be carried out within the machine’s rated limits. The total workpiece mass, fixture mass, position of the center of gravity, and load distribution should be evaluated before machining. A workpiece near the rated capacity may require additional support or a carefully planned loading procedure. The 400 kg figure should not be interpreted as permission to place any shape of load anywhere on the table without checking the manufacturer’s operating requirements.
The machine’s maximum cutting thickness of 450 mm further supports applications involving thick mold plates and large die sections. Thick cutting requires attention to flushing, wire stability, taper compensation, and heat removal. The DK-7745’s high-speed wire system and dielectric circulation design are intended to address these requirements while maintaining a practical balance between cutting speed and accuracy.
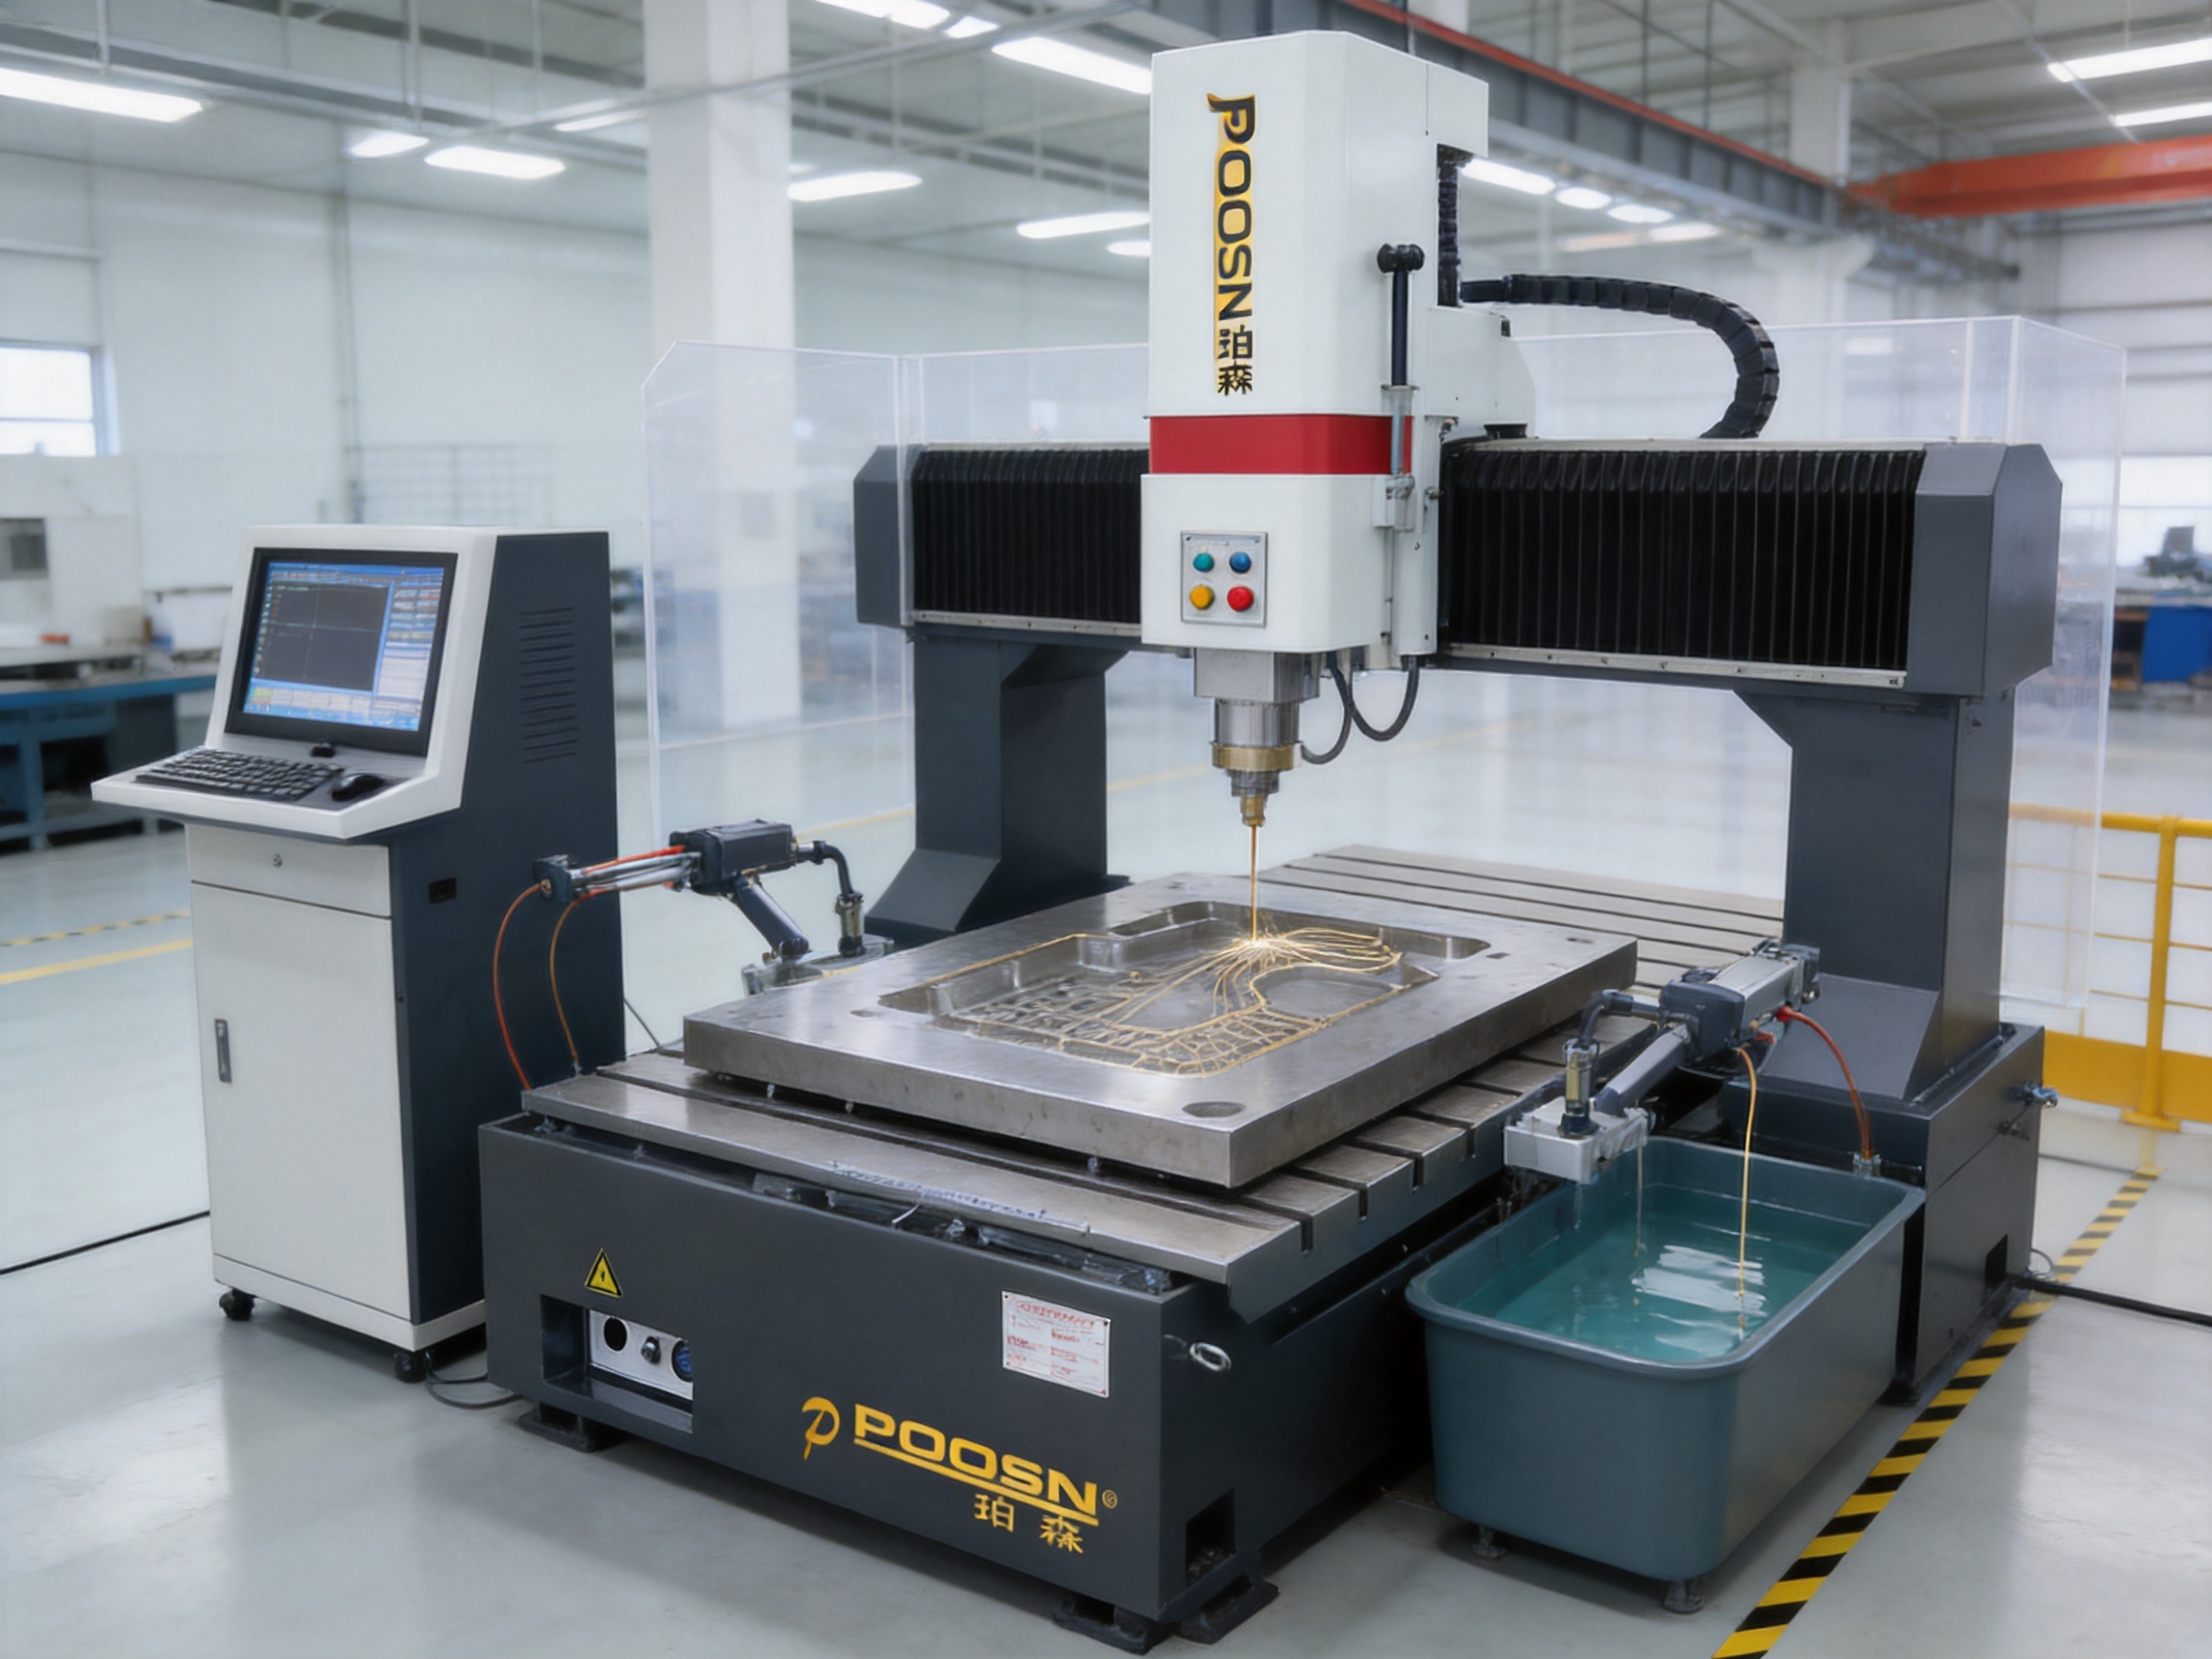
9. Competitive Advantages in the High-Speed WEDM Market
The DK-7745 competes in a market that includes compact high-speed wire EDM machines, medium-size wire-cut systems, large-format machines, and low-speed wire EDM equipment. Its advantages are best understood as a combination of capabilities rather than a single specification.
9.1 Larger Capacity Than Compact Machines
Many compact wire-cut machines are suitable for small parts, sample production, and limited-size molds, but they may require multiple setups when the workpiece becomes large or heavy. With its substantial worktable, 400 kg load capacity, and extended cutting thickness, the DK-7745 provides more room for large components and production nesting.
This capacity can be especially valuable to job shops. A job shop must often switch between different workpiece sizes and materials. A machine with a broader operating range reduces the risk that a new order will exceed the capacity of the available equipment.
9.2 Lower Consumable Pressure Than Single-Use Wire Processes
Compared with low-speed wire EDM systems that normally use continuously supplied wire, high-speed reciprocating technology can reduce electrode-wire consumption because the wire is reused. This difference may lower the cost per job, particularly in applications involving long cutting paths or repeated production. The saving must be evaluated together with electricity, filters, dielectric maintenance, wire quality, and labor, but the reusable-wire architecture remains a significant competitive advantage.
9.3 Four-Axis Taper Capability
Basic two-axis wire-cutting equipment is primarily suited to vertical profiles. The DK-7745’s X, Y, U, and V linkage allows it to produce taper and more complicated upper-to-lower profile relationships. This increases the range of components that can be completed without transferring the workpiece to another machine.
9.4 Balance Between Speed and Precision
The DK-7745 is not positioned solely as a high-speed roughing machine. Its pulse control, guide system, rigid structure, and multi-pass capability are intended to provide efficient cutting while preserving the accuracy needed for molds and precision parts. The published cutting efficiency of up to 16,000 mm²/h gives production departments a useful productivity target, while the specified accuracy and surface finish values support precision-oriented work.
9.5 Heavy-Duty Construction
A reinforced frame and stress-relieved casting provide a more stable foundation than a lightweight structure designed only for intermittent work. Heavy-duty construction can be advantageous in long-duration operation, when machining thick workpieces, or when the machine must maintain alignment under a high table load.
9.6 Flexible Control Cabinet Selection
The standard ZH-K68 desktop cabinet is designed for a conventional operator station, while the optional ZHZK-03 vertical cabinet provides an alternative layout. Cabinet selection allows users to adapt the machine to their workshop arrangement, operator preference, and available floor space. Buyers should confirm which cabinet is included in the quotation and whether any software, communication, or monitoring functions require additional configuration.
10. CNC Control and Operator Usability
High-speed WEDM productivity depends on the machine’s control system as much as on its mechanical hardware. The DK-7745 is described as using an intuitive CNC interface that supports the transition from design data to machining programs. A user-oriented control system can reduce programming time, simplify job setup, and help operators monitor the machining process.
For new operators, clear menus and logical parameter organization shorten the learning curve. The supplied information also describes features such as graphic verification and power-loss memory. Graphic verification helps identify incorrect contours, unwanted intersections, and programming errors before the workpiece is cut. Power-loss memory can reduce the risk of losing an unfinished operation after an interruption, although recovery procedures should always follow the machine’s safety instructions.
The control system supports complex contour interpolation and four-axis coordination. This means the machine can translate programmed geometry into synchronized axis movement rather than relying on manual adjustment of the upper guide. For mold shops that process different geometries every day, this flexibility can improve responsiveness and reduce dependence on highly specialized manual skills.
Ease of operation does not eliminate the need for training. Operators should understand electrical discharge principles, conductive material requirements, wire threading, dielectric maintenance, workpiece alignment, cutting parameter selection, and emergency procedures. The manufacturer’s technical support and process guidance can help customers build a safe and repeatable operating method.
11. Manufacturing Processes and Quality Assurance
The performance of a wire EDM machine depends strongly on how it is manufactured and assembled. Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. states that it has specialized in electrical discharge wire cutting since 1999 and has developed experience in research, development, production, inspection, and technical service.
The company’s manufacturing approach includes strong technical capabilities, advanced processing equipment, and comprehensive testing methods. Its products are described as being manufactured according to national standards, with each machine tool undergoing positioning accuracy testing. This approach is important because wire EDM performance cannot be judged only by the appearance of the finished machine. Guide alignment, axis positioning, electrical stability, wire path geometry, and dielectric circulation must all be checked as part of final assembly.
11.1 Casting and Stress Relief
The DK-7745’s heavy-duty structure begins with a rigid cast foundation. Aging or stress-relief treatment is used to reduce the possibility of internal casting stress affecting geometric stability after machining. The value of this process becomes more apparent over time, as a stable casting is less likely to experience unwanted dimensional change under normal operating conditions.
After casting treatment, critical mounting surfaces can be machined to support guide rails, ball screws, worktable assemblies, and wire system components. The precision of these interfaces determines how accurately the complete machine can be aligned.
11.2 Precision Assembly
Assembly quality is essential for maintaining the relationship between the X, Y, U, and V axes. The table, guide rails, screws, wire guides, and upper and lower arms must be installed and adjusted so that the wire remains correctly positioned relative to the workpiece. Proper assembly reduces mechanical error and supports repeatable taper cutting.
The wire drum and feeding path require particular care. Dynamic balance, guide alignment, and tension control affect vibration and discharge stability. A carefully assembled wire path helps reduce irregular marks, unstable cutting, and premature wire failure.
11.3 Electrical and Control Integration
The power supply, control cabinet, servo or stepper drives, sensors, limit protection, pump system, and user interface must be integrated as one operating system. The manufacturer’s stated high-redundancy electrical design is intended to help the machine remain stable when pulse power demand changes during heavy cutting.
Electrical integration also involves safety. Emergency stops, door or access protections where applicable, insulation, grounding, fluid management, and overload protection must be verified before delivery. Reliable integration helps protect the operator, the workpiece, the wire system, and the machine itself.
11.4 Final Inspection
Before shipment, each machine should be checked for positioning accuracy, axis travel, wire movement, electrical discharge operation, flushing, control response, and overall machine function. The company states that it conducts positioning accuracy tests and maintains comprehensive inspection capabilities. Customers purchasing for high-precision work should request factory acceptance information, accuracy reports, test-cut records, and installation requirements as part of the technical agreement.
12. Application Areas
12.1 Precision Mold Manufacturing
The DK-7745 is well suited to stamping dies, plastic injection molds, progressive dies, precision inserts, punches, and cavity components. Wire EDM can create narrow slots, complex profiles, sharp internal corners, and hardened features that may be difficult to produce by milling alone.
Four-axis taper cutting is useful for die components that require controlled release angles or changing upper and lower profiles. The large worktable and high load capacity are advantageous when the mold base or die plate cannot be conveniently divided into smaller sections.
12.2 Precision Mechanical Components
Mechanical manufacturers can use the machine for gears, punches, shims, precision plates, special shafts, tooling elements, and custom components made from hardened conductive materials. Because the cutting force is very low compared with mechanical cutting, delicate profiles can often be produced with reduced risk of mechanical deformation.
12.3 Aerospace Components
Aerospace manufacturing often involves high-strength alloys, complex profiles, tight dimensional requirements, and strict process documentation. The DK-7745 can support the production of selected conductive aerospace components, tooling, fixtures, and mold elements. Aerospace users should establish material-specific cutting procedures, inspection plans, and traceability requirements before production.
12.4 Automotive Components and Tooling
Automotive die production requires both productivity and repeatability. The DK-7745 can be used for stamping die components, precision inserts, cutting tools, and complex conductive parts. Its combination of large workpiece handling and high-speed cutting can help shorten production cycles while supporting consistent results over repeated jobs.
12.5 Electrical and Electronic Equipment
Electrical and electronic components may require small slots, fine openings, precise plates, connector tooling, and specialized conductive parts. The machine’s controlled wire path and low mechanical cutting force make it appropriate for delicate contours, provided that the workpiece is correctly fixtured and the process parameters are selected for the material and required finish.
12.6 Hard Materials
Wire EDM is particularly useful for conductive hardened steel, carbide, tool steel, and other materials that are difficult to machine by conventional methods. Since the process relies on electrical discharge rather than cutting-edge hardness alone, the machine can process materials after heat treatment. The workpiece must be electrically conductive, and the cutting strategy must reflect its composition and thickness.
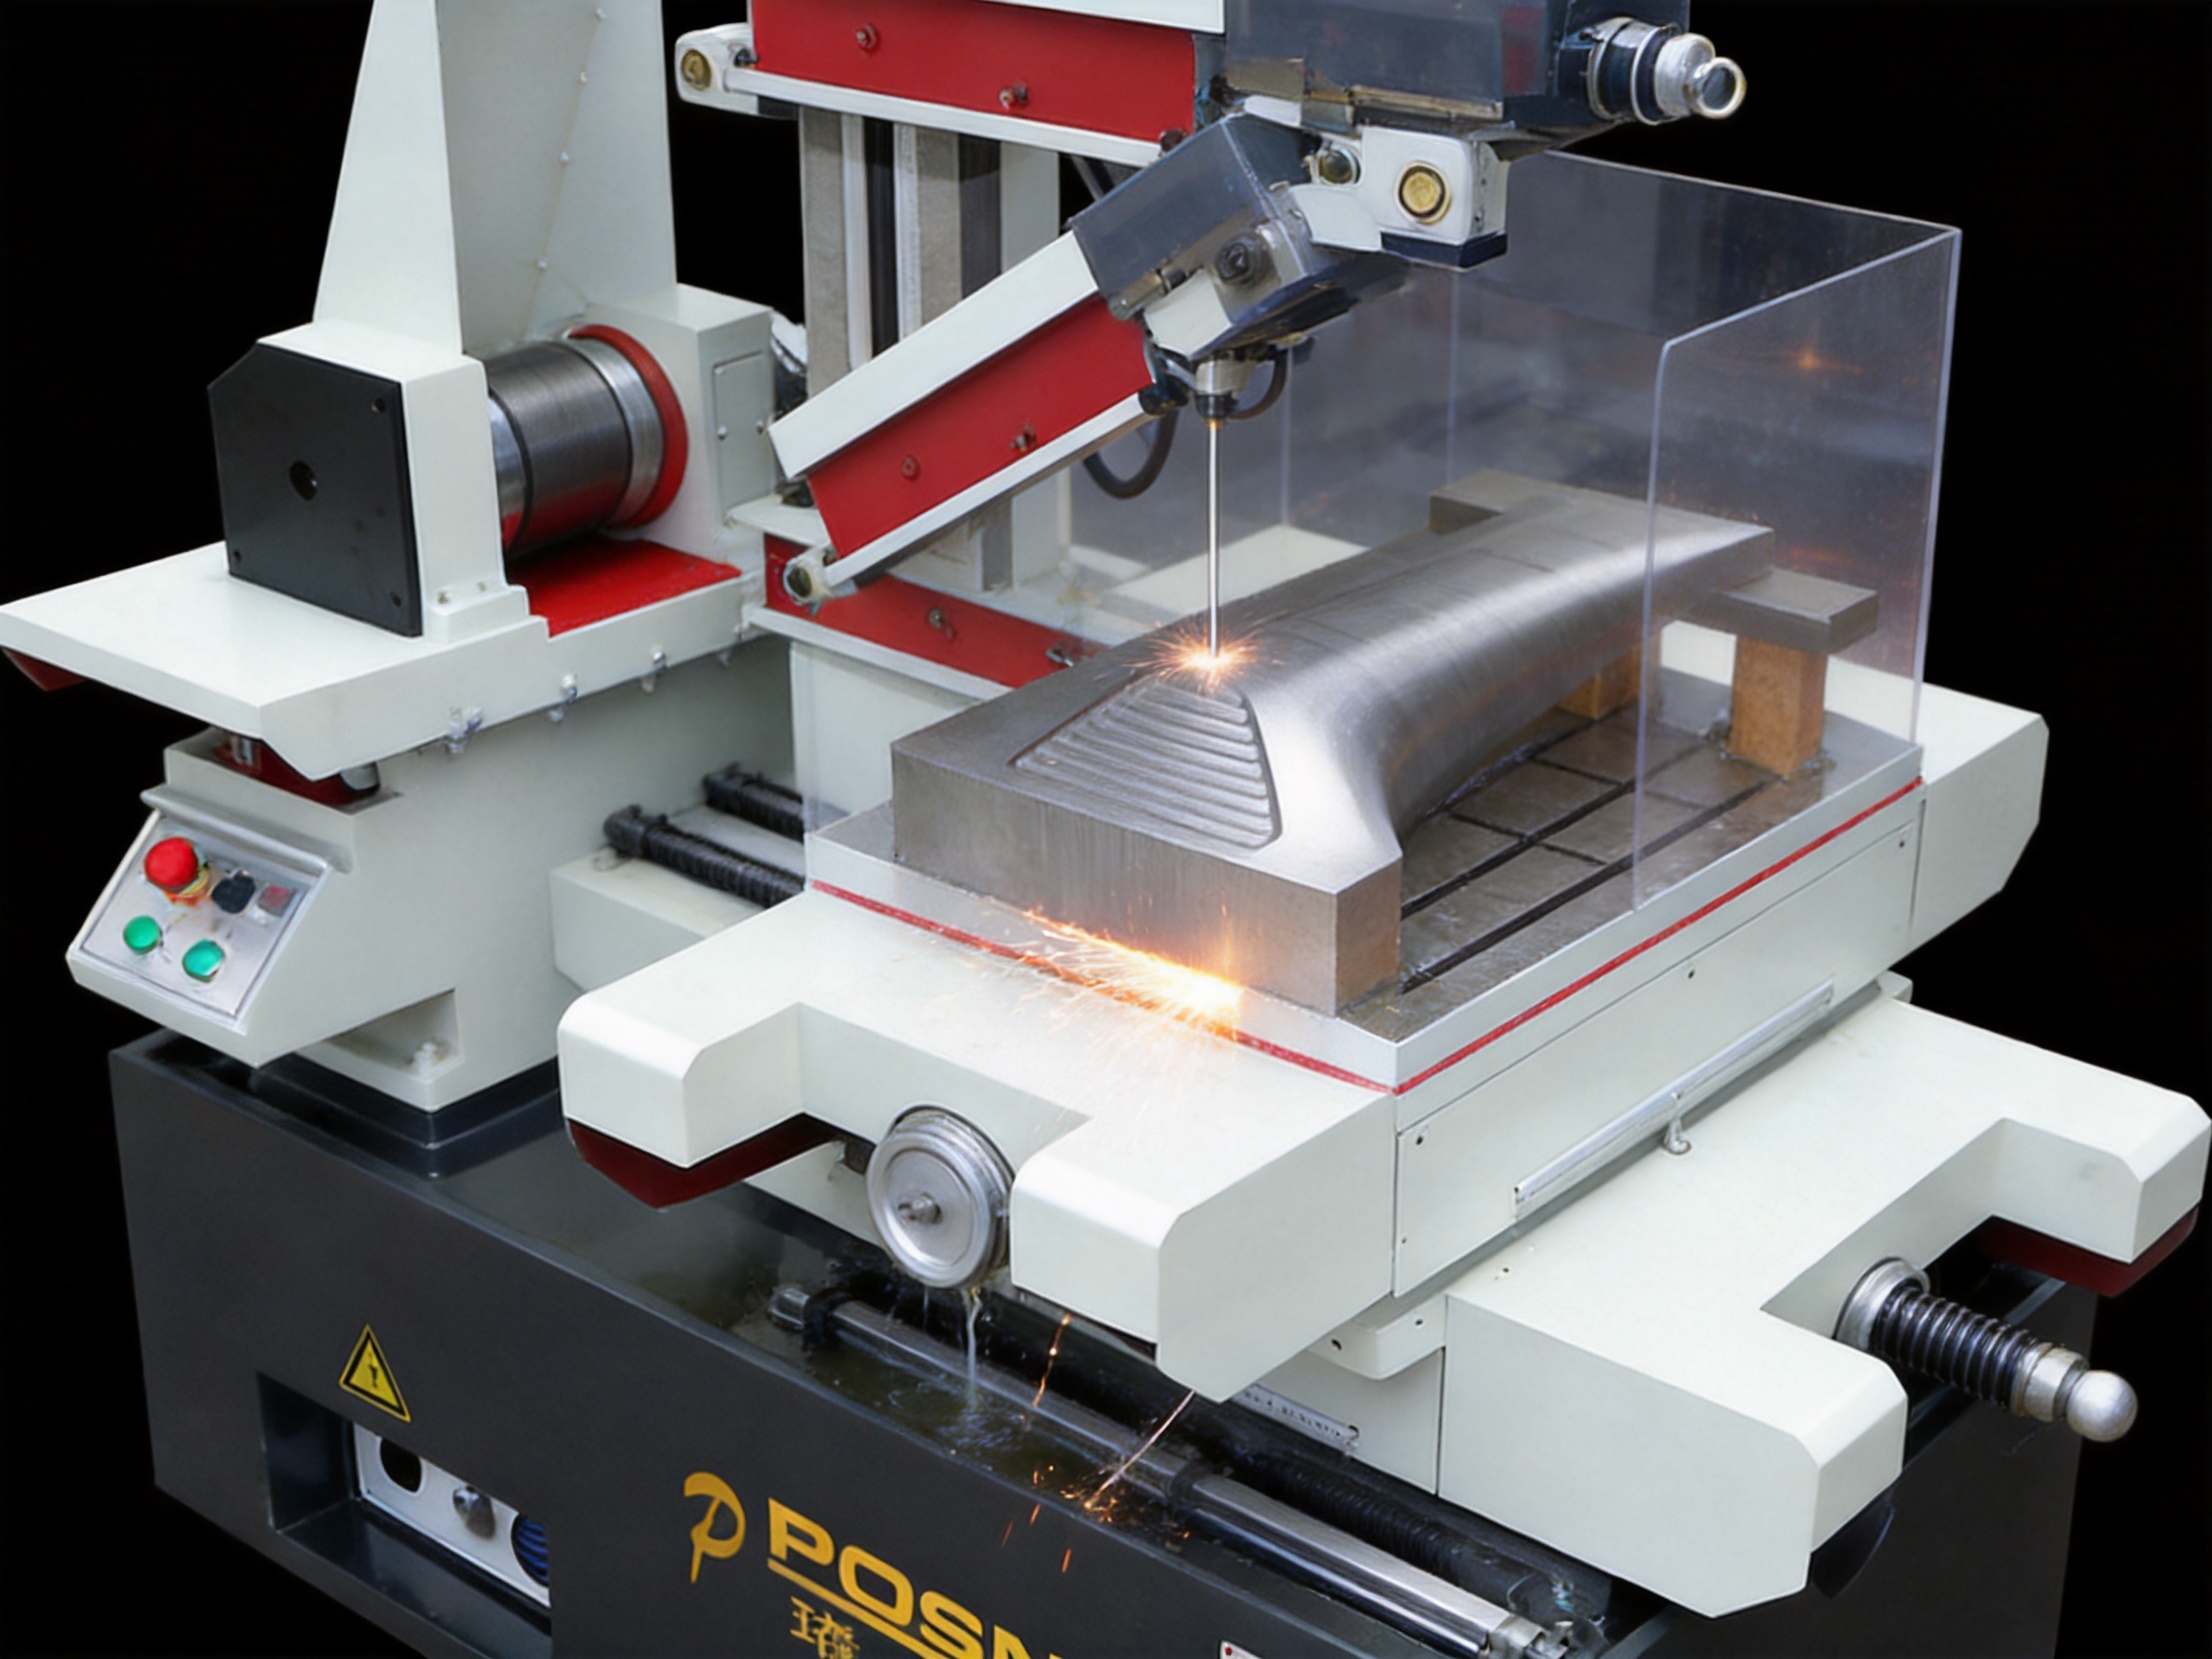
13. Production Efficiency and Total Cost Considerations
Purchasing a wire EDM machine should involve more than comparing the initial equipment price. Manufacturers should evaluate total operating cost, including wire, filters, dielectric maintenance, power consumption, labor, downtime, tooling, installation, and after-sales support. The DK-7745 is designed to improve the overall value equation through efficient cutting, reusable wire operation, large-workpiece capacity, and reduced setup requirements.
High cutting efficiency can shorten production cycles. A shorter cycle may allow a workshop to accept more orders without immediately adding another machine. It may also reduce work-in-process inventory and improve delivery reliability. However, the fastest roughing rate is not always the most economical result. A balanced process that achieves the required dimensional accuracy and surface finish with an appropriate number of passes often provides the best total cost.
The machine’s large working envelope can also improve productivity per setup. Multiple smaller parts may be arranged on one plate, or a large mold component may be completed without repositioning. Fewer setups reduce alignment labor and lower the risk of cumulative positioning errors.
High-speed reciprocating wire technology may reduce the cost of electrode consumption compared with continuously supplied wire systems. This advantage is most meaningful when the machine is used regularly and the wire path, filtration, and electrical settings are properly maintained. Operators should record wire consumption, cutting time, filter replacement, and rework to evaluate actual production economics.
Reliability is another part of return on investment. A rigid frame, stable guide system, robust electrical design, and factory inspection can help reduce unplanned downtime. The manufacturer’s technical support further contributes to equipment availability by assisting with process adjustment, maintenance, consumable selection, and troubleshooting.
14. Customization and Technical Support
Different factories have different workpiece sizes, control preferences, production volumes, power conditions, and automation requirements. The DK-7745 series supports customization services intended to adapt the machining solution to specific technical and production needs.
Customization may involve selecting the control cabinet, confirming worktable and travel requirements, preparing special fixtures, configuring process accessories, or discussing the needs of unusually large or heavy workpieces. For projects involving special cutting conditions, customers should provide drawings, material information, thickness, taper requirements, tolerance targets, surface finish expectations, and estimated production volume.
Technical support should begin before installation. A complete project plan should cover foundation requirements, machine transportation, electrical supply, dielectric system preparation, environmental conditions, lifting arrangements, operator training, and acceptance testing. Early planning helps prevent delays and ensures that the machine can begin production efficiently after installation.
After-sales support may include troubleshooting, process optimization, cutting strategy recommendations, consumable selection, maintenance guidance, and training. The manufacturer states that it provides rapid response and professional technical assistance to help ensure equipment stability and long-term effectiveness.
15. Installation, Operation, and Maintenance Recommendations
The DK-7745 should be installed on a suitable foundation in a clean and stable workshop environment. The floor must support the machine weight and the dynamic loads associated with operation. Adequate space should be reserved around the machine for loading, maintenance, wire handling, electrical access, and safe operator movement.
Before initial operation, the power supply should be checked against the specified three-phase 380 V ±10% requirement. Grounding, electrical protection, dielectric fluid, pumps, filters, wire guides, and emergency functions should be inspected. The machine should be leveled and aligned according to the installation manual.
Daily operation should include checks of wire condition, wire tension, dielectric fluid level, flushing, filters, guide components, workpiece clamping, and abnormal sounds or vibration. The operator should confirm that the programmed path is correct and that the wire can move freely through the intended contour.
Dielectric fluid quality is important for both cutting stability and machine life. Contaminated fluid can increase short circuits, reduce cutting efficiency, affect surface quality, and place additional stress on the pump and filtration system. Scheduled cleaning and filter replacement should be based on usage, material, cutting volume, and the manufacturer’s maintenance recommendations.
Wire guides and contact components are wear parts. Their condition influences wire position and machining accuracy. If guide wear becomes excessive, the machine may show taper errors, dimensional deviations, irregular surface marks, or unstable cutting. Preventive replacement is generally more economical than waiting for a high-value workpiece to fail.
At the end of a production shift, the work area should be cleaned, the dielectric system should be checked, and the machine should be left in the recommended standby condition. Maintenance records should document operating hours, fluid changes, filter replacement, guide replacement, accuracy checks, and corrective actions.
16. Model Selection Within the DK-77 Range
The DK-7745 is one model in a broader family. Selecting the correct model depends on workpiece dimensions, required cutting thickness, worktable load, floor space, production volume, and future expansion plans.
The DK-7725 is aimed at small and medium-sized parts, precision mold work, and small-batch production. It is appropriate when the workpiece is relatively compact and the customer prioritizes a smaller machine footprint.
The DK-7735 provides a larger worktable and travel range for medium-sized components and molds. It may be a suitable step for workshops that have outgrown a compact machine but do not regularly process large heavy workpieces.
The DK-7745 is intended for large-sized parts, high-precision molds, aerospace components, automotive tooling, and applications requiring a stronger worktable load capacity. Its 400 kg rated load and larger working envelope make it a practical choice for demanding general-purpose production.
The DK-7745F is designed for extra-large workpieces and heavier precision components. For aerospace tooling, large-scale molds, and applications where the additional table size and load capacity are essential, this model can provide a more suitable operating range.
The extended models DK-7755F, DK-7763F, DK-7780F, and DK-77100F are intended for progressively larger workpieces. Their table loads range from 600 kg to 1,200 kg, and customizable options are available for DK-77100 and larger machines. Customers should select the smallest model that comfortably accommodates present and anticipated work, because excessive capacity may increase installation, energy, and floor-space requirements.
17. Recommended Purchasing and Acceptance Checklist
Before ordering a DK-7745, the buyer should confirm the exact configuration in writing. This includes the X/Y travel, worktable dimensions, maximum cutting thickness, taper capability, table load, machine dimensions, machine weight, control cabinet, power requirements, software functions, and included accessories.
Customers should also clarify whether the quoted cutting efficiency refers to a specific material and thickness. A sample cutting test can provide more useful information than a general maximum rating. The test should evaluate cutting time, dimensional accuracy, taper accuracy, surface roughness, wire consumption, and the number of required passes.
For large workpieces, the acceptance procedure should verify table loading, workpiece support, wire threading, flushing, axis movement, and accessibility. For high-precision components, acceptance should include measurement of straightness, squareness, positioning, repeatability, taper, and surface finish under agreed conditions.
Documentation should include the operating manual, electrical diagrams where applicable, maintenance schedule, recommended consumables, installation instructions, safety information, inspection certificate, and warranty terms. Clear documentation helps the customer establish a controlled production process and reduces dependence on informal operating practices.
18. Frequently Asked Questions
Q1: What is the maximum worktable load of the DK-7745?
The listed maximum worktable load for the DK-7745 is 400 kg. The actual loading procedure must also consider the fixture weight, load distribution, workpiece center of gravity, and the manufacturer’s safety requirements.
Q2: What are the main accuracy specifications?
The supplied information states linear accuracy of up to 0.005 mm and taper accuracy of 0.015 mm under suitable conditions. The model range is manufactured according to GB/T 7926-2015. Actual results depend on calibration, temperature, material, workholding, wire alignment, programming, and cutting parameters.
Q3: What is the maximum cutting thickness?
The DK-7745 is listed with a maximum cutting thickness of 450 mm. Thick-section performance depends on material, flushing, wire condition, pulse settings, workpiece geometry, and the required accuracy and surface finish.
Q4: What is the maximum cutting efficiency?
The published maximum cutting efficiency is up to 16,000 mm²/h, with a typical stated range of 10,000 to 16,000 mm²/h. This is a reference value rather than a guarantee for every workpiece. Production performance should be confirmed through a sample test using the customer’s material and thickness.
Q5: Can the DK-7745 cut tapered profiles?
Yes. The machine uses X, Y, U, and V axes with four-axis linkage and is listed with a maximum cutting taper of ±6° per 80 mm. The final achievable taper depends on workpiece thickness, wire alignment, programming, material, and process settings.
Q6: Which materials can be processed?
The machine can process electrically conductive materials such as hardened steel, tool steel, carbide, and other conductive alloys. Nonconductive materials generally cannot be processed by conventional wire EDM unless they have been specially prepared or coated according to an appropriate process.
Q7: Is high-speed wire EDM less expensive to operate than low-speed wire EDM?
High-speed reciprocating wire EDM can reduce electrode-wire consumption because the wire is reused. It may therefore offer a lower consumable cost in many applications. Total operating cost still depends on electricity, filters, dielectric maintenance, labor, cutting time, wire quality, and the required number of passes.
Q8: Is the DK-7745 suitable for mass production?
Yes. Its high cutting efficiency, large worktable, 400 kg load capacity, four-axis control, and stable structure make it suitable for repeated production. The best results are obtained when workholding, programming, maintenance, and cutting parameters are standardized.
Q9: Is the CNC system difficult for new operators?
The machine is designed with a user-oriented CNC interface and supports graphic verification and power-loss memory functions according to the supplied information. New operators still require training in wire EDM principles, safety, workpiece preparation, programming, parameter selection, and maintenance.
Q10: What control cabinets are available?
The standard cabinet is the ZH-K68 desktop cabinet. The ZHZK-03 vertical cabinet is listed as an optional configuration. The final cabinet should be confirmed in the commercial quotation because cabinet selection may affect workshop layout and operating preferences.
Q11: How does the machine maintain long-term stability?
The stated design includes a rigid cast structure, aging or stress-relief treatment, precision guide rails, ball-screw transmission, a balanced wire feeding system, and final positioning accuracy inspection. Correct installation, dielectric maintenance, guide replacement, and periodic accuracy verification are also necessary for long-term performance.
Q12: Does the manufacturer provide customization?
Yes. Customization services are available for different machining requirements. Customers can discuss workpiece size, special taper requirements, control cabinet selection, accessories, process conditions, and other technical details with the manufacturer before ordering.
19. Conclusion
The DK-7745 CNC High-Speed Wire EDM Machine is designed for manufacturers that need a strong combination of size, precision, flexibility, and production efficiency. Its four-axis linkage supports taper cutting and complex contours, while the high-speed reciprocating wire system helps control electrode consumption and maintain practical cutting productivity.
The machine’s large worktable, 400 kg loading capacity, 450 mm stated cutting thickness, high-strength structure, precision guide system, controlled pulse power, and dielectric circulation make it suitable for molds, hardened mechanical components, aerospace tooling, automotive parts, and precision electronic equipment. Its listed cutting efficiency of up to 16,000 mm²/h provides a strong productivity foundation, while the specified accuracy and surface-finish capabilities support demanding applications.
Its competitive value comes from the integration of these features. Compared with compact machines, it accommodates larger and heavier workpieces. Compared with basic two-axis systems, it provides four-axis taper capability. Compared with many continuously wired low-speed systems, its reciprocating wire design can reduce wire consumption. Compared with lightweight structures, its heavy-duty frame is intended to provide greater stability during long and high-load operations.
Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. supports this product with experience in electrical discharge wire cutting, in-house manufacturing capabilities, inspection procedures, product development, customization, and technical service. Its broader product range allows customers to select equipment according to workpiece size and production requirements rather than forcing every application into one machine format.
For the best purchasing decision, buyers should confirm the final DK-7745 configuration, conduct a representative sample test, define acceptance criteria, and plan installation and operator training in advance. When correctly specified and maintained, the DK-7745 can serve as a reliable production platform for precision wire-cut EDM work and a practical foundation for improving machining efficiency, reducing setup time, and controlling manufacturing costs.
References
1. Taizhou Xinchengyang Machinery Manufacturing Co., Ltd., DK-7745 CNC High-Speed Wire EDM Machine Product Information and Technical Specifications.
2. Taizhou Xinchengyang Machinery Manufacturing Co., Ltd., DK-77 Series High-Speed Wire-Cut EDM Machine Model Comparison Data.
3. GB/T 7926-2015, Accuracy of Metal-Cutting Wire-Cut Electrical Discharge Machines.
4. General Principles of Electrical Discharge Machining, Technical Training Material for Wire-Cut EDM Operations.
5. Manufacturing Process Guidance for High-Speed Reciprocating Wire EDM Systems, Technical Reference Edition.
6. Industrial CNC Machine Tool Installation, Alignment, Maintenance, and Acceptance Practices.
Product: DK-7745 CNC High-Speed Wire EDM Machine (4-Axis, 400×600mm Travel)
-
Phone
+86-0523-86268788 +86-13815960366 +86-13912191163Email
[email protected]Address
No. 366, Yusheng Road Jiulong Town, Hailing District Taizhou City, China
Copyright © Taizhou Xinchengyang Machinery Manufacturing Co., Ltd. All Rights Reserved.
Custom edm machine for sale
wholesale edm machine manufacturers
